
Custom Casting Blanks for Your In-House Machining
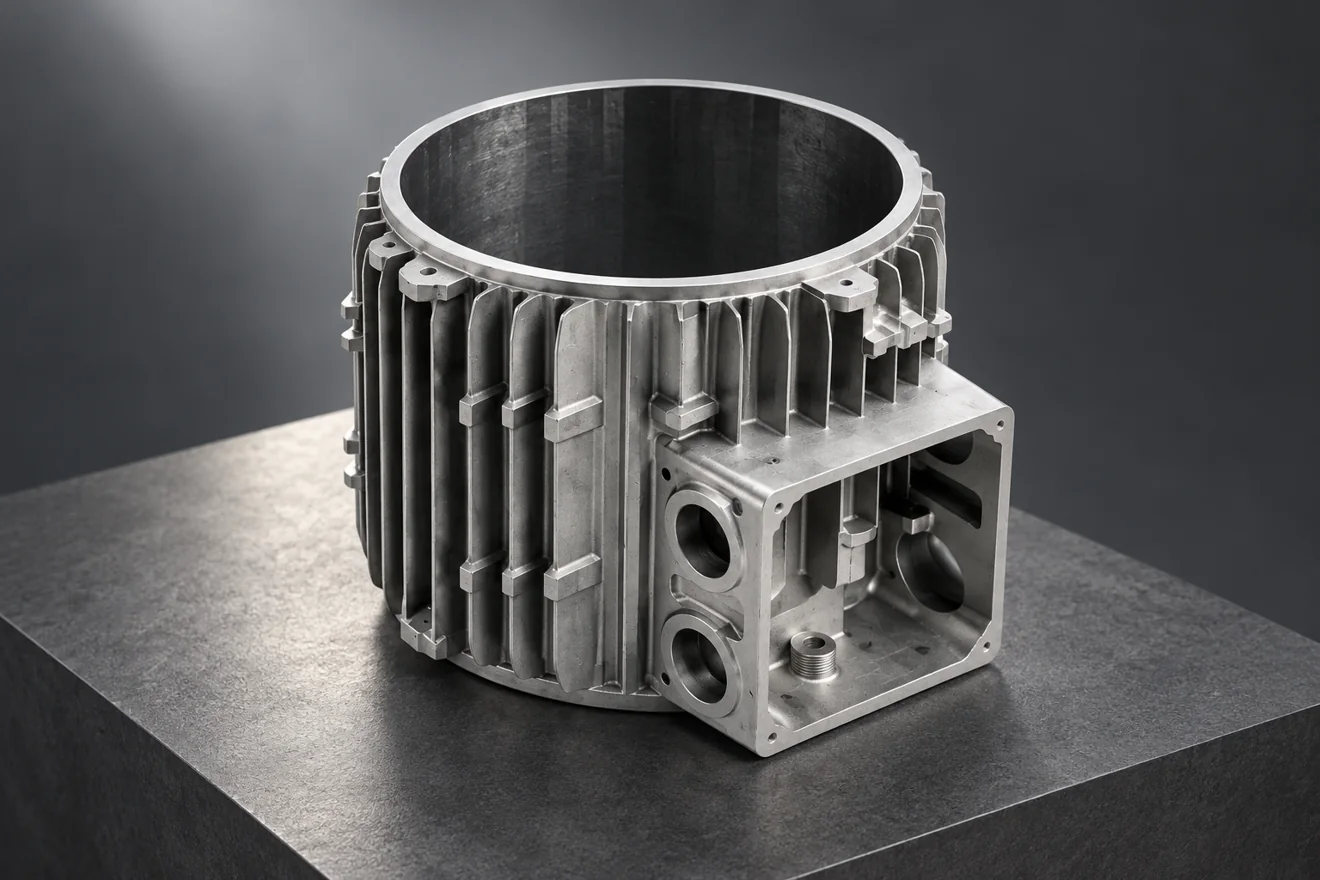
Relia can supply casting blanks for machining in your workshop. Send the finished drawing and first-setup plan so we can define local stock, accessible locating areas and blank receipt checks. Your finished tolerances remain separate from the foundry’s agreed blank-delivery requirements.
Read the overview and page sections
Send the finished drawing and your intended first setup. We use those together to discuss a blank that your fixture can hold and your tools can clean up, while keeping your finished dimensions separate from the foundry's delivery requirements.
The Foundry Blank Starts with Your Workshop Setup
Relia's casting-only review focuses on the surfaces your team will touch first: clamping pads, rough locating areas and faces that need machining stock. For a housing or flange, we relate those areas to the mold, cores and cleanup access. This helps you order a usable starting blank rather than pay for unwanted finishing.
Machining Stock Belongs on the Agreed Blank Definition
Extra material is useful only where the final route needs it. Too little can leave a surface uncleaned; unnecessary stock can increase cutting and disturb the intended wall balance. We review stock by feature and process, with the agreed blank drawing controlling the result rather than a universal allowance quoted without context.
04 / 10Component decisions
Define the Blank Your Workshop Can Actually Locate
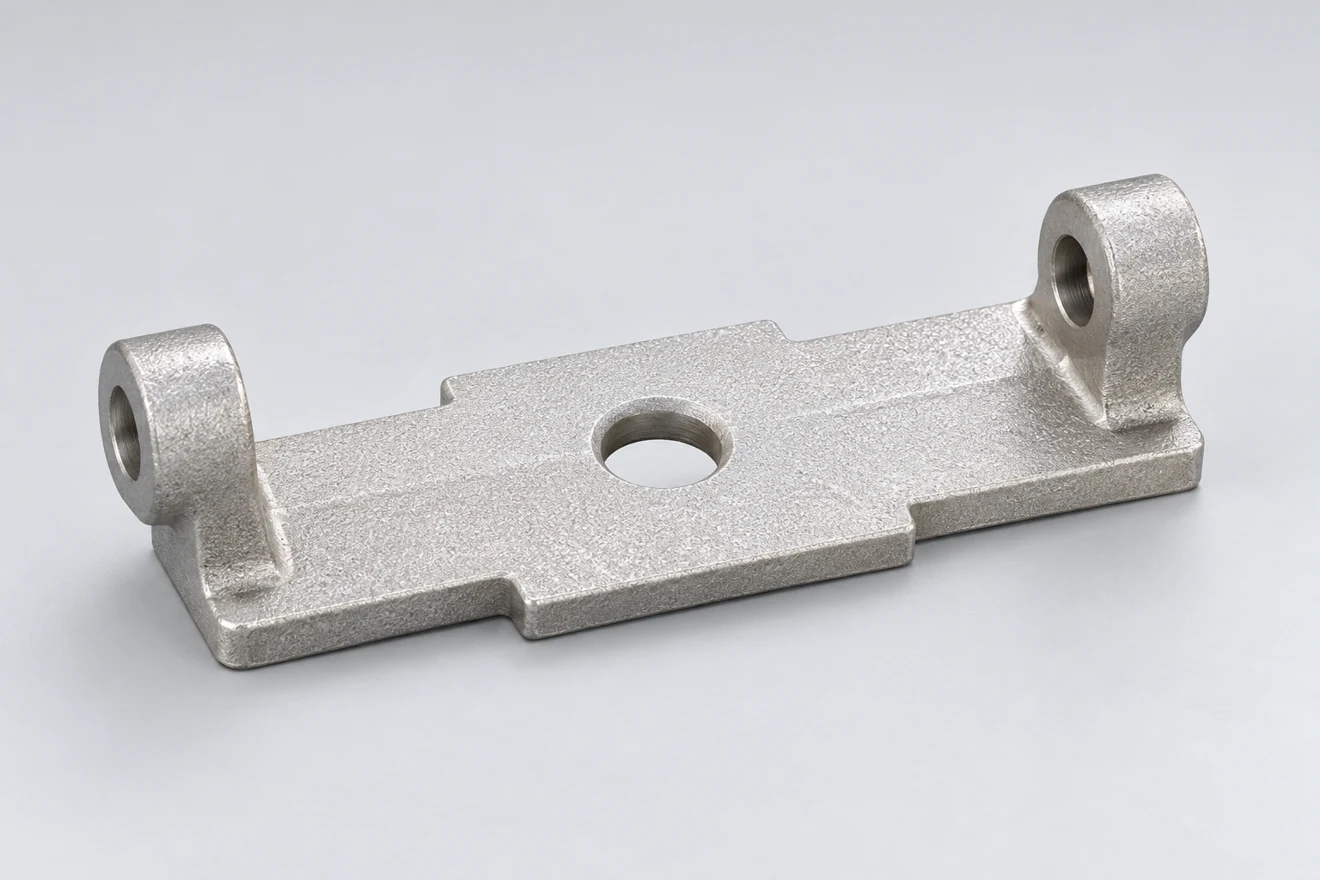
Machining allowance belongs to individual surfaces. A general extra-stock note can hide insufficient stock on one face and unnecessary cutting on another.
| Blank feature | Tell us about your setup | Agree before ordering |
|---|---|---|
| First locating pads | Where your fixture supports and clamps the casting | Pad position, cast tolerance and access |
| Bore and face stock | Finished surface and required clean-up direction | Local allowance on the blank drawing |
| Internal passages | Core geometry and areas your tools cannot reach | Core location and cleaning boundary |
| Cast-only regions | Clearances that stay unmachined | Cast envelope and visual acceptance |
Build Machining Stock into the Mold and Core Plan
The pattern or casting model includes the stock needed at bores, flanges and mounting pads.
- Workshop location
- Mold and cores
- Blank checks
- Protected handover
- Build recoverable stock into the blank
- Check the sample against your workshop setup
Open the manufacturing route and detailed review
Build recoverable stock into the blank
Parting direction and core location influence the variation your first setup must accommodate. Ribs and heavy junctions also affect feeding and cooling, so simply enlarging every surface is not a useful allowance strategy.
Check the sample against your workshop setup
Before repeat supply, a sample blank can be laid out against your fixture and machining plan. The useful result shows that the critical surfaces have enough recoverable stock and that the intended locating areas are accessible. Relia can discuss these blank-level criteria independently from the dimensions your workshop creates later.
Handover Checks Separate Blank Quality from Final Accuracy
Agree the blank dimensions, surface condition and material records required at receipt. Final bore fits and face relationships belong to your later machining and inspection unless separately included. If you need an integrity check before investing more machining time, identify its method, zones and acceptance criteria in the blank order.
07 / 10Component decisions
Review a Sample Blank Before Releasing Repeat Supply
The most useful trial follows your first machining operation. It shows whether the actual blank can reach the finished geometry from the proposed fixture references.
| Trial step | Check in your workshop | Information returned to the foundry |
|---|---|---|
| Locate | Confirm seating and clamping without distortion | Fixture interference or unstable pads |
| Rough machine | Check stock clean-up around critical cuts | Local shortages or excess stock |
| Finish the interfaces | Relate bores and faces to the finished drawing | Any datum or allowance changes |
| Freeze the blank | Record the accepted casting revision | One retained blank definition for repeats |
Transport Protection Preserves the Starting Condition
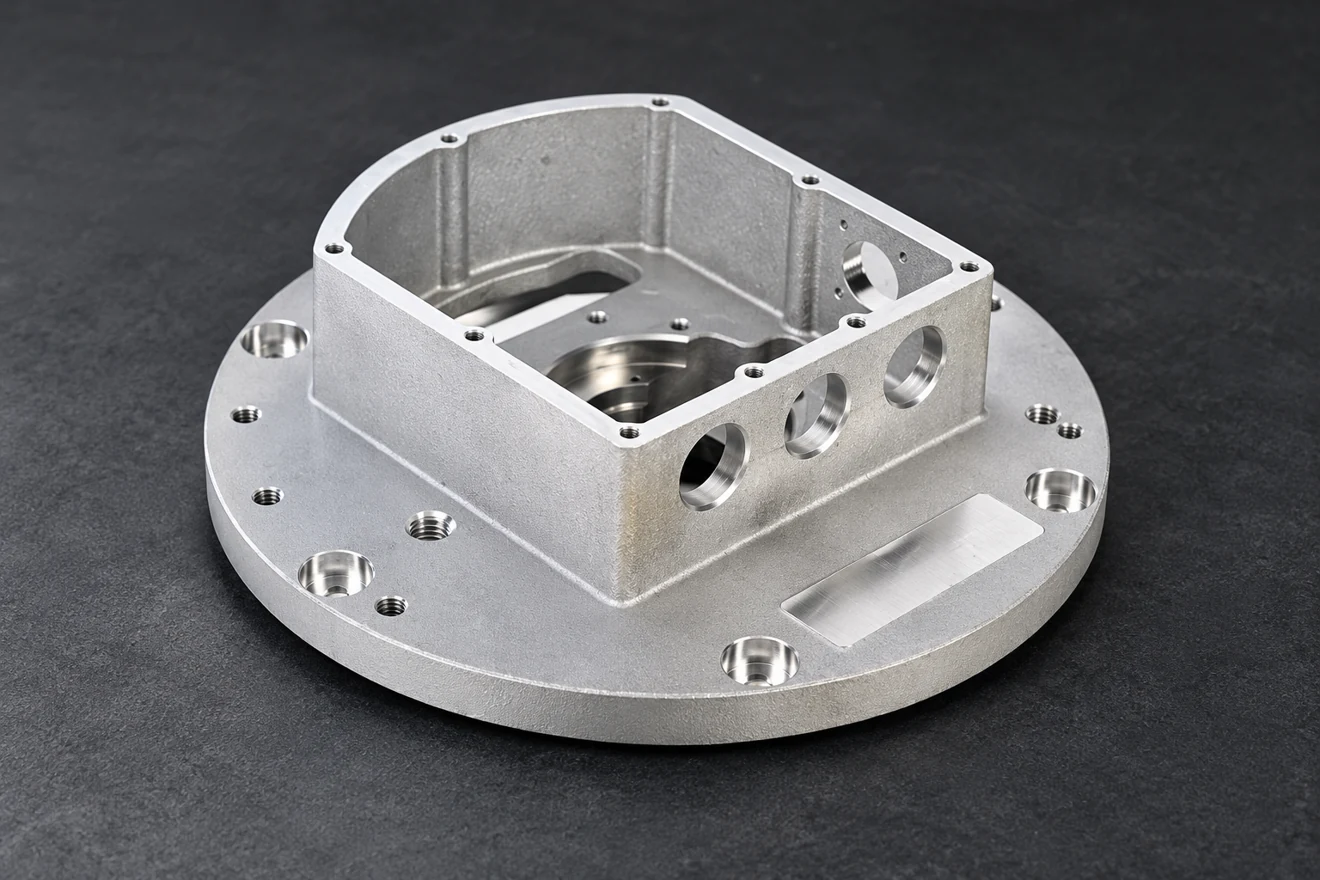
Packing should protect the contacts, stock and cast features you will rely on after receipt. Agree corrosion protection where appropriate to the selected material, how parts are separated and how lots remain identifiable. For an open housing blank, protect cavity access and flange edges from contact during handling. The packing arrangement is confirmed for the component and delivery route.
Send the Details for Your Component Review
Tell us what you need to buy and the condition you need to receive. Relia Casting will review the component, manufacturing scope and requested evidence with you before an order is agreed.
- Finished-part and casting-blank drawings
- Specified casting material
- Required machining stock by feature
- First-setup locating requirements
- Blank receipt checks and quantity
No. 96 Shuyuan Road, Qingdao, Shandong, China
About our component supply · Contact details and project enquiry