
Sand Casting for Housings and Machinery Parts
Relia makes drawing-based iron and steel sand castings for housings, valve bodies, brackets and bases. Your enquiry can cover a cast blank or a CNC-finished component. We review outside shape, internal cores and cleaning access together with the stock needed at the finished bores and mounting faces.
Review your housing and machining scope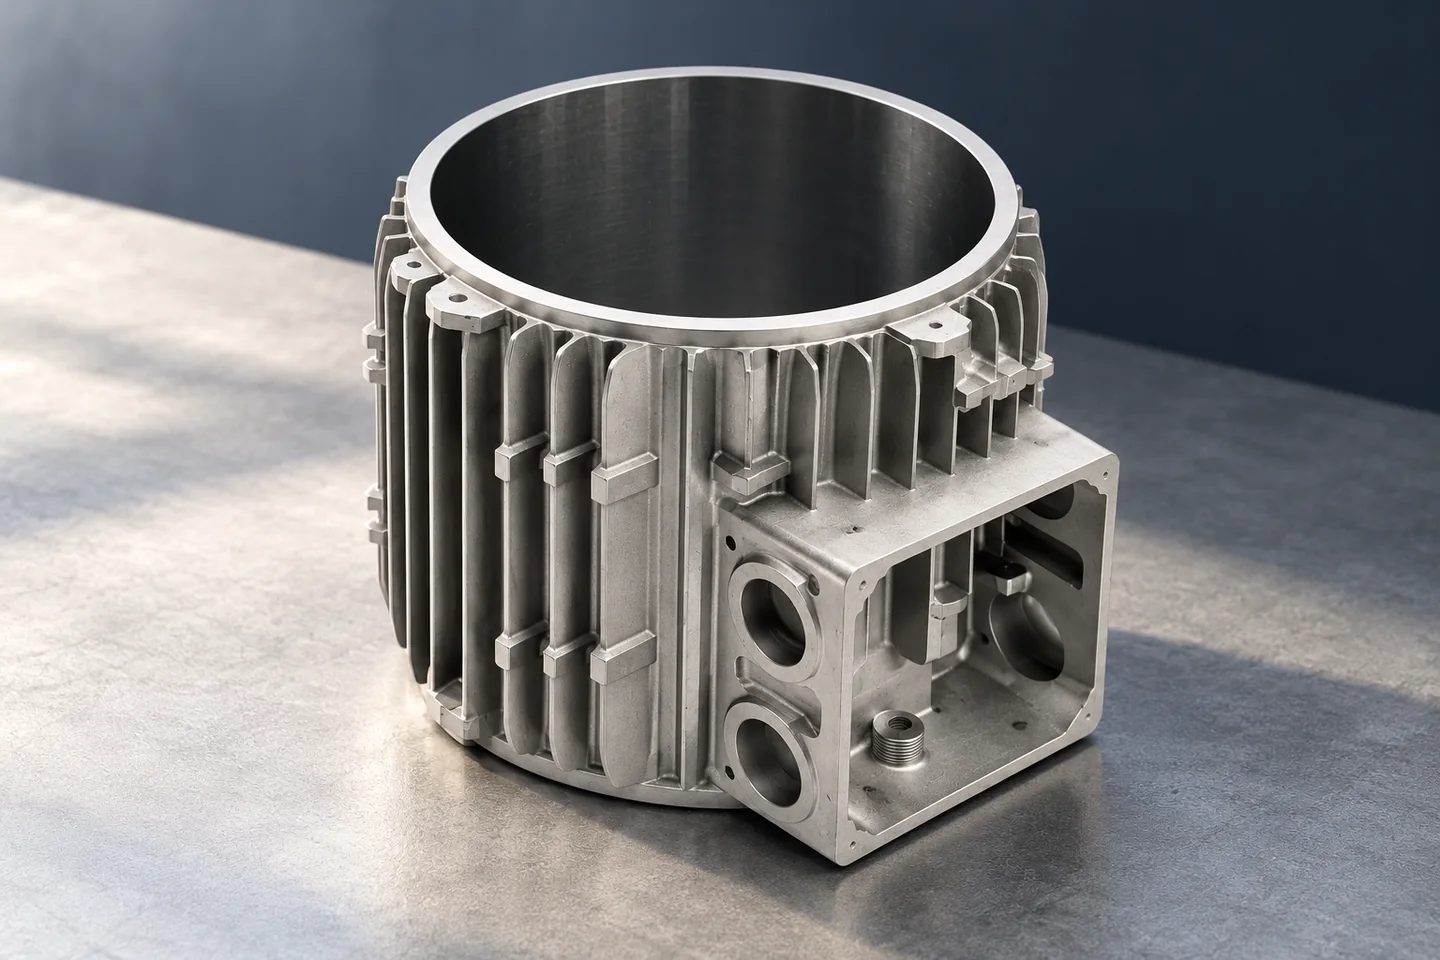
- MoldOutside walls, ribs and parting direction.
- CoreInternal spaces, support and removal access.
- CNCFinished bores, mounting faces and fixing patterns.
The Housing Drawing Connects Foundry and CNC Work
Relia reviews sections and finished contacts together. The grey-iron catalogue housing has an open cylindrical form, outside ribs and a side region; the iron valve-body reference adds flanged openings and internal passage questions. Those features determine different mold, core and cleanup needs. The order selects the actual component rather than treating the photographed assortment as one complete pump or valve.
- HousingWall sections and bore-to-base relationship.
- Valve bodyInternal boundary and connection faces.
- SupportRib junctions, seating plane and loaded contacts.
Pattern Withdrawal Establishes the Parting Plan
The reusable pattern must leave the mold without damaging the cavity. That makes draft, undercuts and parting location practical design issues. A dividing line near a flange or a fitted clearance may need a defined cleanup boundary. Where a cavity cannot be formed by straightforward pattern withdrawal, review a core or an alternative arrangement instead of assuming every recess is freely moldable.
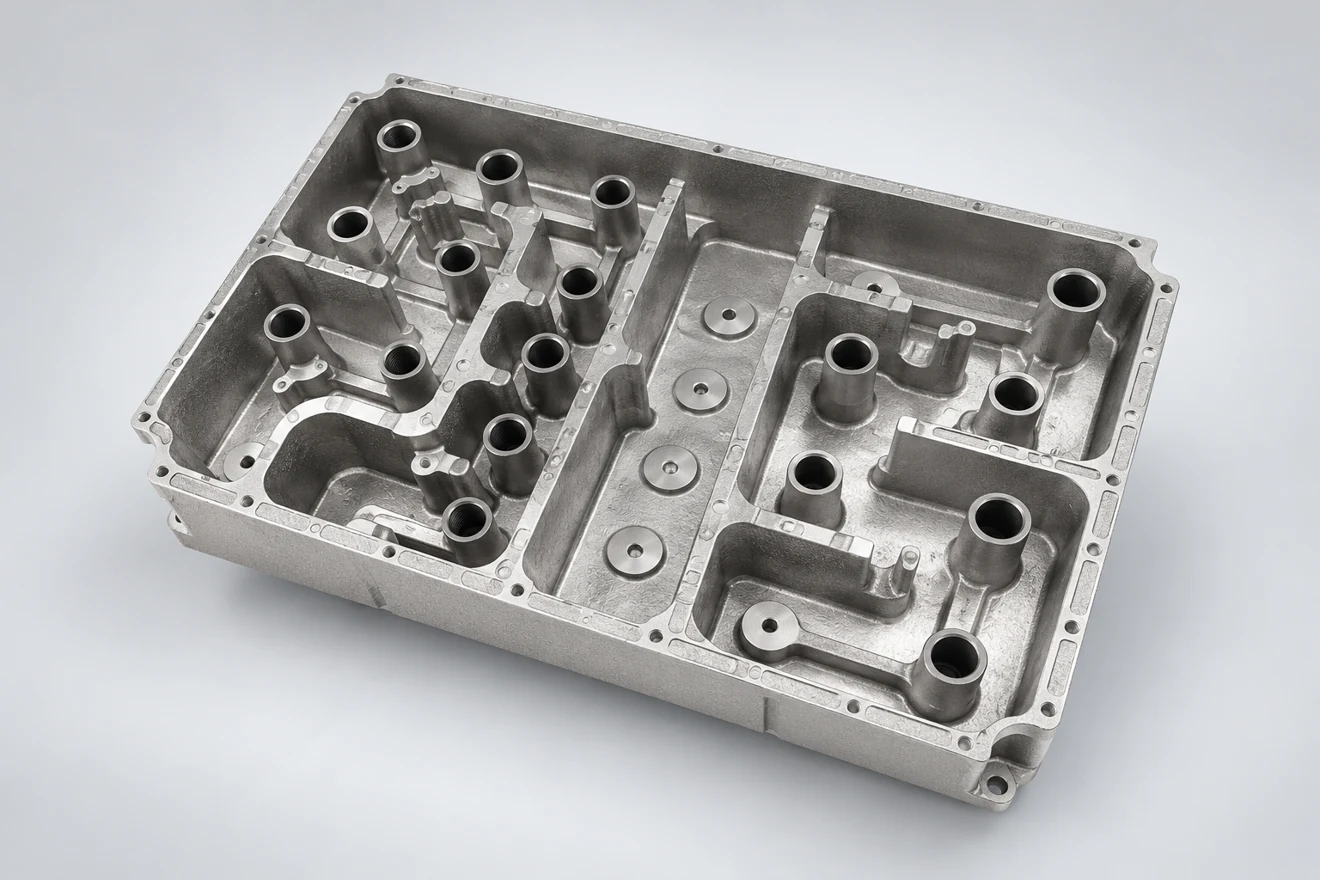
- WithdrawDraft and an accessible release direction.
- SeparateA practical mold parting arrangement.
- ProtectFunctional faces and nearby clearances.
Cores Need Support and a Removal Route
A core establishes an internal space but must remain located as the mold is handled and filled. Its seating and stiffness affect the material left around a later bore. After casting, the internal spaces need access for the agreed core removal and cleaning. An outside drawing alone cannot show those constraints, so housing and passage projects need useful sections through the internal geometry.
Define core seats and support during mold handling and filling.
Relate the core to the later bore so the required wall remains after machining.
Keep an accessible route for the agreed internal cleaning after casting.
Iron and Steel Require Different Material Decisions
Grey iron, ductile iron and cast steel are separate material choices, not interchangeable names for a dark casting. The grade, relevant properties and delivered condition are selected for the part’s duty. A bracket with impact exposure may lead to a different material review from a machine base selected for damping. We assess the chosen metal with local sections and final contacts before confirming the production proposal.
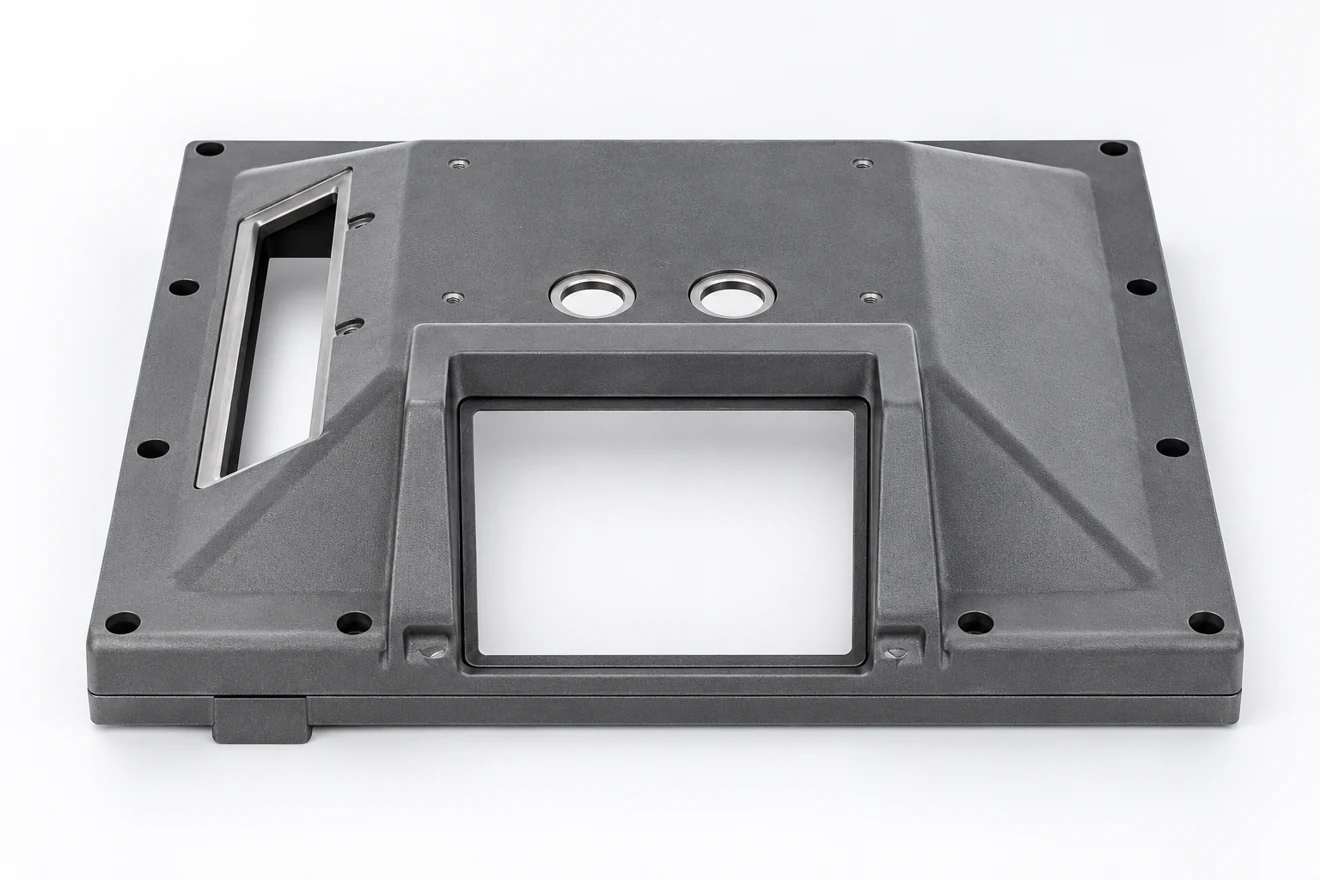
- Grey ironReview the specified grade and housing or base duty.
- Ductile ironReview load direction, ductility and the actual grade.
- Cast steelReview the material condition and relevant property evidence.
Heavy Junctions Need a Soundness Plan
A broad boss adjoining thin walls can remain liquid after the nearby sections begin to freeze. Feeding and the local section layout must address that region. Simply making every wall thicker can add metal while preserving the same difficult junction. We review transitions with the drawing and the later machined surfaces, because a sound exterior alone does not describe the material exposed by a deep cut.
- Section layoutWhere local metal mass accumulates.
- SolidificationThe regions needing an effective feeding arrangement.
- Final cutThe material required at working interfaces.
Stable Supports Turn the Blank into Related Contacts
An open housing or broad plate can distort under clamping. The machining plan starts with suitable support points and a first reference, then relates the bore, base and hole pattern through subsequent setups. Stock should be checked at every important cut; a correct outer envelope does not guarantee adequate cleanup around an offset internal feature.
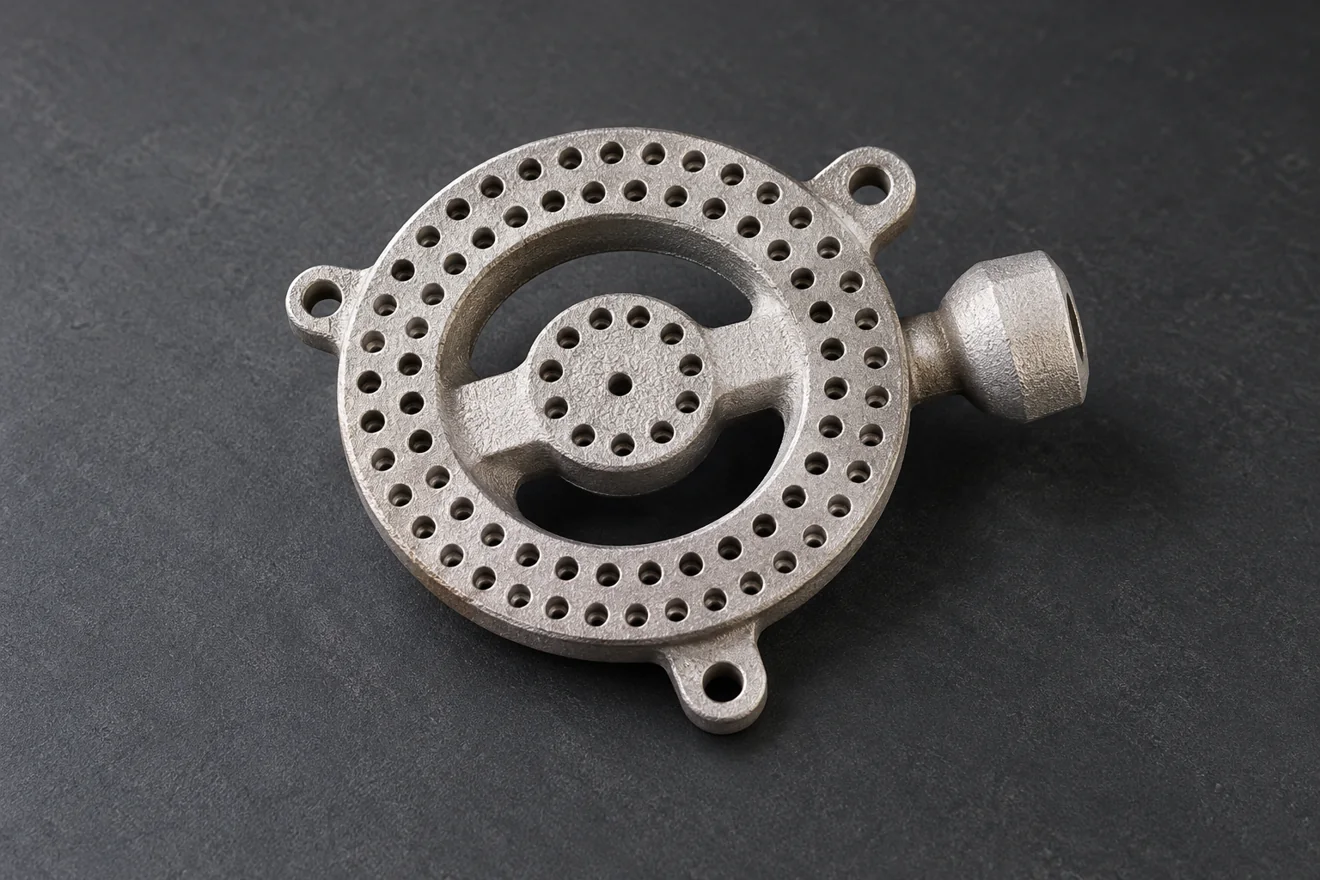
- SupportRestrain without forcing thin or broad regions.
- ReferenceCreate the first useful datum.
- FinishRelate working features to the assembly drawing.
Acceptance Separates the Blank from the Finished Part
The casting drawing identifies as-cast envelope, allowed draft, cleanup and stock. The finished drawing controls machined size and relationships. Add internal cleaning or integrity requirements where the function needs them, and define any pressure or leakage test independently. Relia can provide agreed key-dimensional records with inspection scope and sampling stated for the order.
- As castEnvelope, section, cleanup and local stock.
- MachinedBores, faces and position from functional datums.
- ApplicationOnly the tests specified for the actual duty.
Move from the Route to a Specific Housing Decision
The detailed pages distinguish pump housings, support bases, valve bodies, tooling economics and supplier transfers. Smaller technical notes address core movement, residual sand and first-operation references. Use them to resolve a defined manufacturing concern without duplicating the entire procurement guide.
Contact the Casting Team
Provide the component sections, actual material, quantities and final drawing. Identify internal cleaning access, core-sensitive walls and the surfaces to be machined.
Qingdao Reliacasting Co., Ltd.
Drawing-based metal castings and CNC-finished OEM components from China.
Qingdao officeNo. 96 Shuyuan Road
Qingdao, Shandong, China
Arrange a project visit with us before travelling.
The released drawing, selected material and agreed order define the supplied component and required acceptance evidence.