
01 / 10 · Buy a blank that fits the machining plan
Machining-Stock Maps for Precision Casting Blanks
Your machining team needs stock at each final cut, not only an overall blank allowance. Relia reviews precision-casting blanks against the finished model and first setup. Mark bores, faces and protected thin walls so the incoming checks address the material that must remain available.
The surfaces and material required in service.
The agreed material available for each finishing operation.
The casting condition and checks used at handoff.
Relia reviews that map with your machining team and the first-operation locating concept.
Review your local stock map02 / 10 · Foundry and machine-shop agreement
A Local Stock Agreement Instead of a General Allowance
Relia connects casting geometry to the surfaces your workshop will machine. We identify required cleanup zones, retained cast regions and the references used to assess the blank.
Feature-specific
Bore stock, face stock and nearby remaining sections reviewed together.
Condition-specific
Blank acceptance tied to the agreed treatment and delivery state.
03 / 10 · Controlled geometry
The Finished Component Inside the Casting Envelope
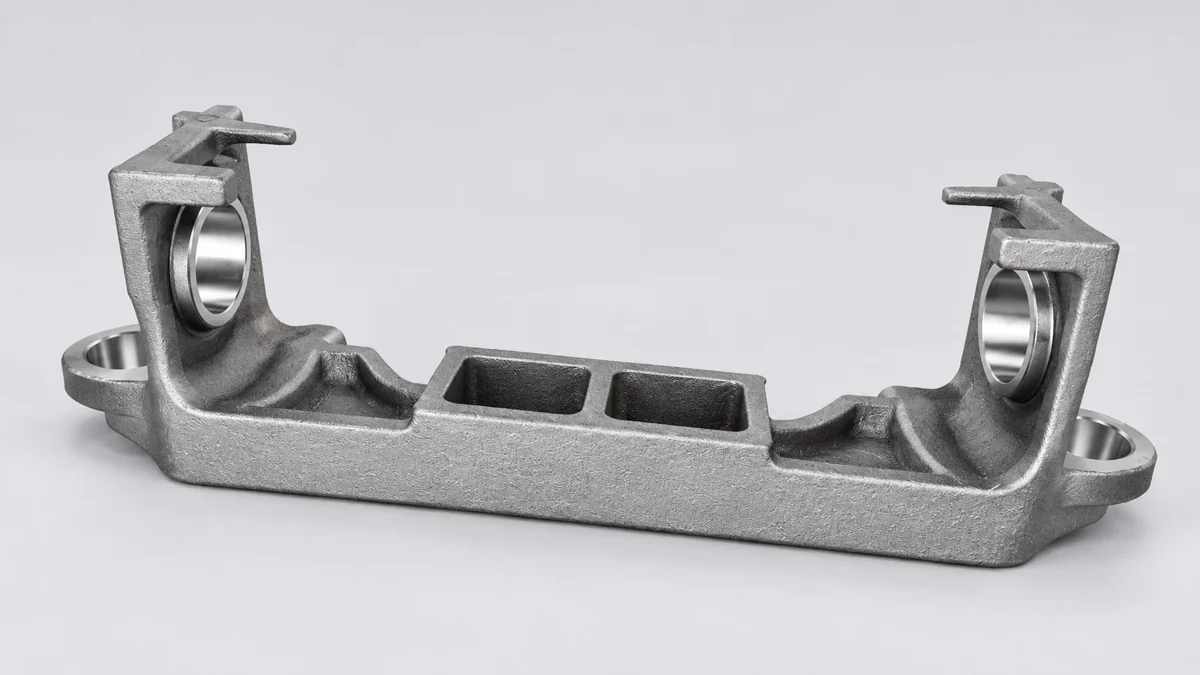
Provide cast and finished models on the same coordinate basis, with matching revisions. Mark the first-operation contacts and the final drawing datums.
Resolve differences between the casting and machining drawings before the order. Stock for finishing and allowances used to develop tooling are distinct items in the review.
Define the casting-blank delivery handoff04 / 10 · Internal features
Stock at Bores and Recessed Features
Review the unmachined opening relative to the intended finished bore.
Identify regions that must fully clean up after machining.
Retain the required section around the finished opening.
One measurement at the entrance may not represent the stock deeper in a recess. Agree the accessible sections or other verification approach needed for the actual feature.
Make the locating setup part of stock acceptance
A stock assessment depends on the casting's position relative to the finished geometry. Identify the agreed support and reference setup rather than accept an unexplained overall dimension.
05 / 10 · Faces and interfaces
Stock at Flanges and Locating Faces
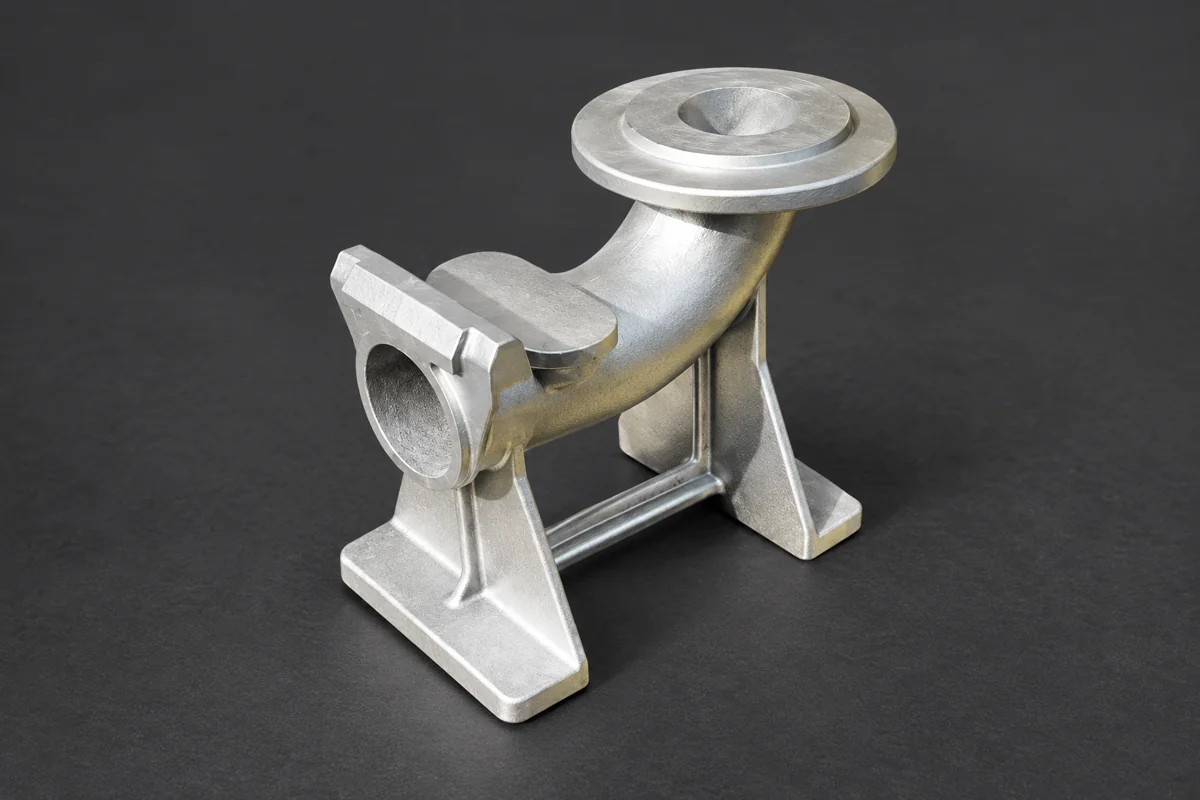
Show the material required at each finished face, including its relationship to bores and mounting holes. Identify local high or low regions that affect the intended setup.
Review the first face to be created and the contacts available before it exists. A temporary locating feature needs its own retained or removed condition.
06 / 10 · Material that must remain
Thin Walls and Protected Material Boundaries
Remove
Agreed stock at designated machining regions.
Preserve
Minimum finished sections, contact edges and protected cast geometry.
Extra external stock is not permission to shift a bore into a protected wall. Review the cast-to-finished relationship locally and record any exception before machining.
07 / 10 · Delivered-blank evidence
Verification Points on the Delivered Blank
Identify the surfaces or points checked, their reference setup and the stage of measurement. Link the result to the blank and drawing revision.
Relia can provide agreed key dimensional records. Define the characteristics and sampling frequency per order, including how an apparent lack of stock is handled before cutting begins.
08 / 10 · Component references
Flanged and Bored Component References
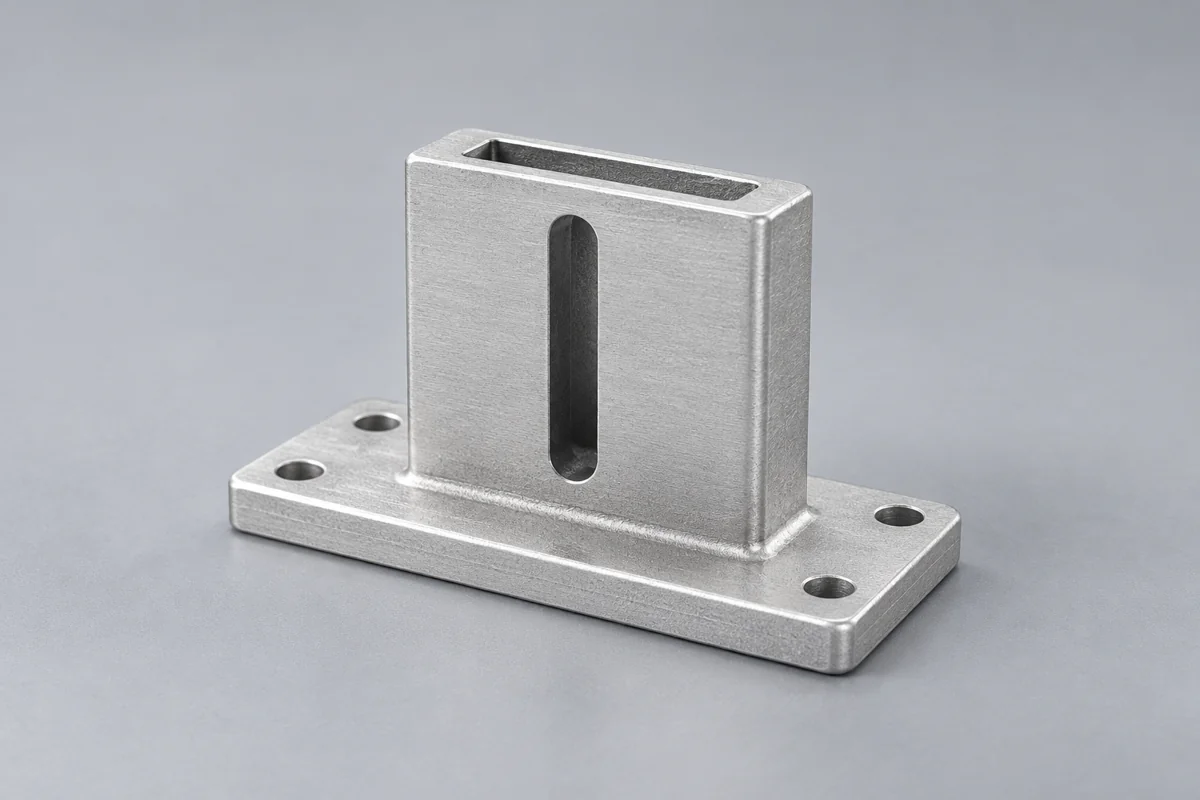
Bored supports, flanged bodies, slotted mounts and fork ends place finishing material in different regions. Start from the relevant form and supply your own cast and finished requirements.
View bored support casting enquiriesView flanged body casting enquiriesConnect stock to as-cast and machined tolerance planning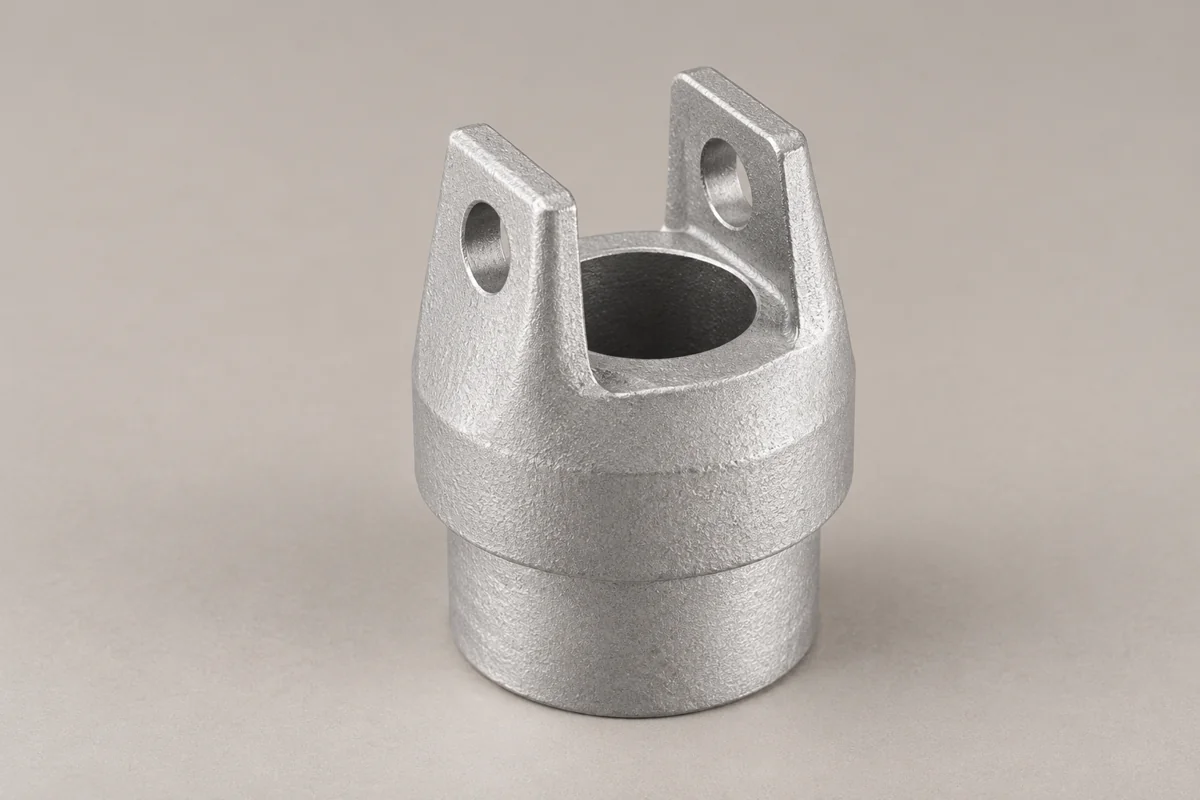
09 / 10 · Order release
Agree Cleanup Exceptions Before the Order
Identify cleanup zones and protected geometry.
Agree sample checks and delivered-blank evidence.
Approve samples and resolve documented exceptions before the batch.
Keep the stock map with the controlled drawing so later revisions reach both casting and machining teams.
10 / 10 · Start the stock review
Send Cast and Finished Models for Stock Review
Send Relia both models, material, quantities and your locating concept. Mark full-cleanup surfaces, protected sections and the checks required on delivered blanks.
Email the cast and finished geometry- [email protected]
- Phone
- +86 185 6176 2631
- +1 404 203 0971
- Company and address
- Relia Casting
No. 96 Shuyuan Road
Qingdao, Shandong, China