
Silica-Sol Shell Planning for Lost-Wax Steel Casting
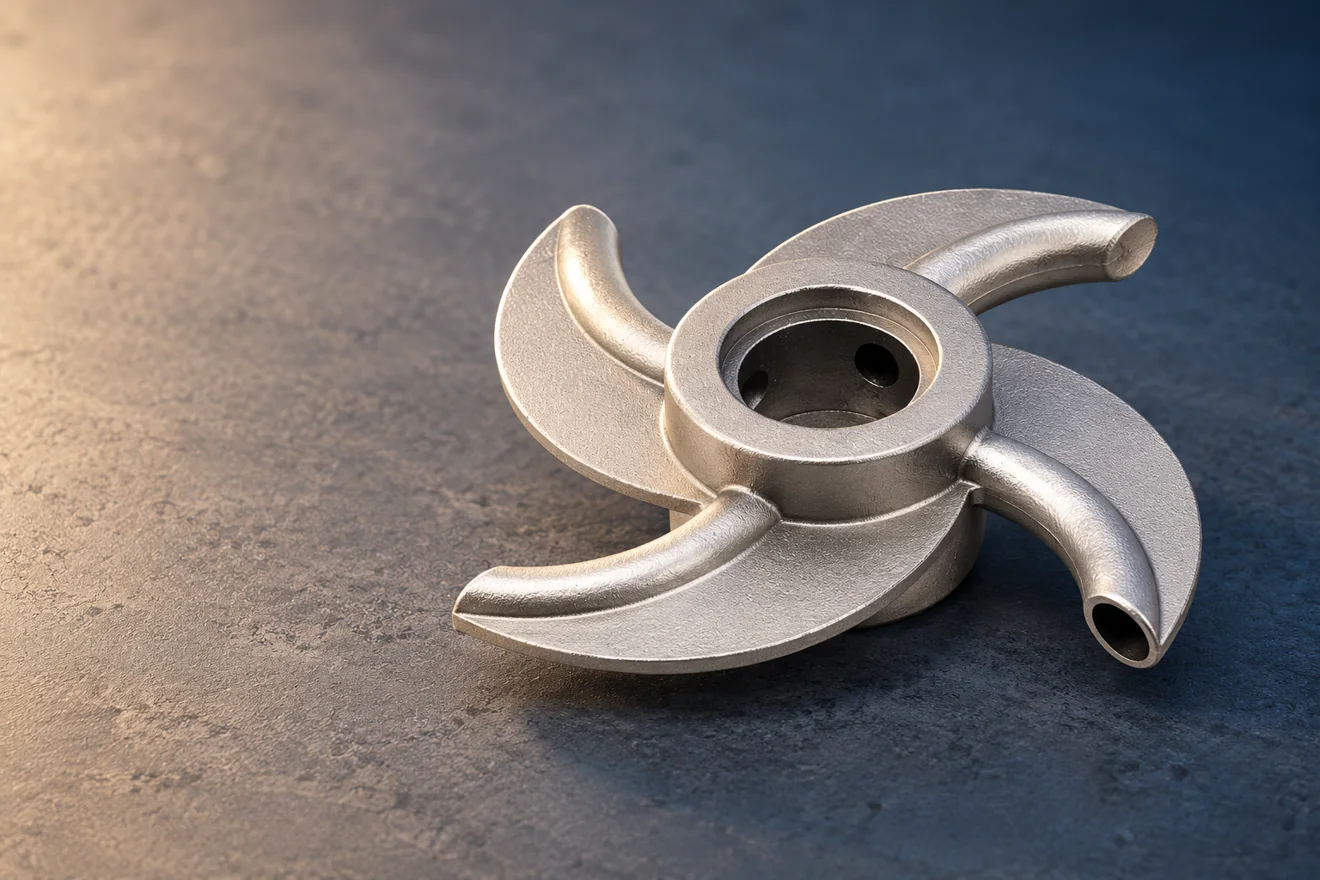
You can review the wax-pattern and ceramic-shell plan for your silica-sol steel casting with Relia before tooling decisions are fixed. We connect thin regions, recesses, cleanup openings and the stock needed for final machining. This page helps you define the mold-system review for the actual component, rather than treating a shell binder name as proof of finished precision or service performance.
Read the overview and page sections
We explain how shell preparation, casting cleanup and selected CNC operations relate to the part. The enquiry buys a defined component and acceptance scope, rather than assuming that a shell-binder name alone guarantees a particular tolerance or surface result.
The Finished Component Leads the Shell-Process Review
Relia connects the lost-wax component model with the surfaces the ceramic mold must reproduce and the regions that later work must reach. We distinguish pattern changes, shell access, metal-casting considerations and final CNC contacts. That makes the planning discussion specific to your component instead of repeating the general investment-casting overview.
03 / 10Component decisions
Understand What the Silica-Sol Shell Contributes
The ceramic mold is built around a sacrificial pattern. It provides the casting form, while the complete process and later operations determine the delivered component.
| Process stage | Purpose | Part-specific review |
|---|---|---|
| Pattern preparation | Represent the component and casting arrangement | Wall features, access and local stock |
| Shell building | Create a layered ceramic mold | Coverage, drying and difficult recesses |
| Dewaxing and casting | Remove the pattern and form the metal blank | Alloy, sections and pouring arrangement |
| Cleanup and finishing | Separate and finish individual castings | Shell removal, gates and final contacts |
Connect Shell Building with Casting and Final Finishing
The lost-wax route begins with the pattern and its gating arrangement.
- Pattern definition
- Shell formation
- Cast cleanup
- Final scope
- Connect pattern and shell preparation
- Carry the cleaned blank into finishing and acceptance
Open the manufacturing route and detailed review
Connect pattern and shell preparation
Refractory slurry and stucco layers build the shell, with controlled drying between stages before dewaxing and preparation for pouring. Shell coverage and handling need to suit the component's recesses and section changes; the binder name does not remove those manufacturing constraints.
Carry the cleaned blank into finishing and acceptance
After solidification, shell removal, gate separation and cleanup produce the blank for the agreed finishing work. Relia's review connects the cast form with the stock and locating features needed by CNC operations. The sample and final acceptance should refer to the ordered alloy, geometry and supplied condition, with separate limits for cast and machined features.
Connect Difficult Geometry with Shell and Cleanup Access
A recess or vane-like feature creates several connected questions. The pattern must represent the approved shape, shell material must form the relevant surface, and the resulting mold material must be removable after casting. A feature that looks open in an outside view may still have a restrictive internal neck or a hidden pocket.
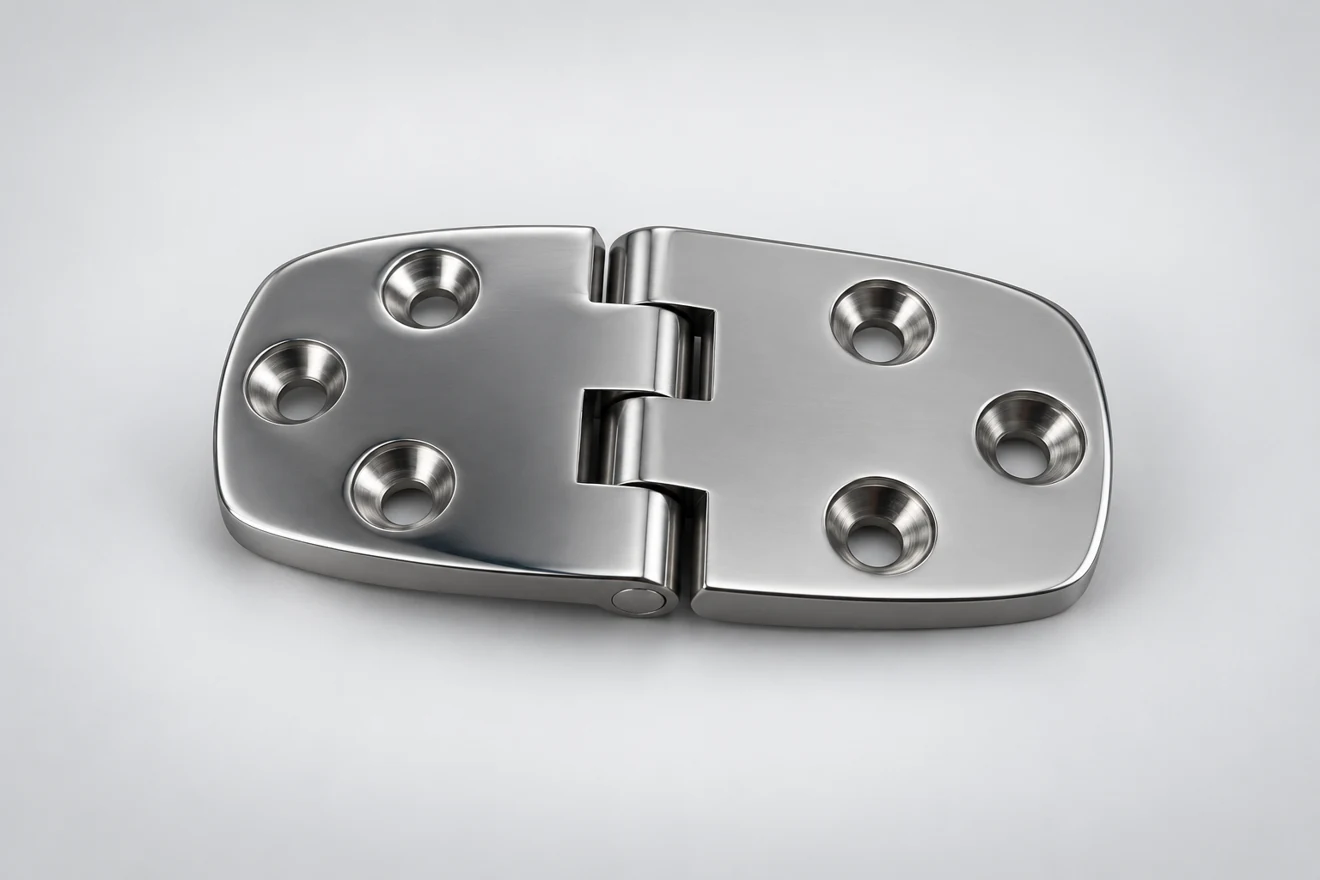
Relia reviews those regions using the component model and sections, with local finishing stock included at the working contacts. Any proposed change is checked against your functional and assembly constraints before approval. The sample review then focuses on the named difficult features; a catalogue form illustrates the discussion without establishing a measured wall limit, hidden quality or rotor rating.
Pattern features, slurry and stucco access, local coverage and drying.
Shell removal, openings and cleanup access after solidification.
Review both directions on the actual section view. Reserve final-machining stock without blocking the access path.
As-Cast and Machined Requirements Stay Separate
Define which surfaces remain cast and which require CNC work or another finishing operation. State their acceptance requirements and datum relationships. The process review should not convert every functional fit into an assumed as-cast feature simply because the order uses precision or silica-sol terminology.
07 / 10Component decisions
Buy the Final Condition Alongside the Casting Route
Two quotations can both name silica-sol casting while including different machining or inspection work. Make the delivered boundary comparable.
| Order item | Define for the component | Acceptance output |
|---|---|---|
| Material | Actual casting grade and required condition | Relevant material record |
| Geometry | Cast envelope and machined interfaces | Feature-specific dimensional acceptance |
| Surface | Required cleanup, finish and protected areas | Defined supplied surface state |
| Evidence | Sample, dimensional and any special-test scope | Records linked to part and revision |
Sample Approval Tests the Agreed Route and Scope
Agree the dimensional, surface, integrity and application evidence needed for the sample. Identify the component revision and route being evaluated. Where recurring production needs additional checks or records, keep them explicit rather than assuming the sample result guarantees every later batch or variant.
Send the Details for Your Component Review
Tell us what you need to buy and the condition you need to receive. Relia Casting will review the component, manufacturing scope and requested evidence with you before an order is agreed.
- Controlled component drawing and model
- Actual material and supplied condition
- Mandatory or proposed silica-sol route
- Cast, machined and surface requirements
- Sample and batch evidence with quantities
No. 96 Shuyuan Road, Qingdao, Shandong, China
About our component supply · Contact details and project enquiry