
01 / 10 · Internal casting cleanout
Core Removal and Residual Sand in Resin-Sand Pump Housings
For a resin-sand pump-housing order, agree both the core-removal scope and the internal condition required at delivery. Relia reviews the actual cavity and access openings with you; cleaning a passage and verifying its acceptance are separate tasks.
Relia reviews passage sections, removal access and the required delivered condition with your team. The agreed scope identifies what is cleaned, what can be inspected and which records are needed.
Review your housing cleanout scope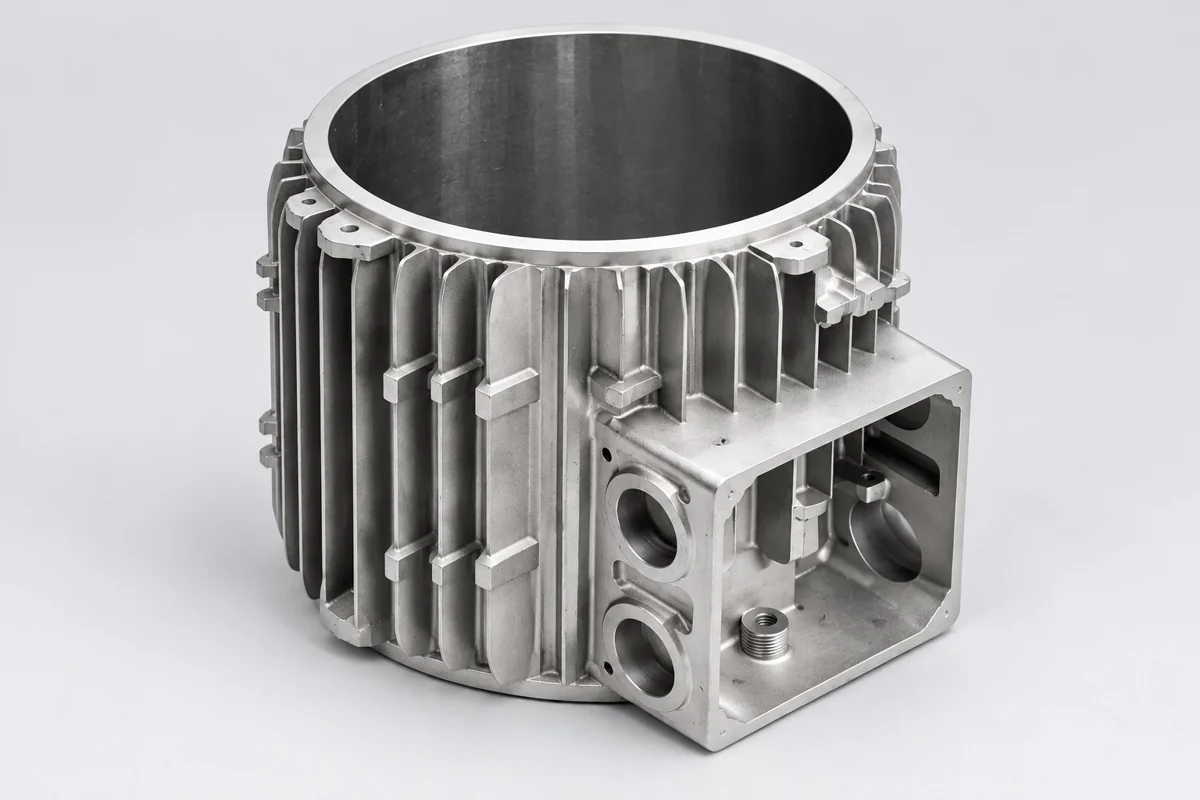
02 / 10 · Factory delivery scope
A Cleanout Scope Defined with the Housing Geometry
Relia connects the resin-sand casting proposal to the cavities on your actual drawing. Internal sand removal, machining residue and final cleanliness are identified as distinct responsibilities.
Break down and remove the core through the available access.
Choose operations that address the agreed residue and component condition.
State coverage, method and any required record.
03 / 10 · Internal features
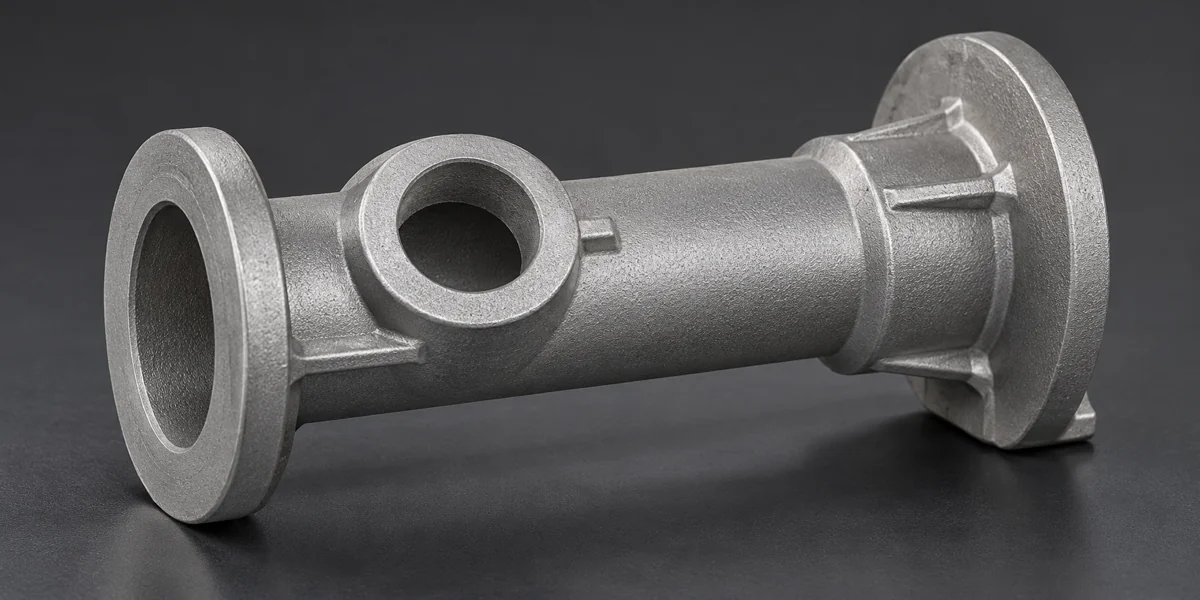
Passages and Pockets That Retain Sand
Show bends, blind pockets, intersecting passages and restricted openings in section. Identify areas that a straight exterior view cannot reveal.
Include the surface condition and residue concern relevant to the component's use. A general request for a clean casting does not define the coverage or acceptance needed in a fluid-handling assembly.
Review pump-housing casting and finished-interface requirements04 / 10 · Core removal planning
Core Breakdown and Removal Access
A sand core forms internal geometry that the exterior mold cannot create on its own. After casting, the removal route must reach that core through the openings available in the component.
Show the complete cavity
Connect internal sections to each usable opening and restricted region.
Define the removal route
Review the proposed breakdown and removal operations with the actual core and alloy.
Review restricted regions before tooling approval
If the proposed geometry restricts removal or verification, resolve the access requirement with engineering. Any opening or geometry change needs approval against the working component.
05 / 10 · Sequence and access
Openings Available Before Final Machining
Identify which openings exist in the casting and which are produced later. Cleaning and inspection access can change as machining operations expose additional surfaces or close a temporary opportunity to reach them.
Keep the internal cleanout proposal connected to that sequence. Also specify how machining chips, burrs or other later residue are handled before the final delivery check.
06 / 10 · Process and evidence
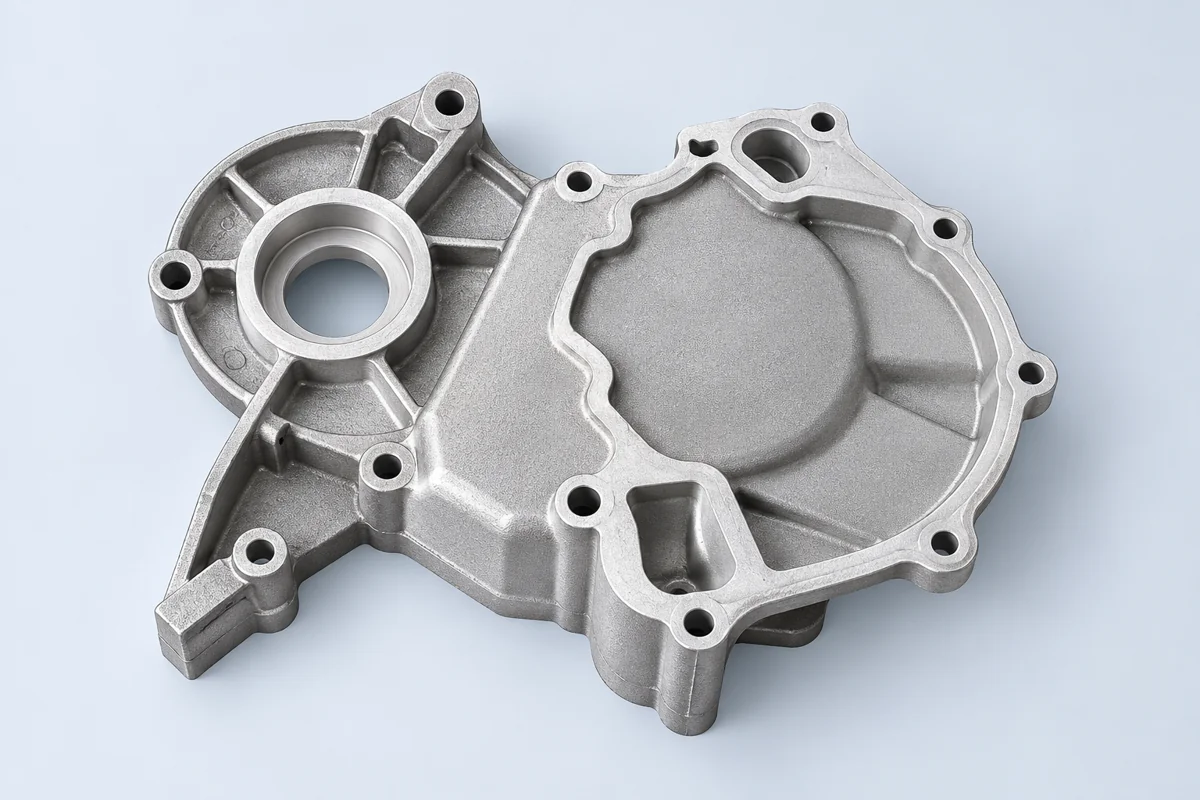
Cleaning and Inspection Are Separate Operations
Apply the agreed cleaning route
Specify the surfaces and residue addressed, with compatibility for the component and its condition.
Check the agreed result
Define the inspected region, method, acceptance and required documentation.
A visible external surface does not establish the condition of a hidden pocket. Likewise, one cleaning operation should not be assumed to verify every internal region.
Separate internal deburring, machining residue and final cleanliness requirements07 / 10 · Inspection scope
Residual-Sand Acceptance and Inspection Coverage
Identify the passage, pocket or surface zone.
Agree how that region can be evaluated.
Define the condition required for acceptance.
Specify evidence and the agreed sampling frequency.
Discuss inaccessible regions before production. The acceptance plan should state what the selected method covers and how any unresolved access issue is handled.
08 / 10 · Catalogue references
Pump Housing and Fluid Component References
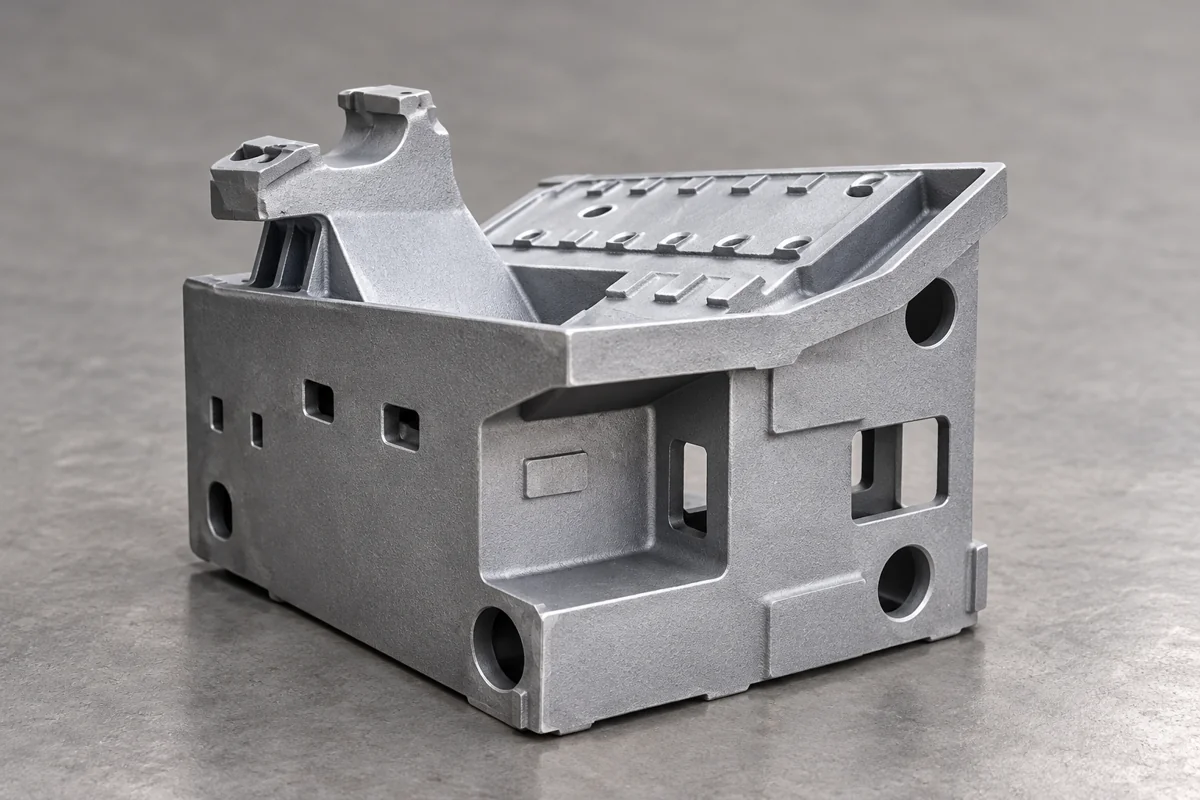
Use the selected housing geometry to begin the enquiry, then attach its actual passage sections and cleanliness requirements. Open structural forms and hollow connectors show different access situations.
View industrial resin-sand housing and pump-part enquiriesView hollow bodies, covers and open casting forms09 / 10 · Delivery responsibilities
Responsibility at Each Delivery Stage
Define the blank supplied to the next operation.
Address residue introduced or revealed by finishing.
Record acceptance in the specified supplied condition.
Approve the sample and cleaning scope before arranging batch production. Keep packaging and handling requirements connected to the accepted final condition.
10 / 10 · Start the cleanout review
Send Passage Sections and Cleanliness Requirements
Send Relia the housing drawing, material and quantities. Mark hidden pockets, available openings and the required delivery condition, including any inspection or residue acceptance specification.
Email the passage sections- [email protected]
- Phone
- +86 185 6176 2631
- +1 404 203 0971
- Company and address
- Relia Casting
No. 96 Shuyuan Road
Qingdao, Shandong, China