
Stainless Valve Body Investment Casting and Machined Sealing Interfaces
Relia reviews stainless valve-body castings with ports, threads and sealing contacts finished to your drawing. We connect passage access and cleanup with the machining scope and any ordered body test. Define the body and included hardware clearly, so its acceptance is separate from the complete valve assembled later.
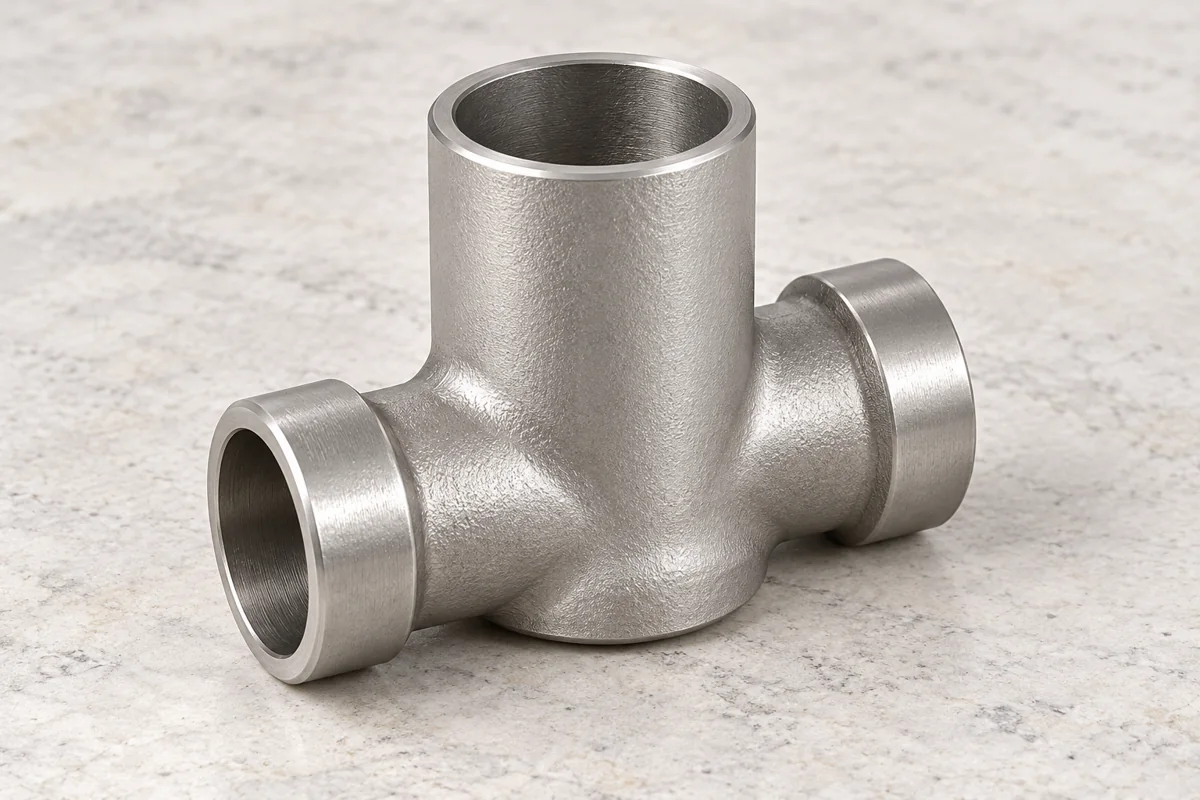
A Supplied Body Has a Defined Test Boundary
Relia reviews the valve body from its internal passage to the finished connection faces. We identify which openings are formed, which are machined, and which closures or internal parts belong to another supply item. That gives the material, machining and any test discussion the same component boundary instead of relying on an undefined promise of leakproof performance.
Actual body geometry, internal passage and selected material.
The ports, threads, seats and faces included in the machining scope.
Passage Sections Connect the Ports and Sealing Areas
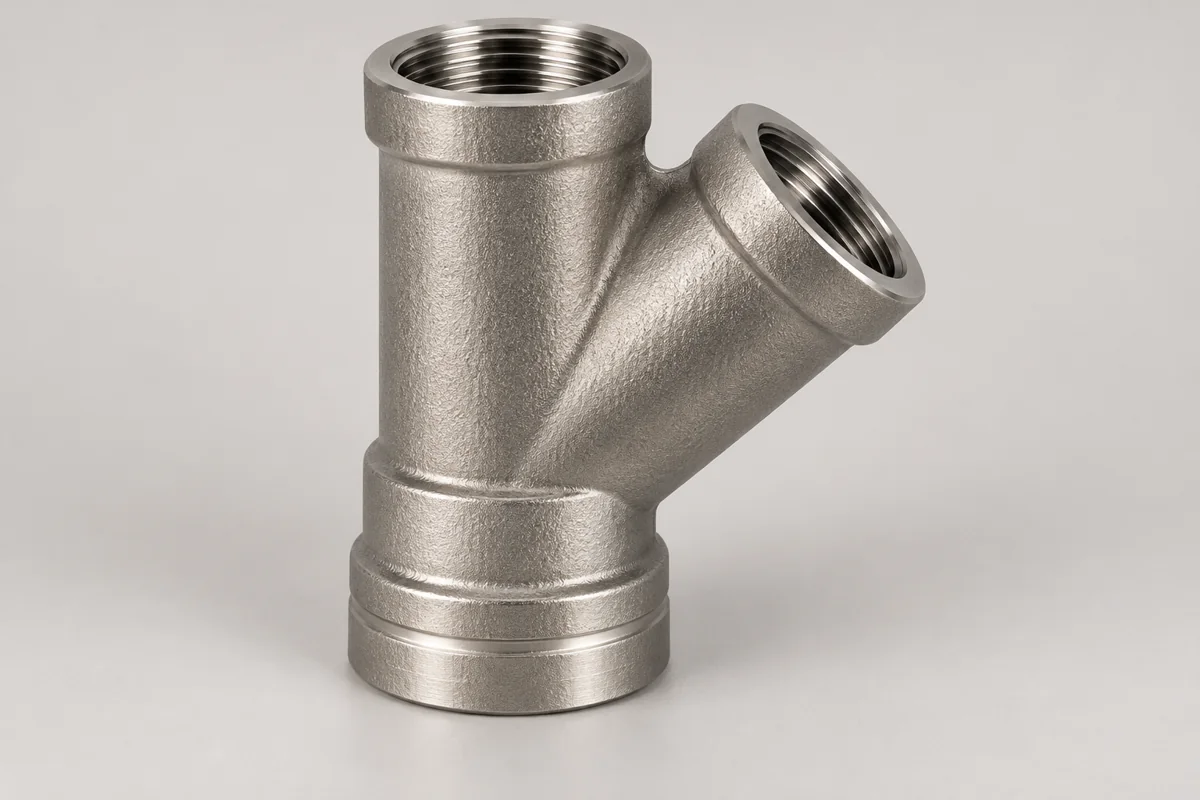
An outside view shows port positions but leaves the internal passage uncertain. Section views help us discuss wall transitions, core or pattern access and the material available around threads and seats. Include intersecting passages and local sections where a final machining cut approaches the flow boundary.
The Medium Guides Material and Surface Decisions
The medium, temperature and cleaning environment belong in the material brief. Specify the actual cast-alloy standard and delivered condition rather than relying on a stainless name alone. Food-contact use introduces its own applicable requirements and documentation; it is not established by the appearance of a polished fitting.
Clean the Cast Passage Before Finishing Threads and Seats
Lost-wax casting creates the body form through a pattern and ceramic mold; the working threads and seats may still require CNC finishing. Mold-material removal needs access to the actual internal regions. That cleanup should not consume the local stock reserved for a sealing shoulder, thread entrance or flange face.
Relia connects the cut sequence with the final passage condition. Machining an intersecting port can create a new burr after the casting has been cleaned, so the plan includes access for subsequent deburring and final cleaning. If a body test is ordered, its closures, conditions and acceptance result must describe the boundary after the relevant material removal.
Seal Geometry Needs More Than a Smooth Appearance
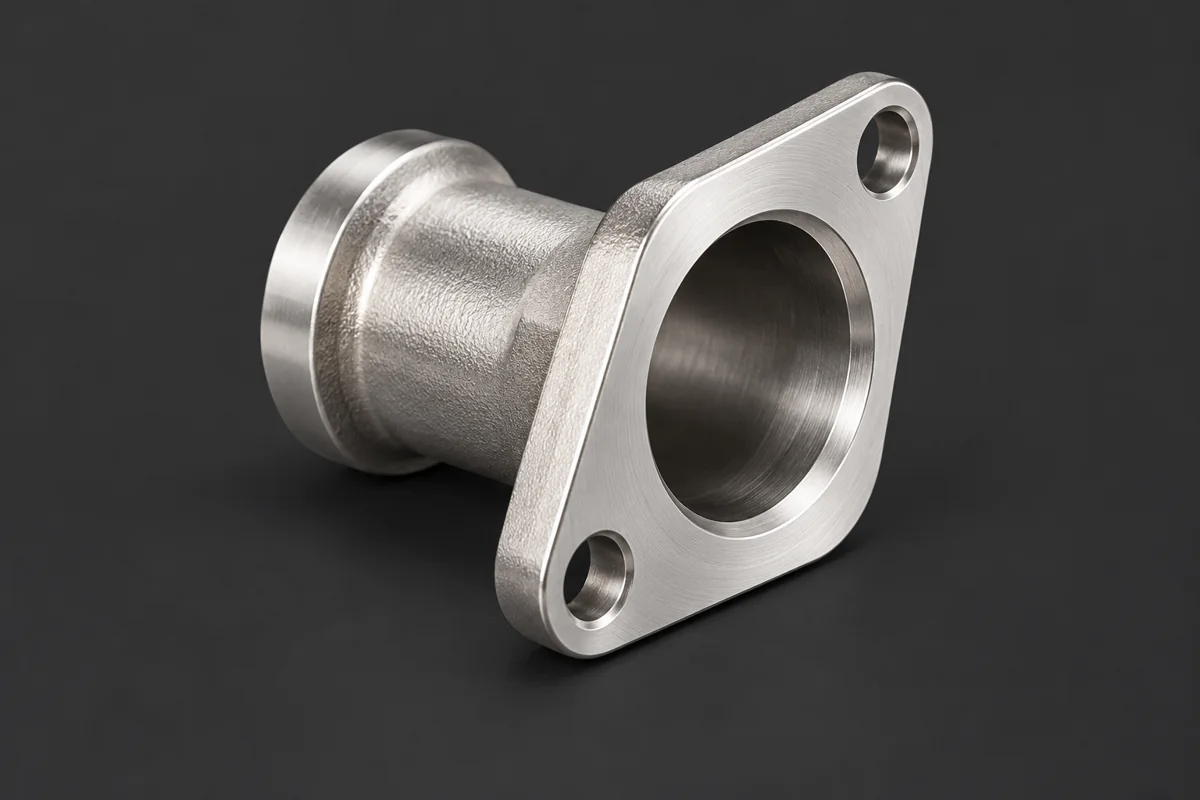
A sealing interface needs a defined geometry, not just a smooth-looking surface. State the thread system, seating contact, relevant face or axis relationships and measured roughness requirements where applicable. Each requirement should identify its location so machining and inspection address the same functional surface.
Leak Testing Uses an Agreed Method
A meaningful leak-test requirement identifies the object, method, medium, conditions and acceptance limit. Agree how openings are closed and whether the check follows final machining and cleaning. We review the specified method for the actual part; no pressure class or universal test condition is inferred from a flange photograph.
Inspection Records Describe the Delivered Condition
An inspection record is useful when it identifies the delivered body and the condition in which it was checked. Connect the drawing revision, batch reference, selected features and any specified test to the same order. Separate material evidence, dimensional results and body-test results instead of treating them as interchangeable certificates.
Detailed drawing and acceptance checklist
A Valve-Body RFQ Separates Included and Excluded Work
Your enquiry should show the body drawing, flow sections, material specification, machined contacts and included hardware. Add the sample quantity, repeat demand and any cleaning or test requirement. This lets you compare the full body supply scope and see which assembly responsibilities remain with your team.
Related engineering and purchasing guidance
Discuss Your Valve-Body Drawing
Share your valve-body drawing and fluid conditions with us. Mark threads, seats, sealing faces and the required test boundary, then include quantity and delivery needs. We can review the component scope before you commit to tooling or samples.
- [email protected]
- Phone
- +86 185 6176 2631
- +1 404 203 0971
- Project enquiry
- Contact our Qingdao team