
01 / 10 · Casting blanks for your machine shop
Core Location and Bore Stock in Sand-Cast Housing Blanks
Before you buy housing blanks, define where the cast cavity sits inside the finished bore. Enough material on one side does not compensate for missing stock on the other.
Outside casting envelope
Core-made internal cavity
Finished bore and its location
Relia reviews these references together so your incoming blank acceptance can support the machining plan.
Review your housing stock requirements02 / 10 · Buyer and foundry agreement
An As-Cast Cavity That Supports Your Machining Plan
Relia connects the proposed sand-cast blank to the finished component drawing. Your machining team identifies its locating method and required stock; the casting proposal defines the cavity, external references and agreed blank condition.
- DRAWINGOverlay cast and finished sectionsShow what is removed and what remains.
- PROCESSLocate the core and blankConnect internal and external references.
- ACCEPTANCECheck before machiningAgree the accessible points and required records.
03 / 10 · Section definition
The Cast Cavity Inside the Finished Envelope
Provide a section showing the cast internal surface and the final machined bore. Add the bore position relative to the finished mounting references.
In sand casting, a core can create an internal cavity that is not defined by the exterior mold alone. Its position affects the local stock available when the blank is machined.
Define the complete casting-blank delivery condition04 / 10 · Core support in the mold
Core Seating and Location References
Review the regions that locate and support the proposed core. The relevant references depend on the housing geometry and molding arrangement.
Location schematic only · no dimension or tolerance is implied
- Core seating
- Show locating regions in the mold and their relationship to the cavity.
- Casting reference
- Connect that cavity to accessible external features on the blank.
- Machining reference
- Locate the first operation from an agreed cast feature or prepared surface.
Check the local stock around the required bore axis. A cavity diameter alone cannot describe its location inside the blank.
Record the relationship rather than only a cavity diameter
A diameter check alone does not establish where the cavity sits inside the blank. Agree the positional references and section locations needed to evaluate local machining stock.
05 / 10 · Local material
Local Stock Around the Bore
State the stock requirement where it matters, including thin walls, nearby openings and transitions into ribs or bosses. Use section locations that both teams can identify.
A general machining allowance is useful only when the casting position and the intended finished geometry are also known. Set the actual limits against your part, material and machining sequence.
06 / 10 · Machining preparation
First-Operation Fixturing and Inspection Access
Agree how the housing is held before its final datums exist. The chosen cast pads or accessible surfaces should support both setup and the agreed stock checks.
Locate the blank
Identify the contacts used for the first machining operation and any preparation needed.
Reach the characteristic
Confirm access for the selected check, especially beside recesses and neighboring openings.
07 / 10 · Incoming inspection
Incoming Blank Acceptance Before Machining
Agree the required casting checks before your machine shop commits to cutting. The record should identify the component, drawing revision, measured locations and supplied condition.
Relia can provide agreed key dimensional records. Set the characteristics and sampling frequency per order, with any additional inspection method stated explicitly.
Keep an accepted blank reference or approved first-off record with the machining setup information so both teams use the same basis.
08 / 10 · Catalogue connections
Housing Geometry and Related Component References
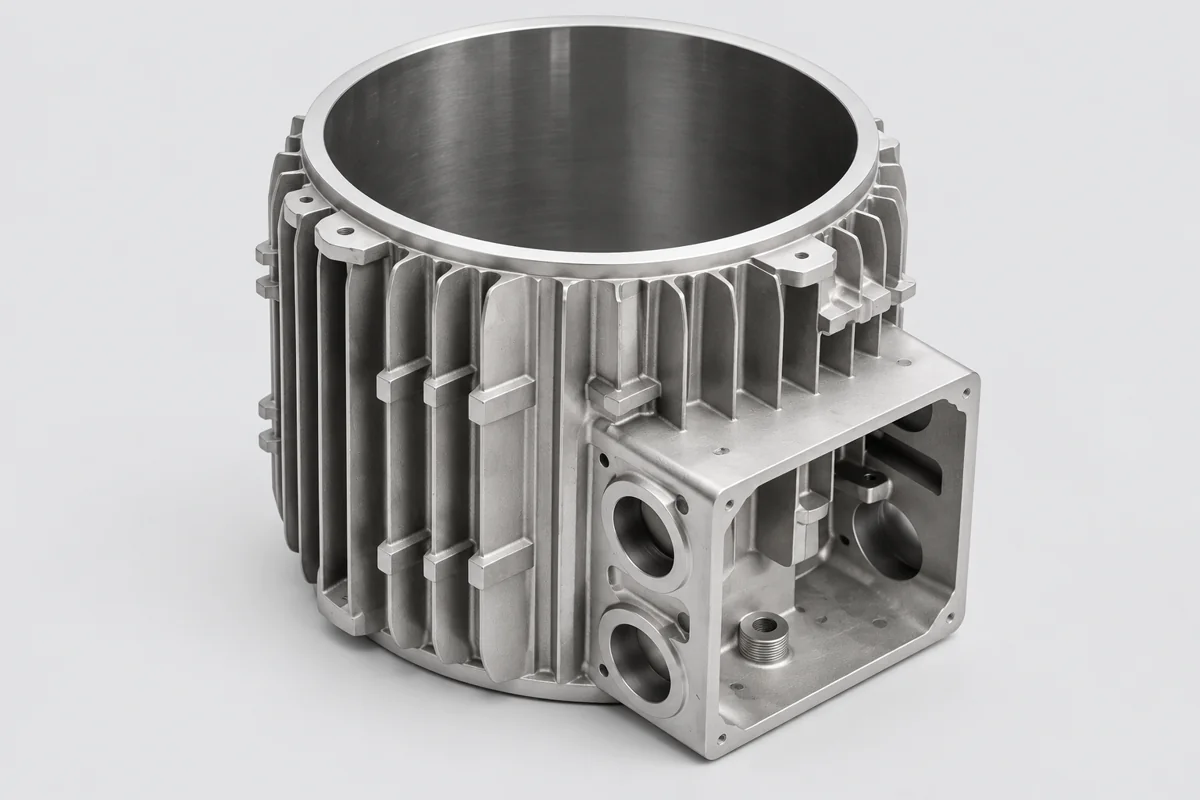
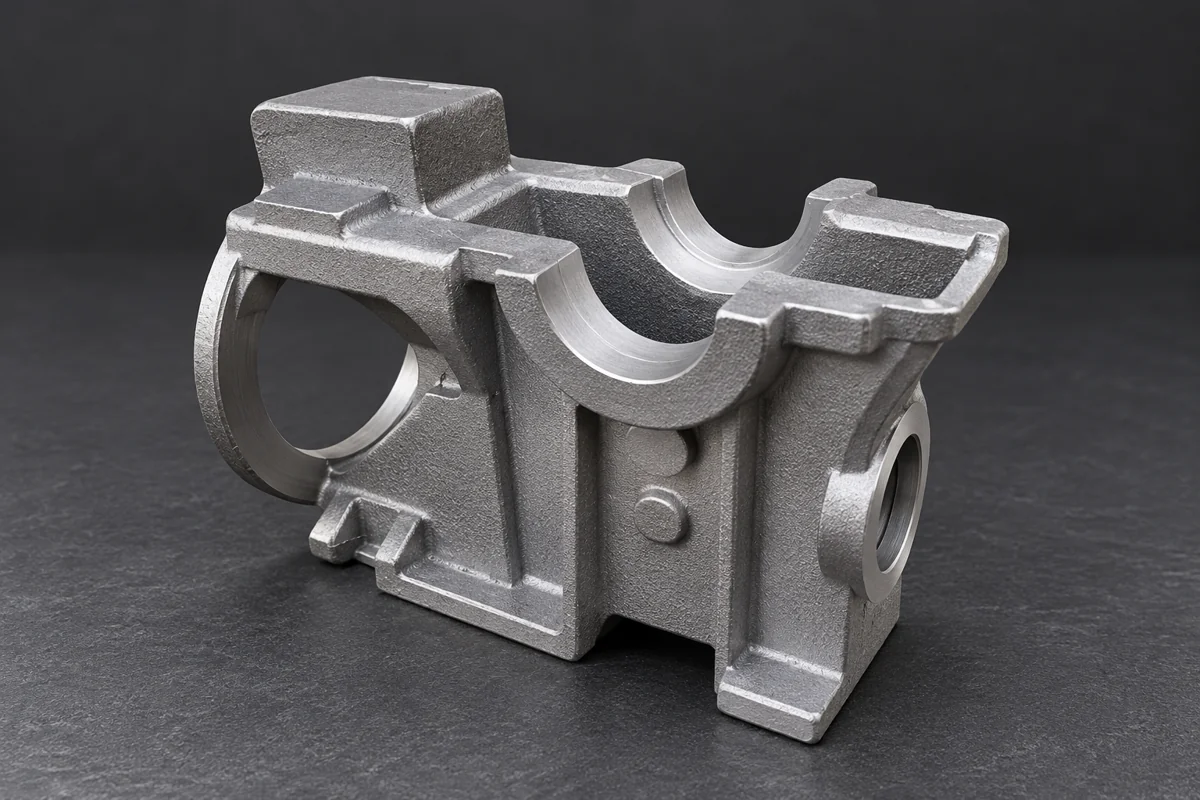
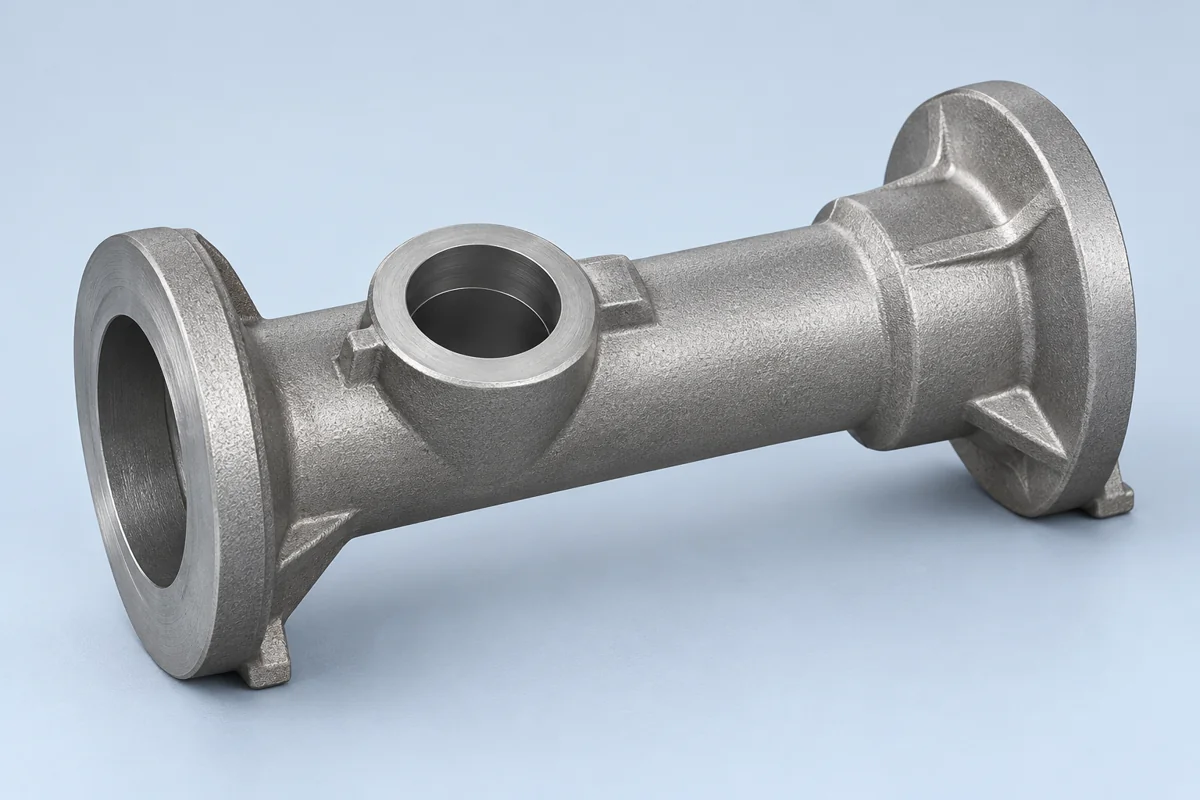
Open cylindrical housings, recessed bodies and asymmetric covers present different access and stock questions. Select the actual component drawing before agreeing the core and machining proposal.
View housing and industrial resin-sand casting enquiriesView circular housing and open-frame casting enquiriesView covers, bearing supports and ported casting forms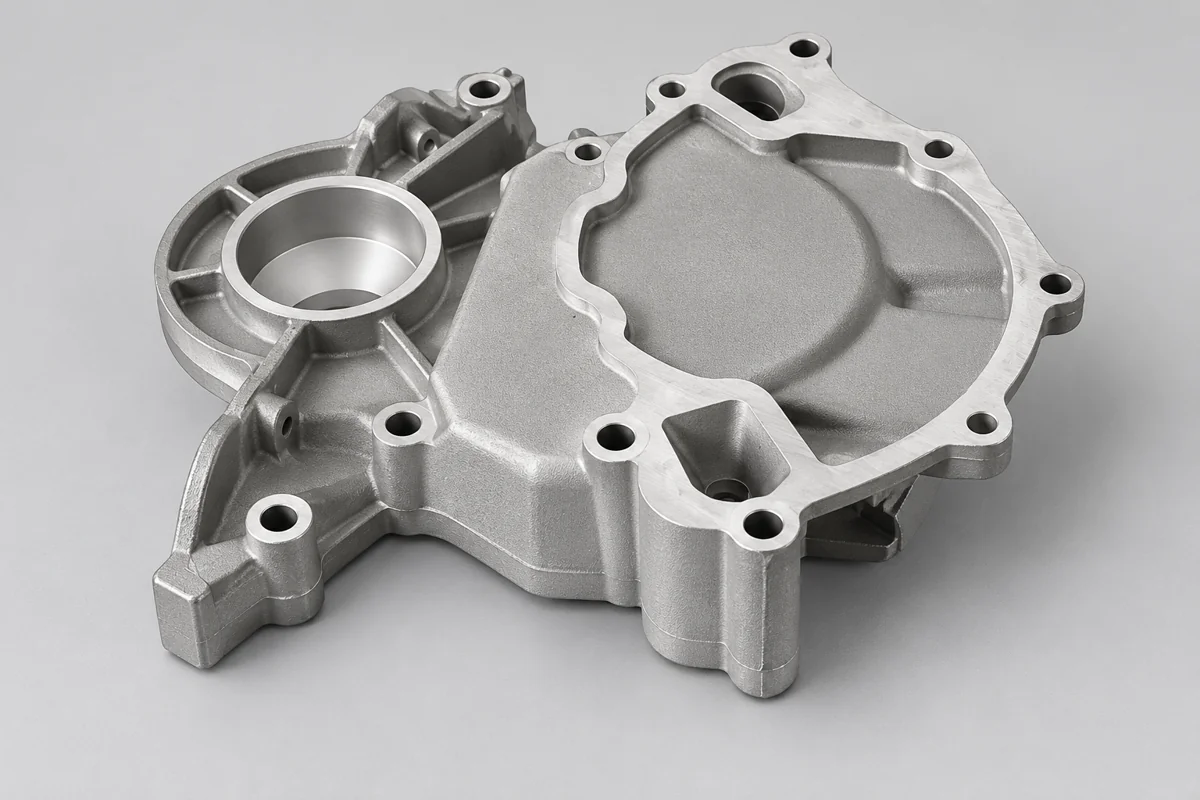
09 / 10 · Production release
Resolve Stock Exceptions Before Batch Release
Record the blank, section and measured observation.
Assess the effect with the agreed machining references.
Agree the next action before the affected batch proceeds.
Sample approval connects the casting proposal to the intended machining result. Changes to the core, locating method or finished drawing should return to that shared reference.
10 / 10 · Send the machining brief
Share Cast and Finished Housing Sections
Send Relia the finished drawing, proposed blank sections, material and quantities. Include your first-operation locating method and the local stock you need checked before machining.
Email the housing sections- [email protected]
- Phone
- +86 185 6176 2631
- +1 404 203 0971
- Company and address
- Relia Casting
No. 96 Shuyuan Road
Qingdao, Shandong, China