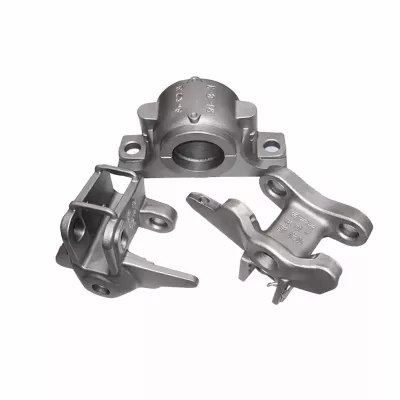
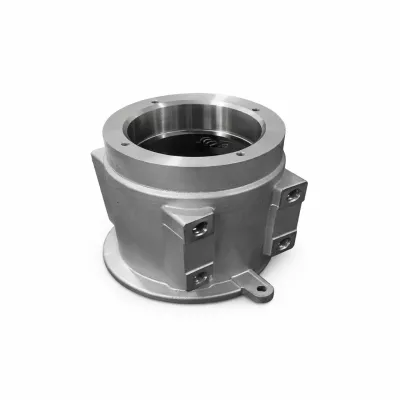
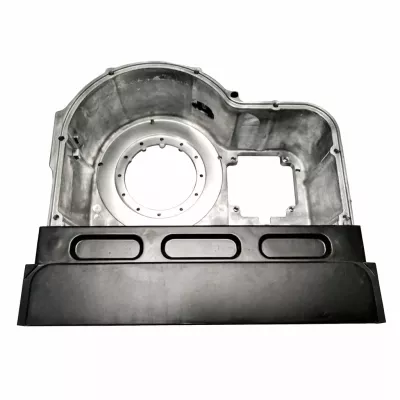
-
Model NumberDie castingMaterialAluminum
-
ApplicationIndustryDimensionsCustomer Required
-
Surface treatmentPaint/Powder coating/oxidation etcMold makingBy ourself
-
ProcessDie Casting-deburring- MachineryServiceOEM ODM
-
FeatureEco FriendlyQuality ControlProfessional Inspection
-
PackingCarton
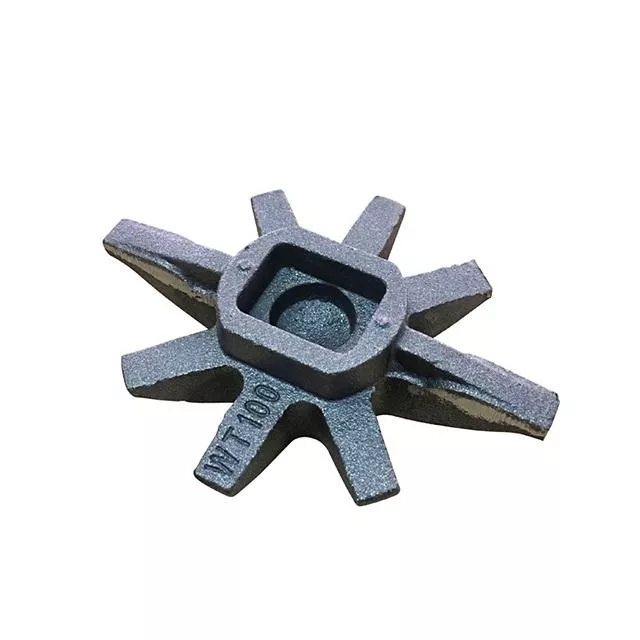
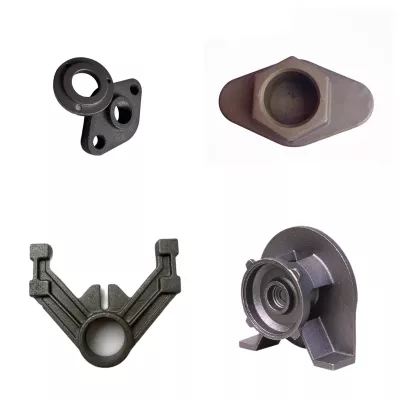
Use the actual radial geometry to define the custom casting request. The example is a dark star-like component with projecting arms and a raised roughly square central recess around a round region. Neither its color nor the visible lettering independently establishes the material grade, manufacturing route or operating purpose.
Describe the arms and central seat
Provide the outer envelope, arm arrangement and section thicknesses from a controlled drawing. Locate the central recess and round region relative to the casting's datum surfaces. Identify the faces or openings that engage adjoining parts and include their mating details where they control fit.
- Provide the radial-component drawing and its revision.
- Specify the actual grey-iron grade and material records.
- Dimension the arms, central recess and mating interfaces.
- Identify casting, machining and finishing requirements.
- Define final inspection and the intended application criteria.
Choose the material and route for the order
For a grey-iron sand-casting enquiry, identify that material and route explicitly. Aluminum and die-casting terms elsewhere in the service information are separate directions to review, not evidence that this grey-iron requirement should be produced from aluminum or follow every listed process.
Mark surfaces supplied as cast and those requiring secondary machining. State the actual dimensions, units, tolerances and inspection methods needed for the central seat and arm interfaces. A generic precision or inspection label does not define those requirements for the part.
Connect finishing to the supplied condition
Select paint, coating or another treatment appropriate to the chosen metal and installation. Identify contact areas needing masking or dimensional protection and state whether acceptance occurs before or after the selected finish. The photograph does not establish a coating process or a tested resistance property.
Provide the actual assembly role and any load, speed or other duty criteria relevant to selection. A radial form does not prove that the item is a rated rotating component. Confirm current quantities and the records needed with the supplied part. A clear enquiry connects one arm-and-seat geometry to its material, casting route and inspection plan, avoiding a combined specification assembled from unrelated catalogue fields.