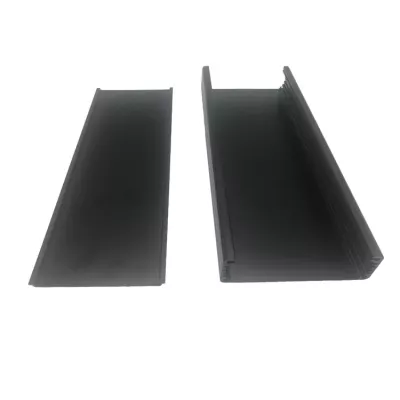
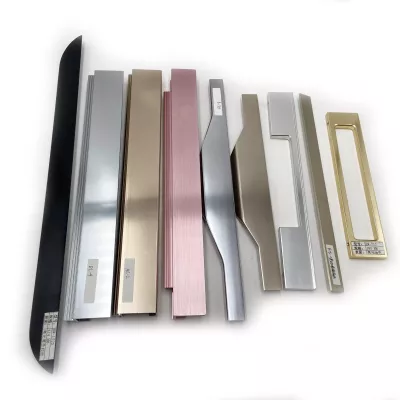
-
Grade6000 SeriesTemperT3-T8
-
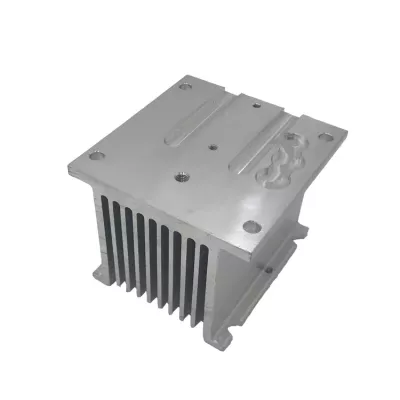
ApplicationHeat Sink, Industrial EquipmentShapeT - Profile
-
Alloy Or NotIs AlloyModel NumberDmetal-200034
-
Tolerance+-0.05mmProcessing ServiceCutting, extruding
-
Delivery Time22-30 daysProduct material6063 Aluminum
-
ColorBlack MetalSizeCustomized
-
Surface treatmentAnodized/oxide etc /powder coatedToolingMade by ourself
-
PackingCartonProcessSand casting +CNC Machining
-
CertificationISO9001-2008MachiningAvailable
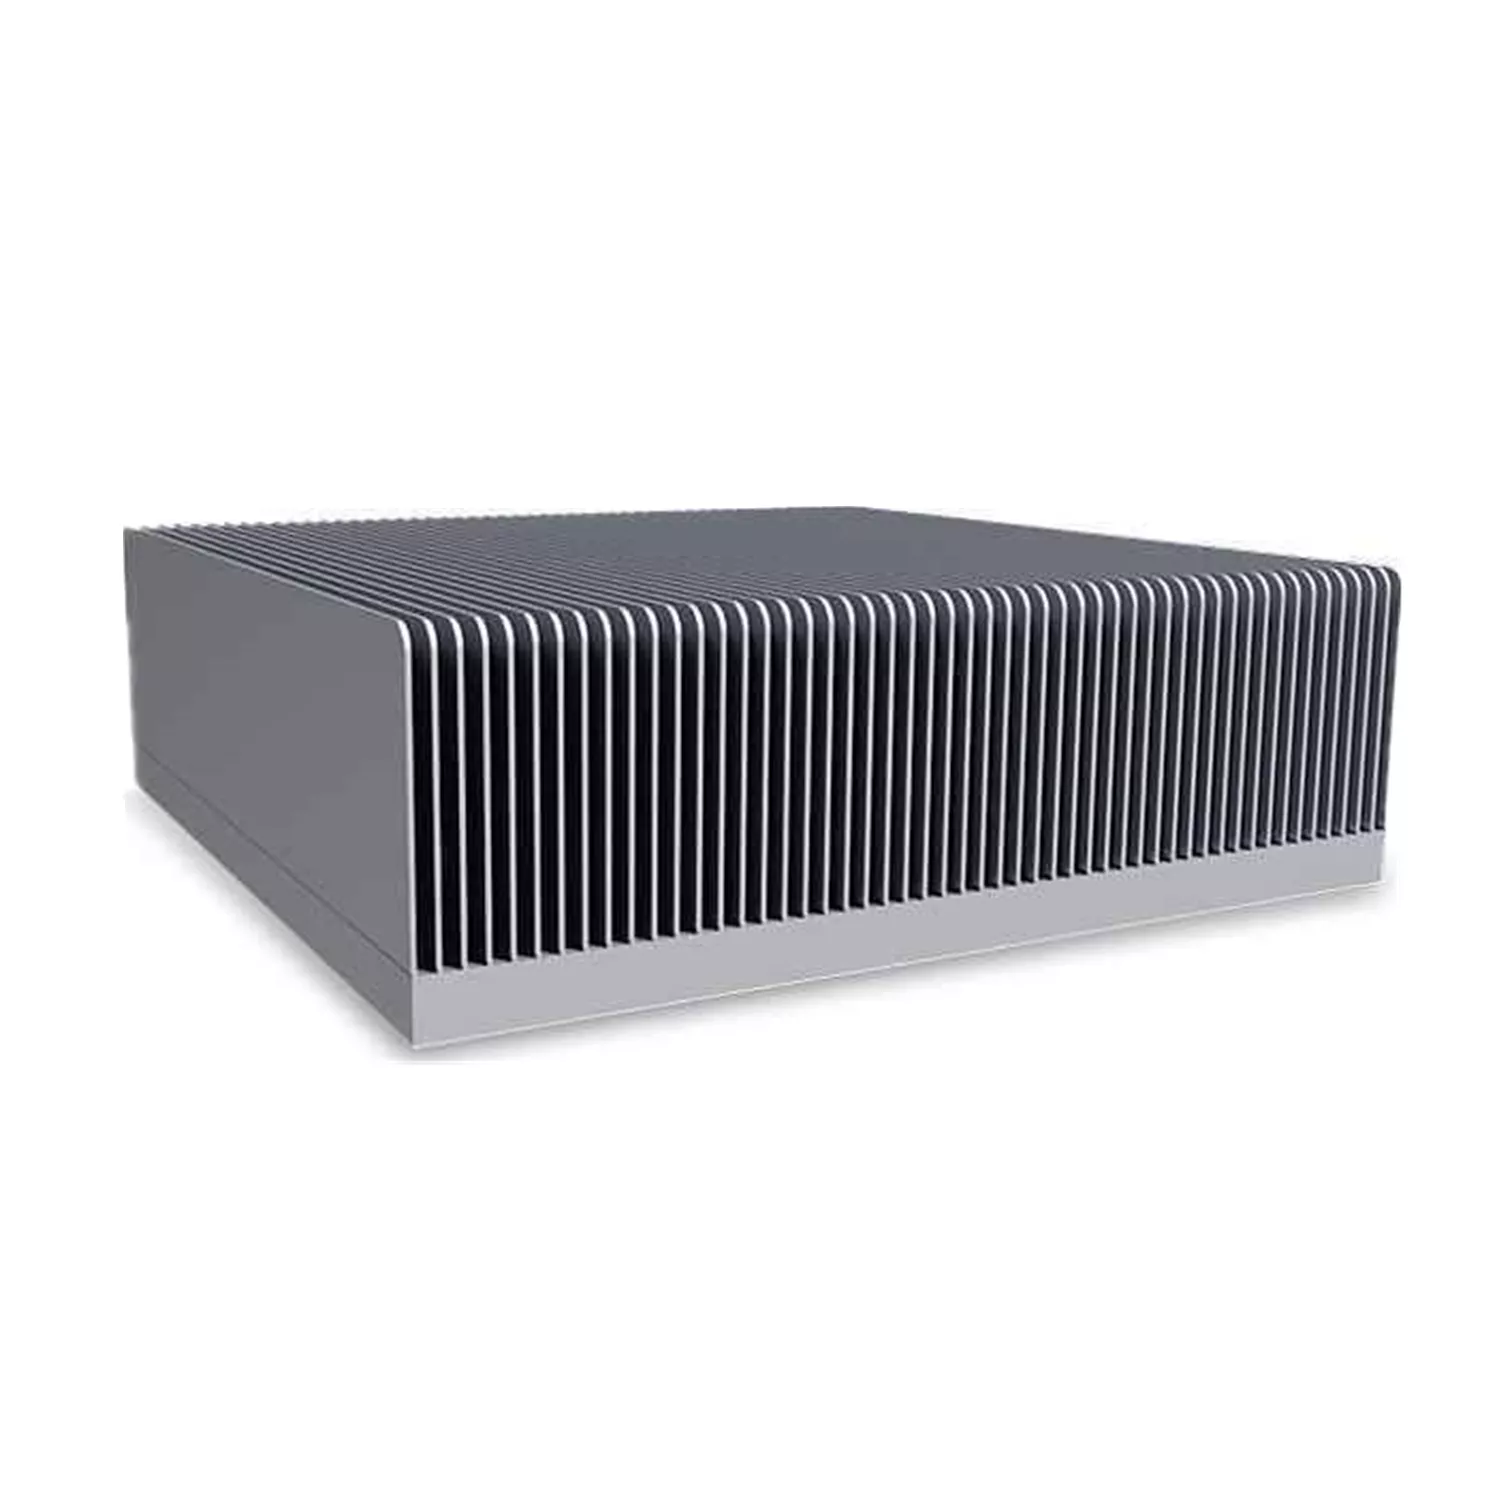
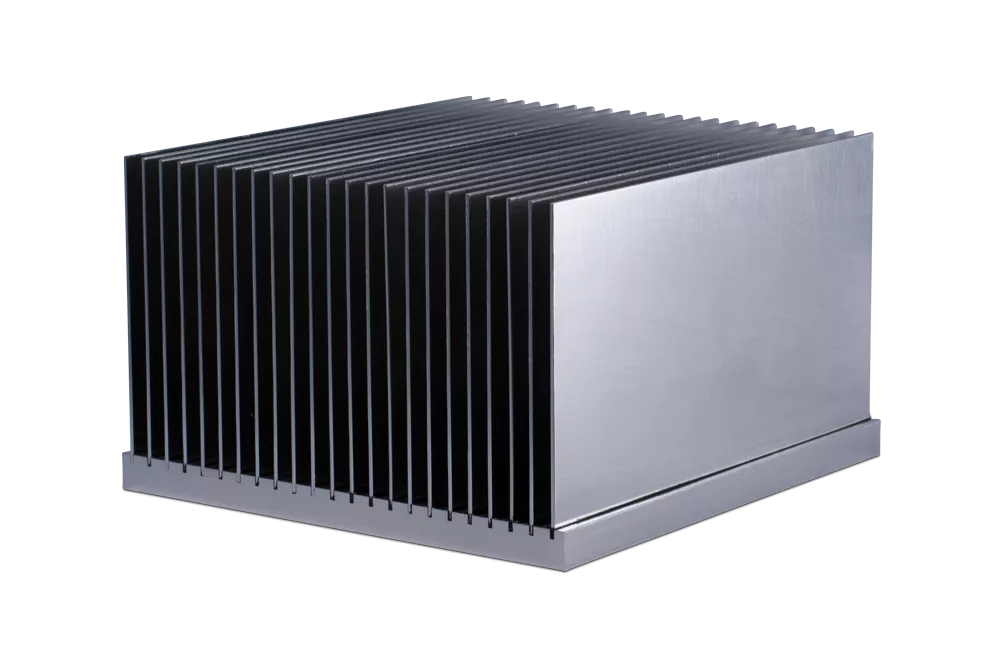
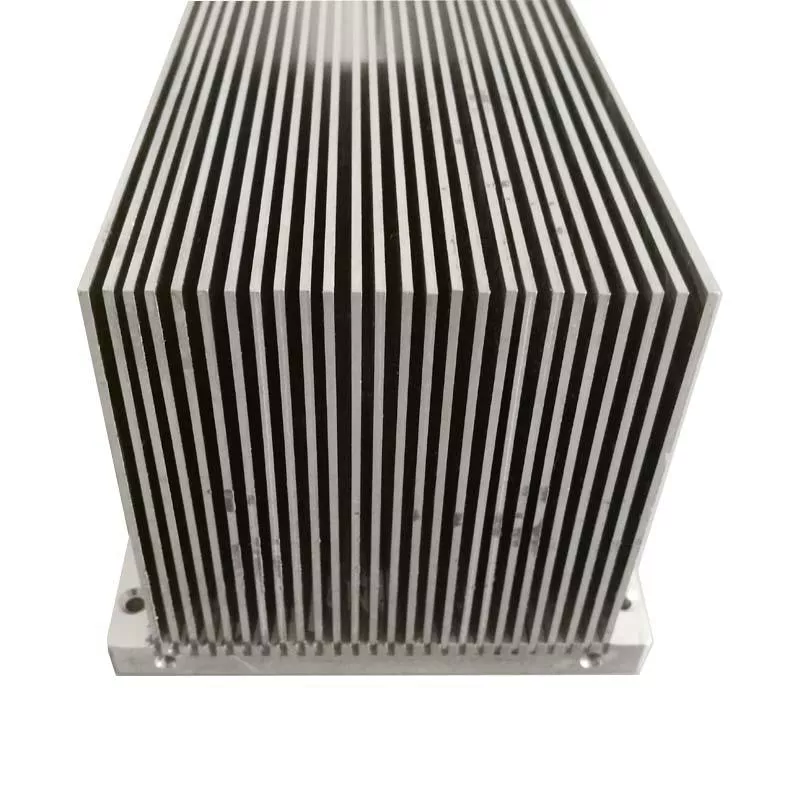
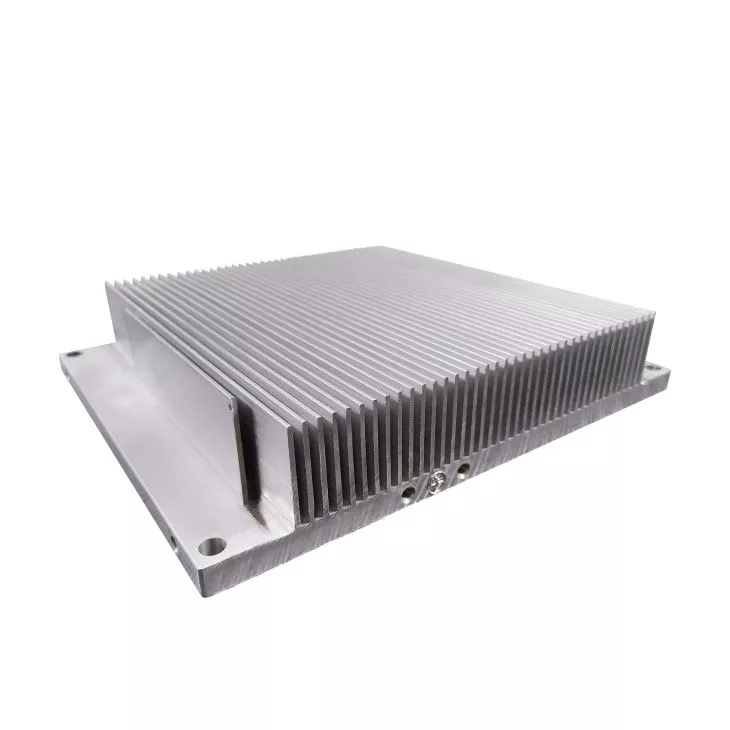
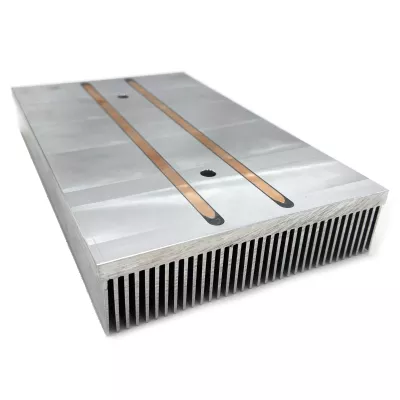
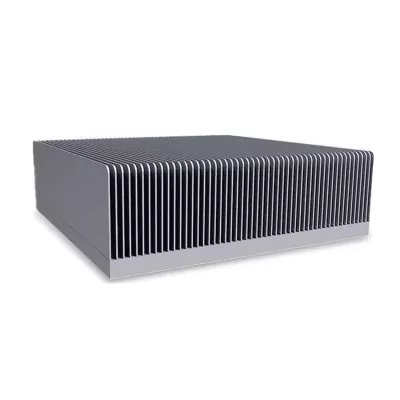
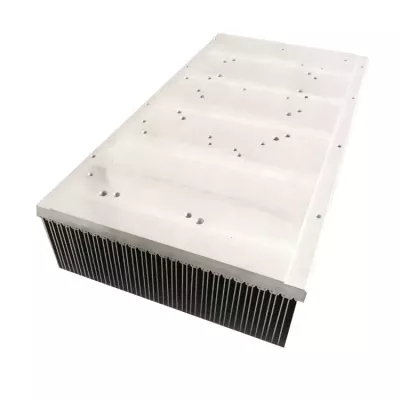
A skived or bonded-fin heat-sink enquiry should identify the construction required by the drawing. The example has a rectangular field of closely spaced thin plates with curved transitions at the visible fin ends. Appearance alone does not determine whether those fins are skived, bonded or made by another route.
Choose the fin construction to be reviewed
State whether the project requires skived fins, bonded fins or an alternative proposed construction. Identify the base and fin scope, including any joint or process acceptance required by the selected design. Different process names in a catalogue should not be combined into one assumed manufacturing sequence.
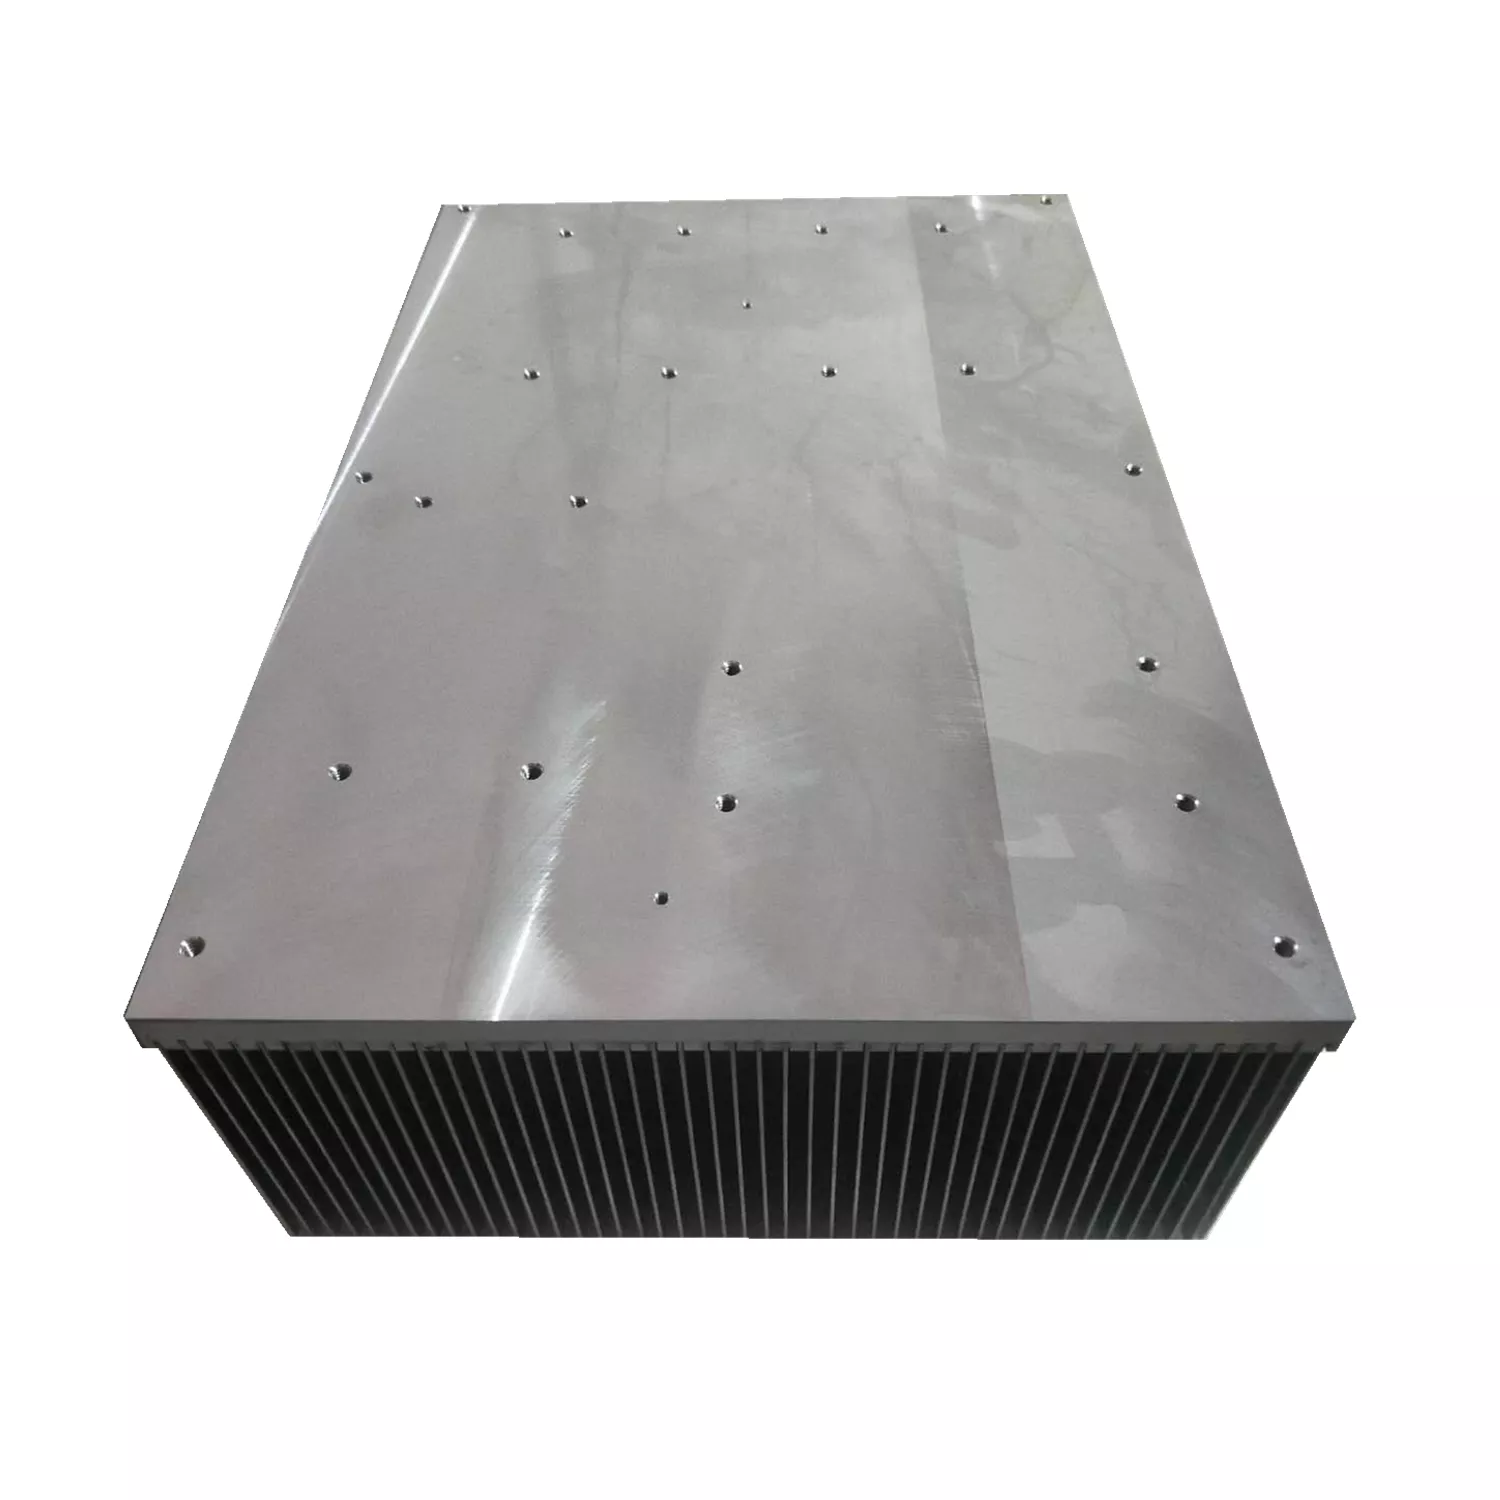
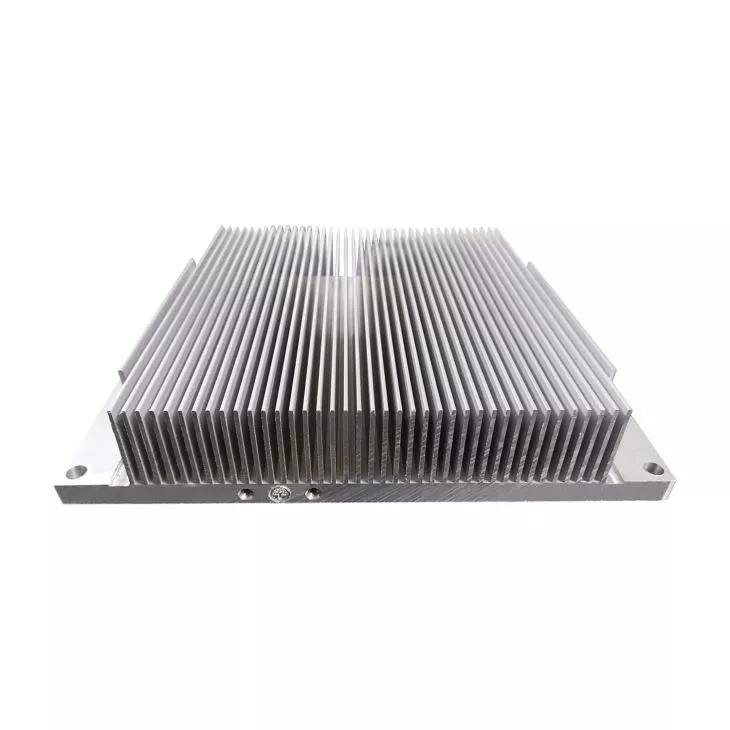
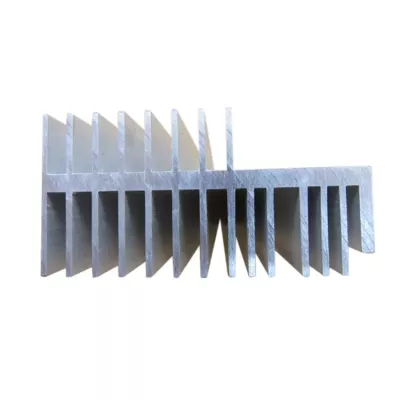
Provide the base dimensions and thermal contact face, with fin thickness, height and spacing where they matter to the design. Include the installation envelope, mounting arrangement and adjoining parts that limit access. The drawing should define the component independently of the example's appearance or a general T-profile field.
- Select the actual alloy condition, including 6063-T5 if required.
- Define the base and fin geometry on a controlled drawing.
- Identify the required construction and any joint acceptance.
- Mark secondary machining, masking and contact interfaces.
- State final-condition tolerances and inspection records.
Specify alloy, finish and critical dimensions
The broad temper range and ±0.05mm reference are starting information, not proof of the condition or tolerance of every sample. Assign dimensional requirements to the actual features and agree how they will be checked. Likewise, the historical sand-casting and CNC field does not require every thermal-profile enquiry to follow that route.
Link the fin design to its operating conditions
Supply the heat load, ambient conditions, airflow arrangement and thermal contact requirements for project-specific assessment. A dense plate array does not establish a measured cooling result or verified joint quality. Choose anodizing or another finish for the selected material and application, with contact-face requirements identified. Confirm current quantities, documentation and delivery arrangements for the order. A useful enquiry combines one construction choice with a defined drawing, supplied condition and acceptance plan.