Custom 6000 Series 6061 6063 Aluminum Extrusion Heatsink with CNC Machining Enquiries
-
Grade6000 SeriesTemperT3-T8
-
ApplicationHeat Sink, Industrial EquipmentShapeT - Profile
-
Alloy Or NotIs AlloyModel Number2201
-
Tolerance±1%Processing ServiceBending, Decoiling, Punching, Cutting
-
Delivery Time22-30 daysProduct material6063 Aluminum
-
ColorBlack MetalSizeCustomized
-
Surface treatmentAnodized/oxide etc /powder coatedToolingMade by ourself
-
PackingCartonProcessSand casting +CNC Machining
-
CertificationISO9001-2008MachiningAvailable
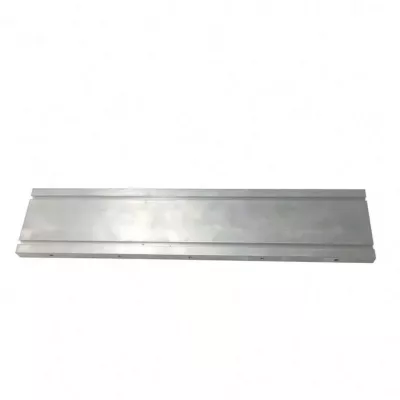
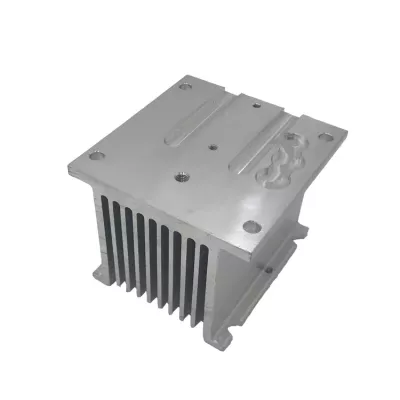
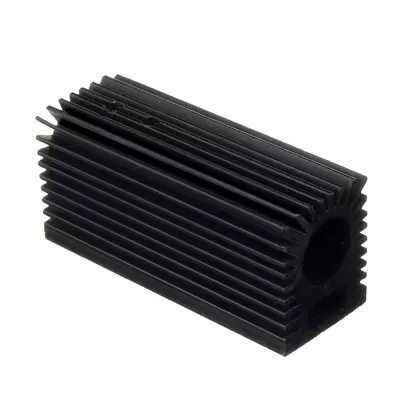
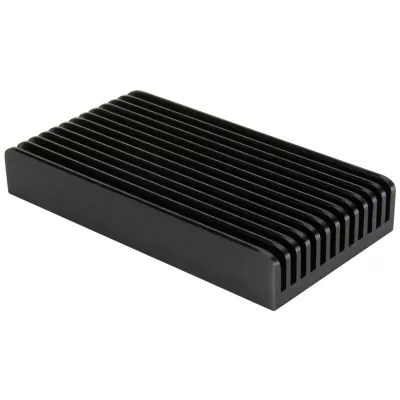
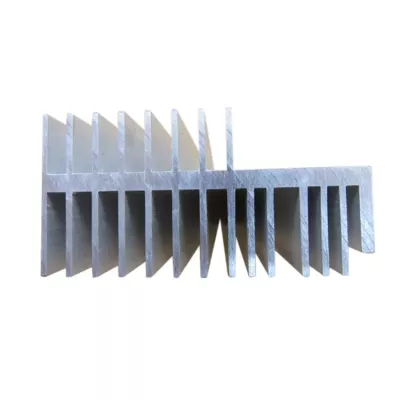
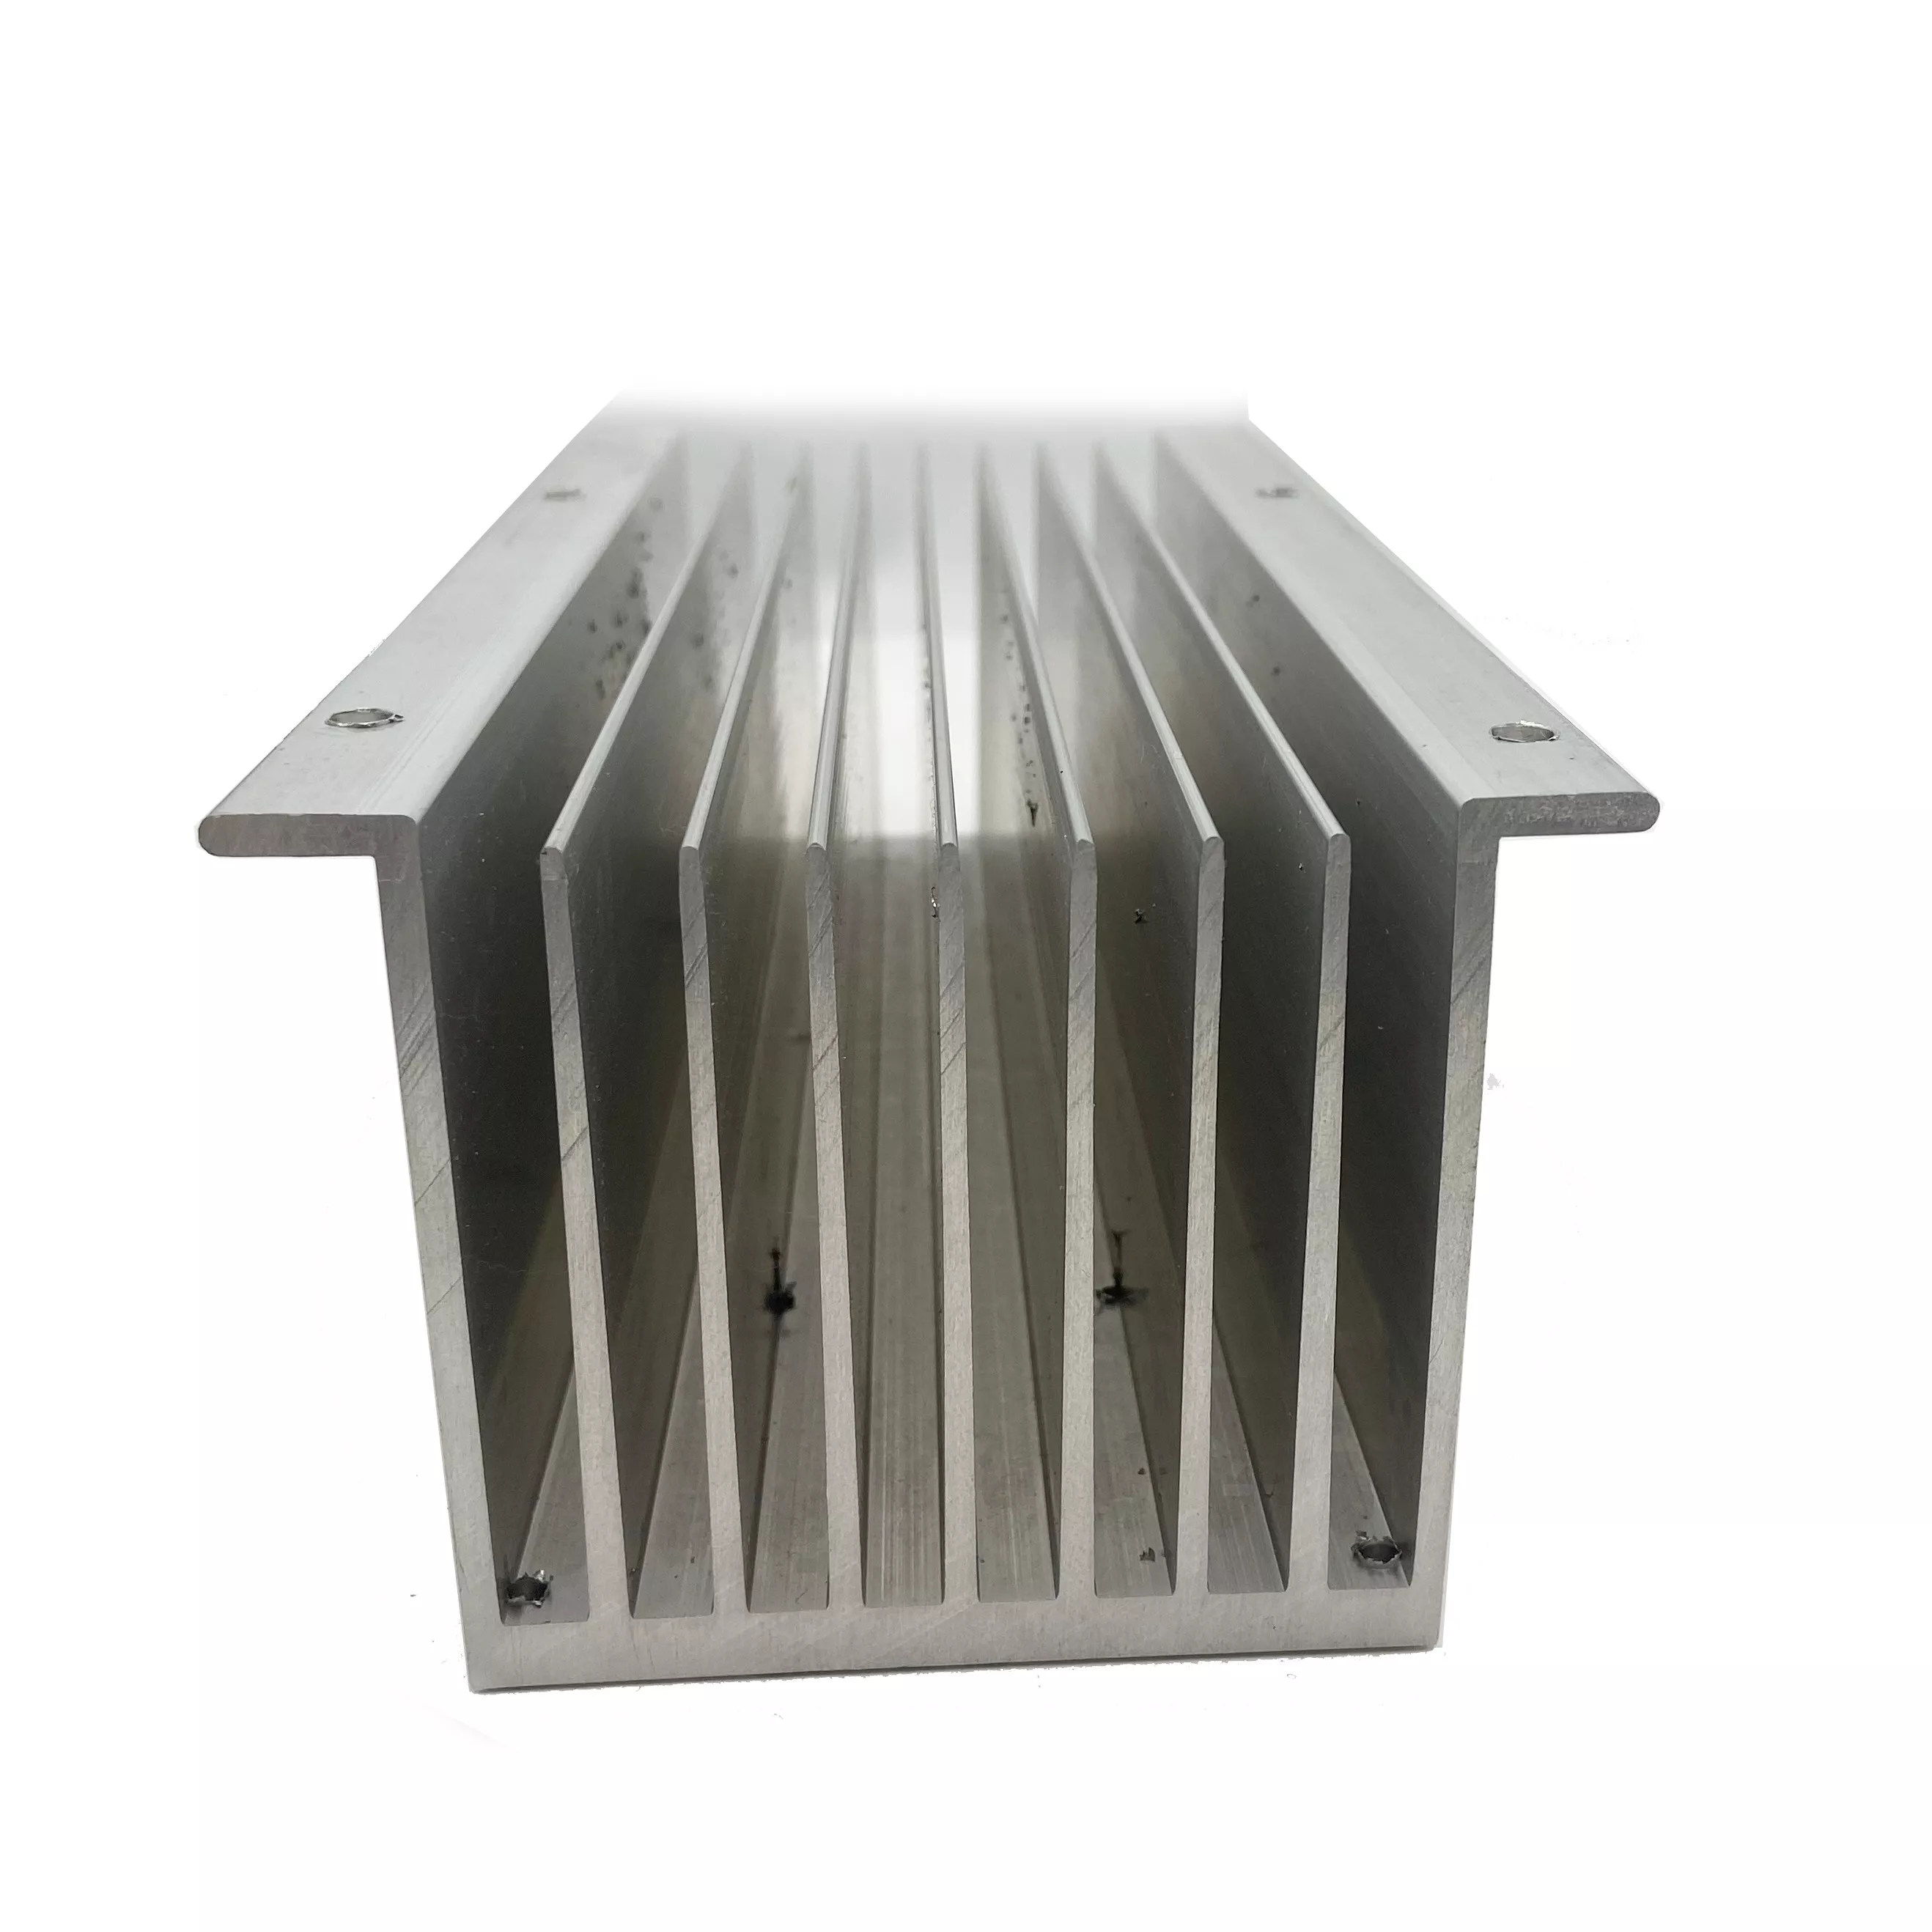
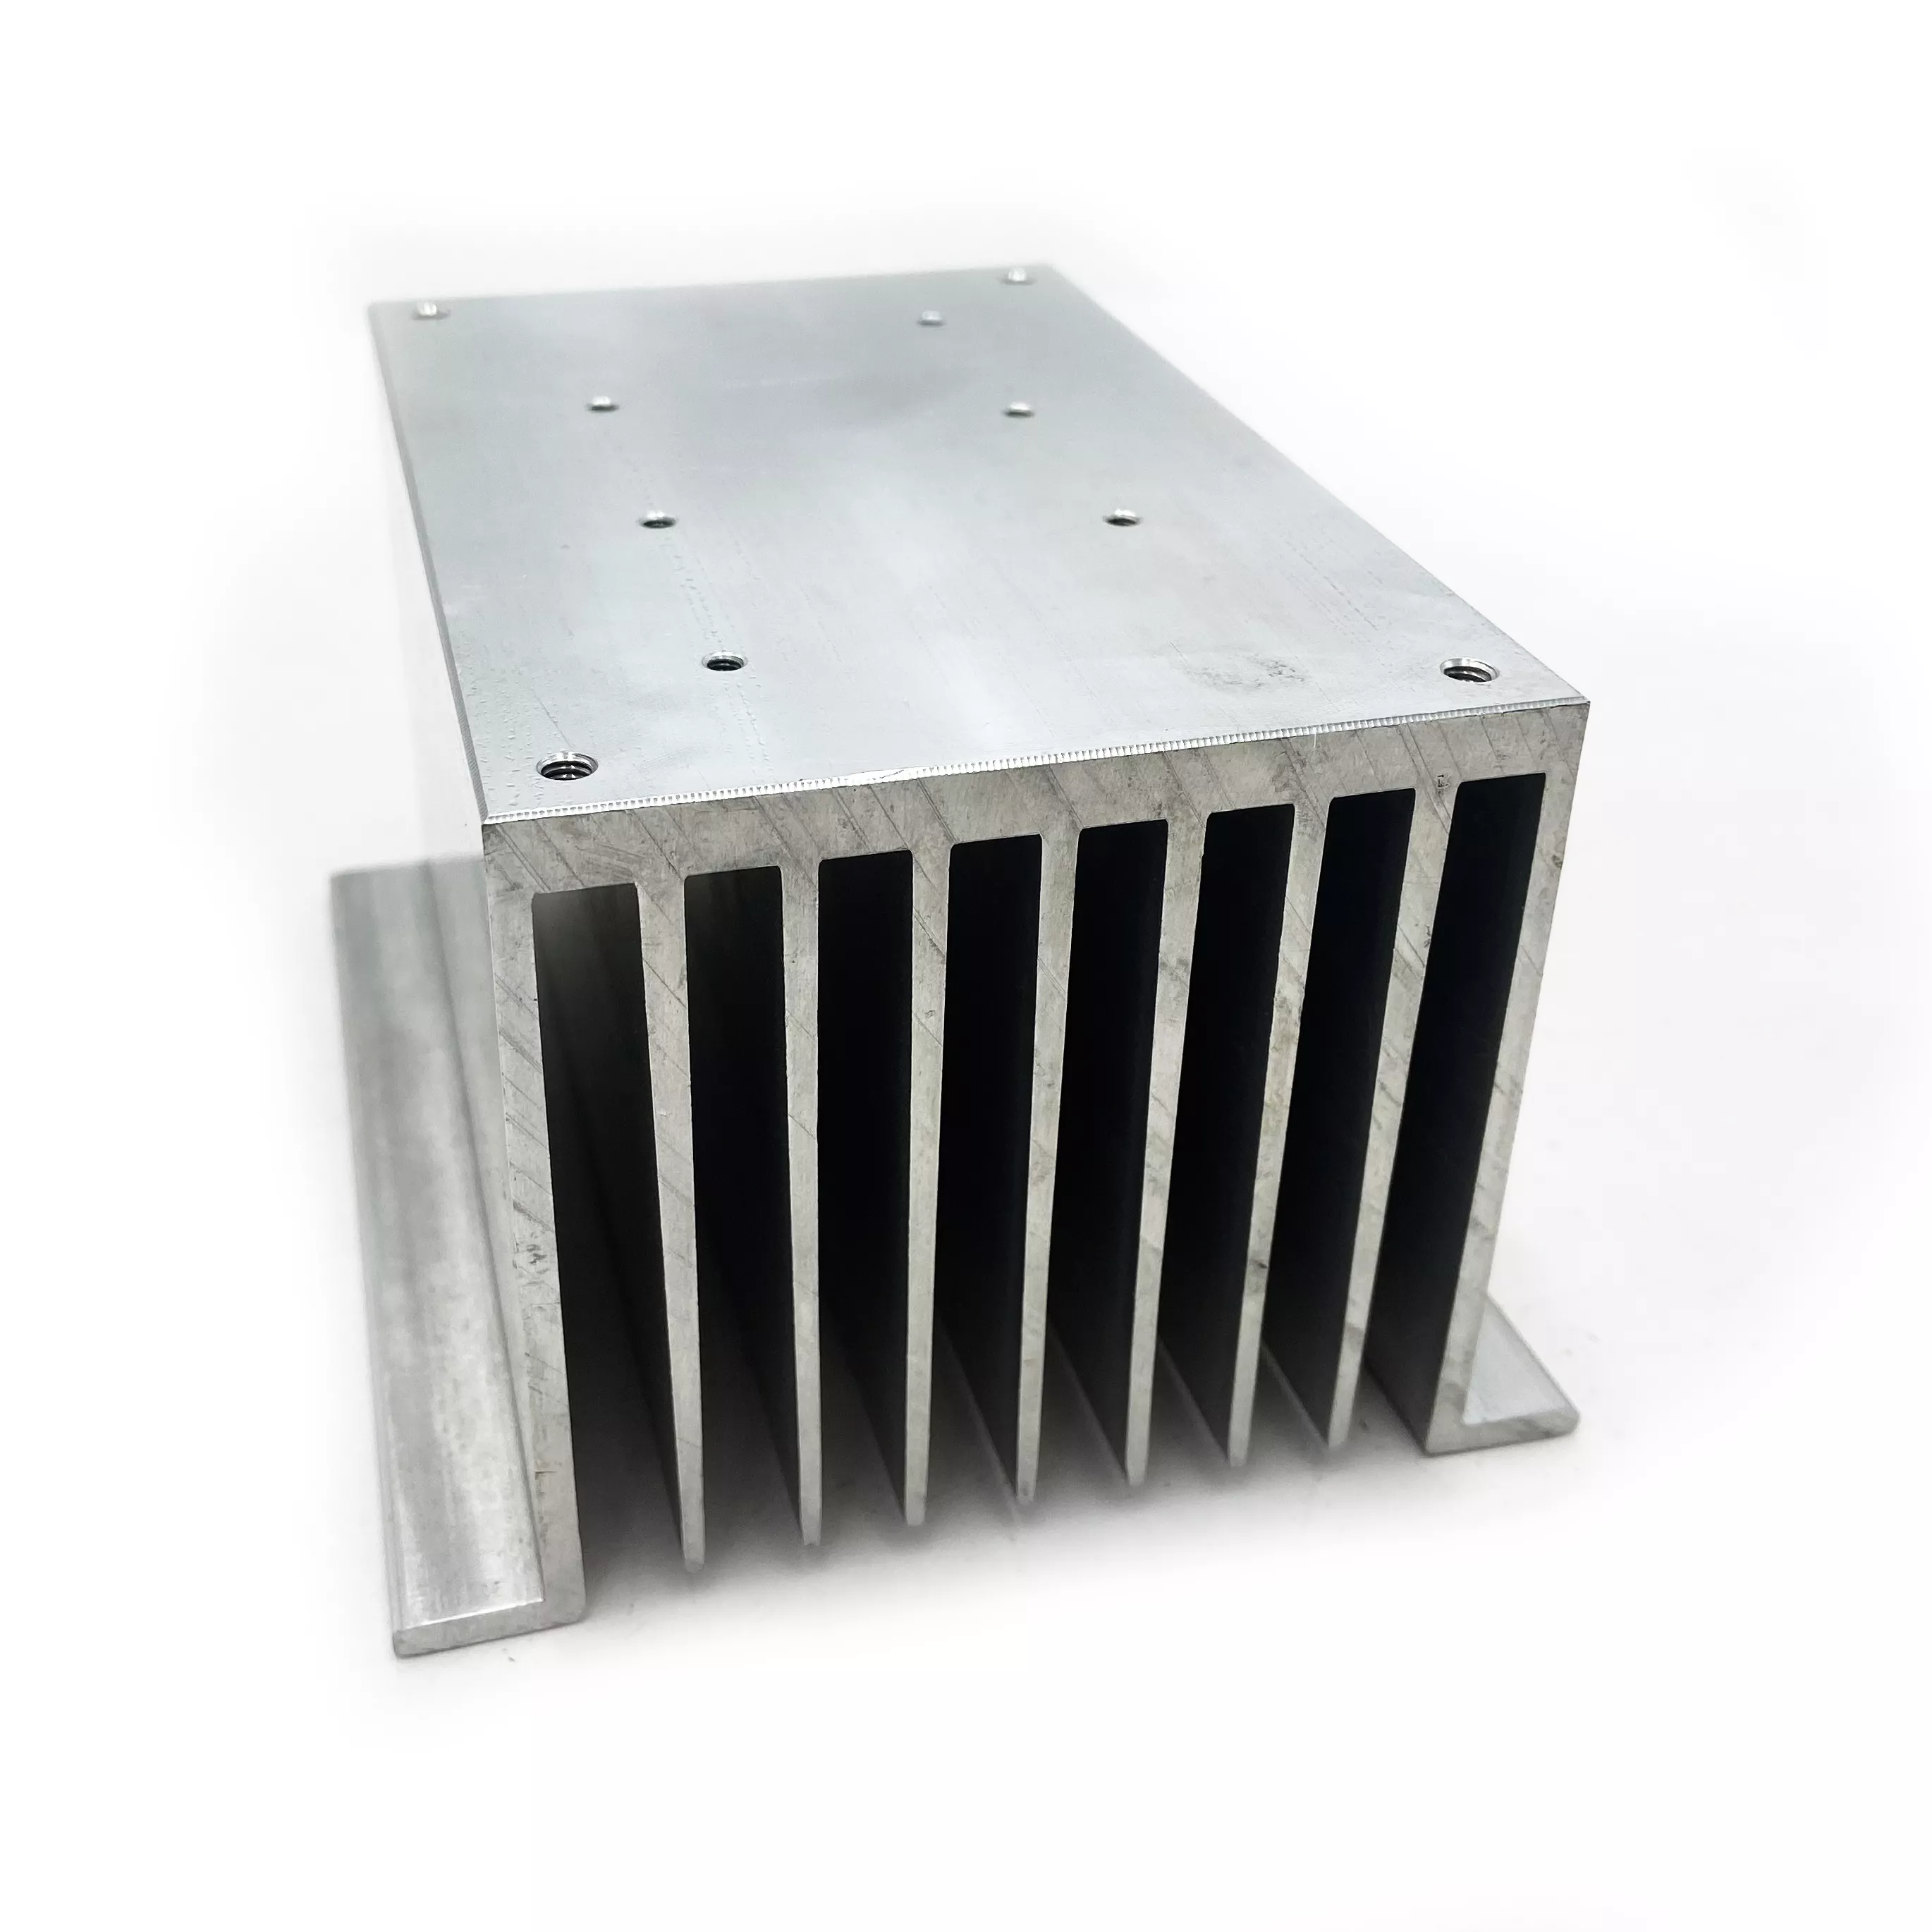
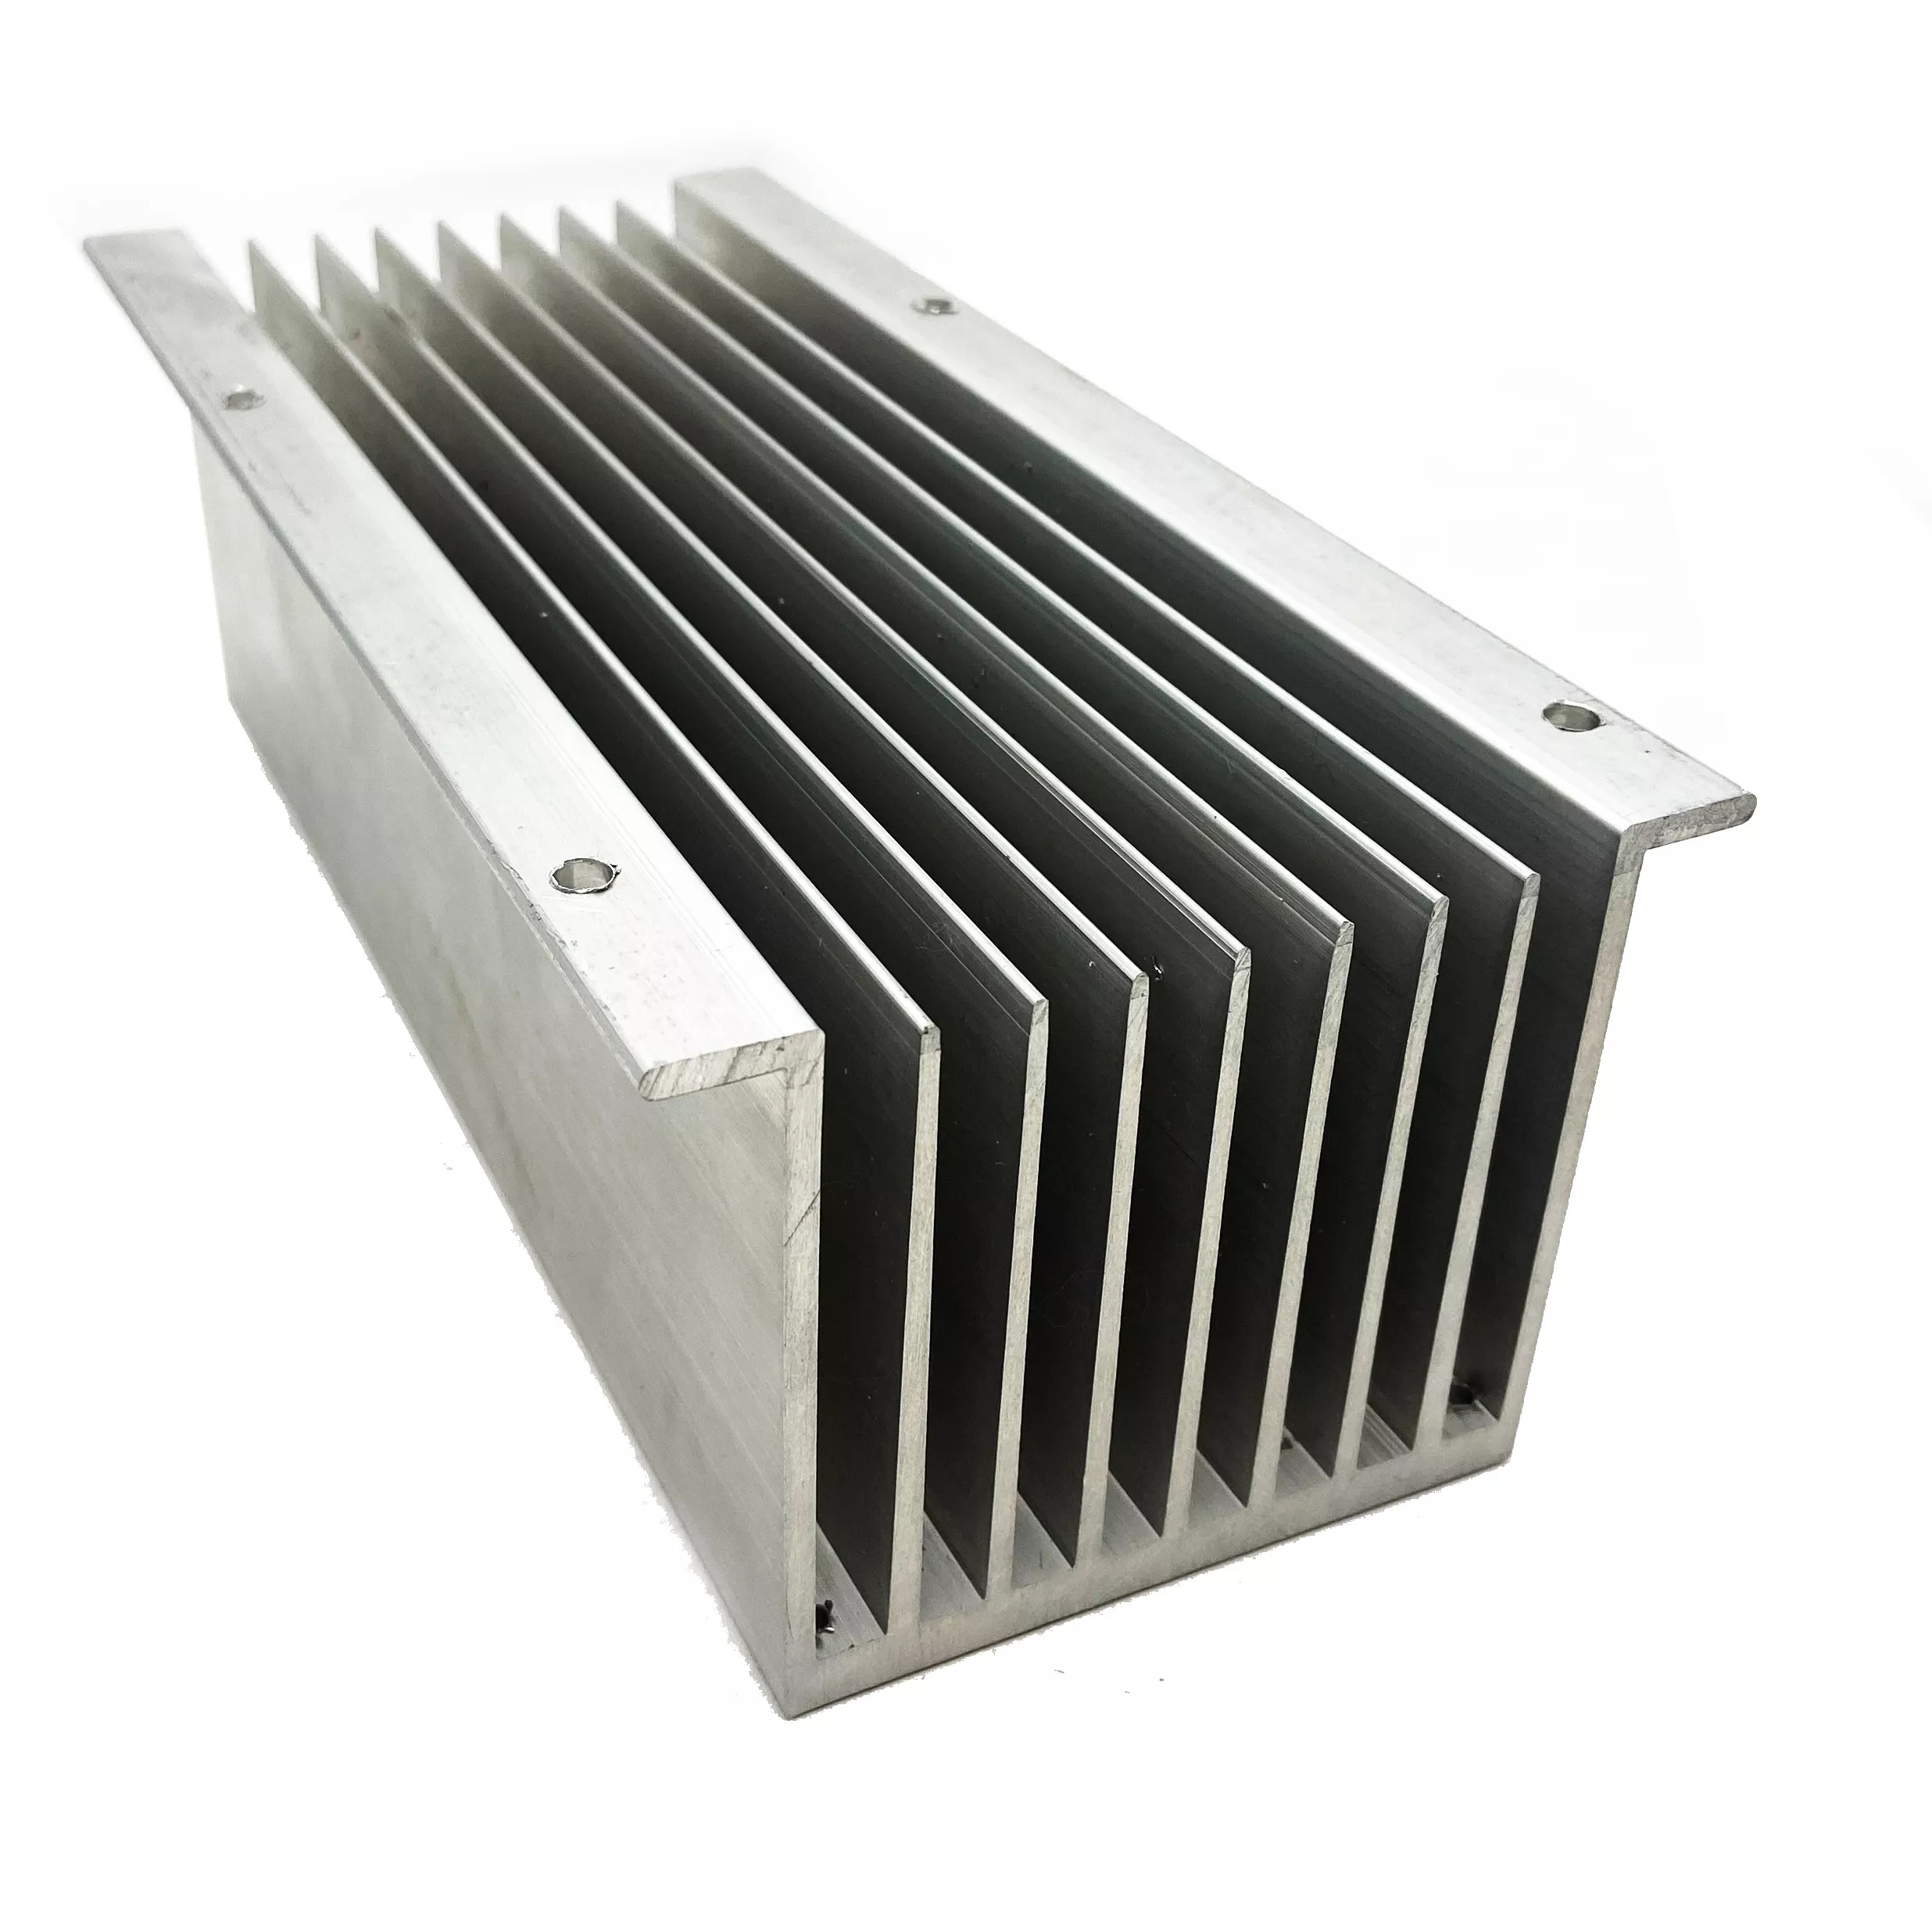
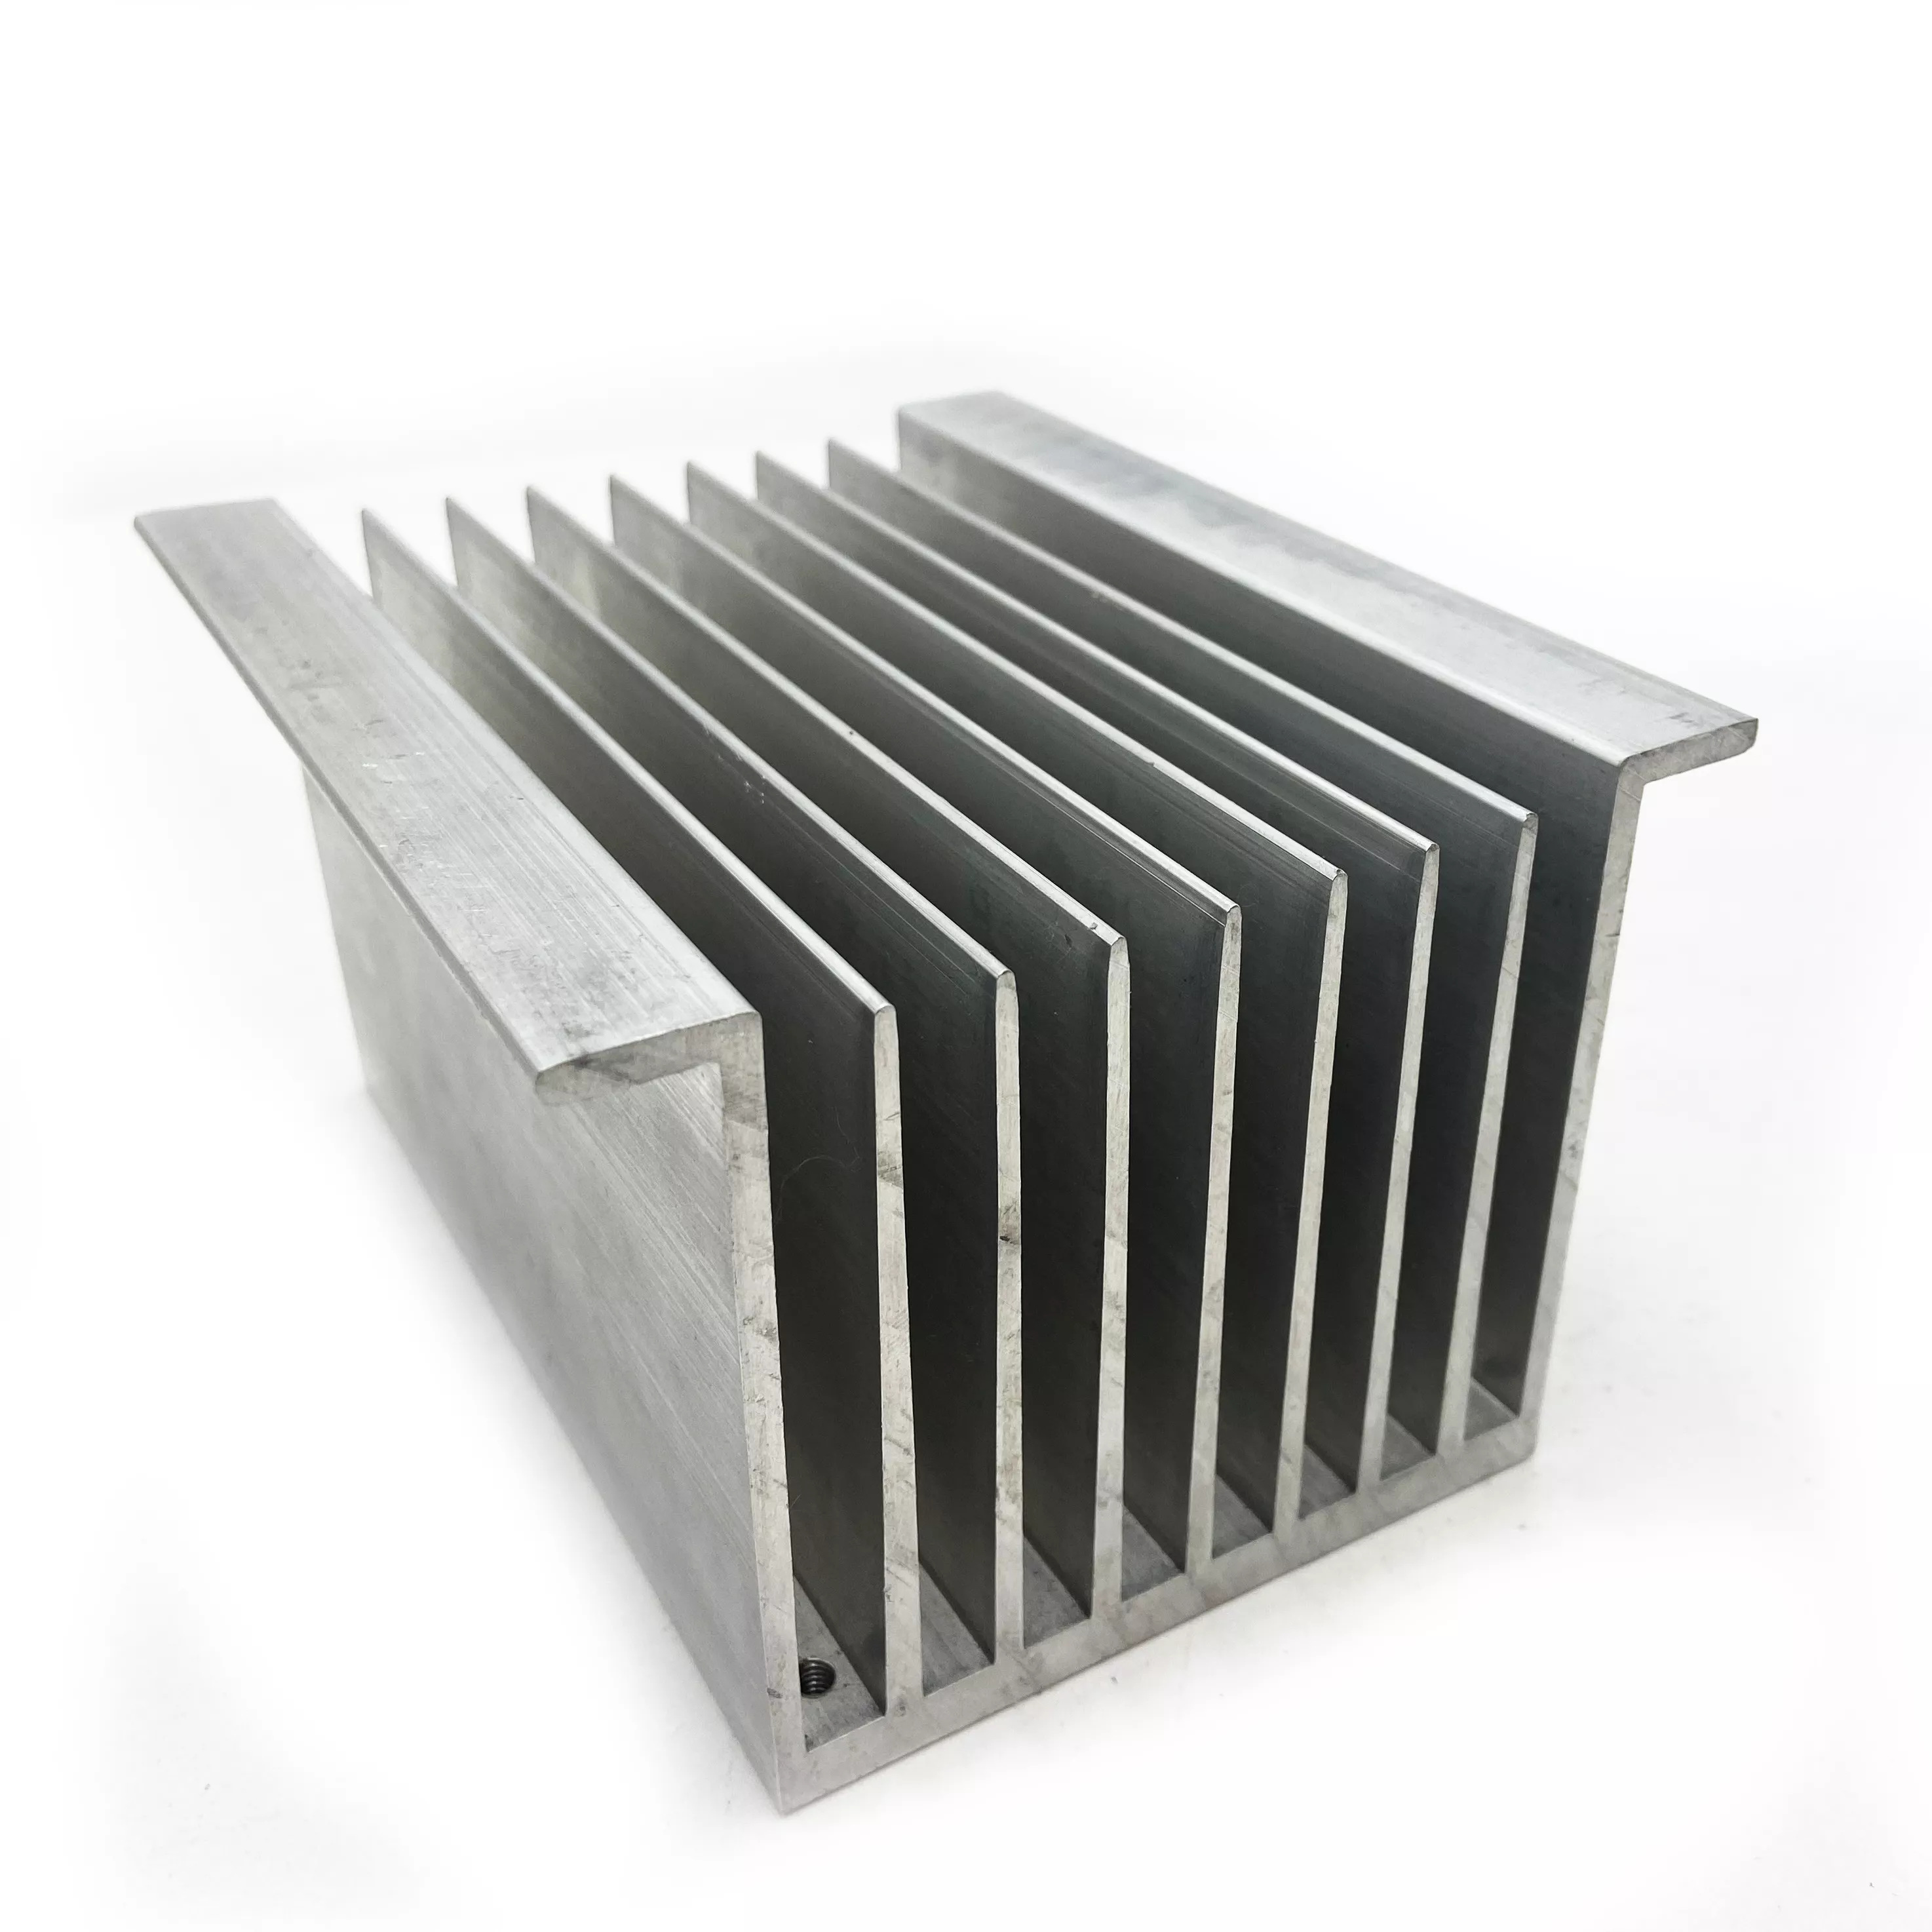
Select the actual aluminum alloy for the component before defining its machining scope. This enquiry names 6000-series material with 6061 and 6063 alternatives and CNC machining. The example has a deep channel-like section with thick outer walls, projecting upper lips and several thinner fins rising from the inner base.
Dimension the channel and mating lips
Provide the cross-section and cut length, locating the walls, base, lips and internal fin field from the assembly references. Identify any adjoining part that engages the lips or constrains the inner channel. Include the installation envelope and the clearances required around the fins.
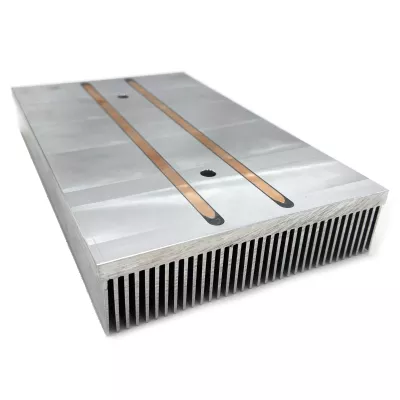
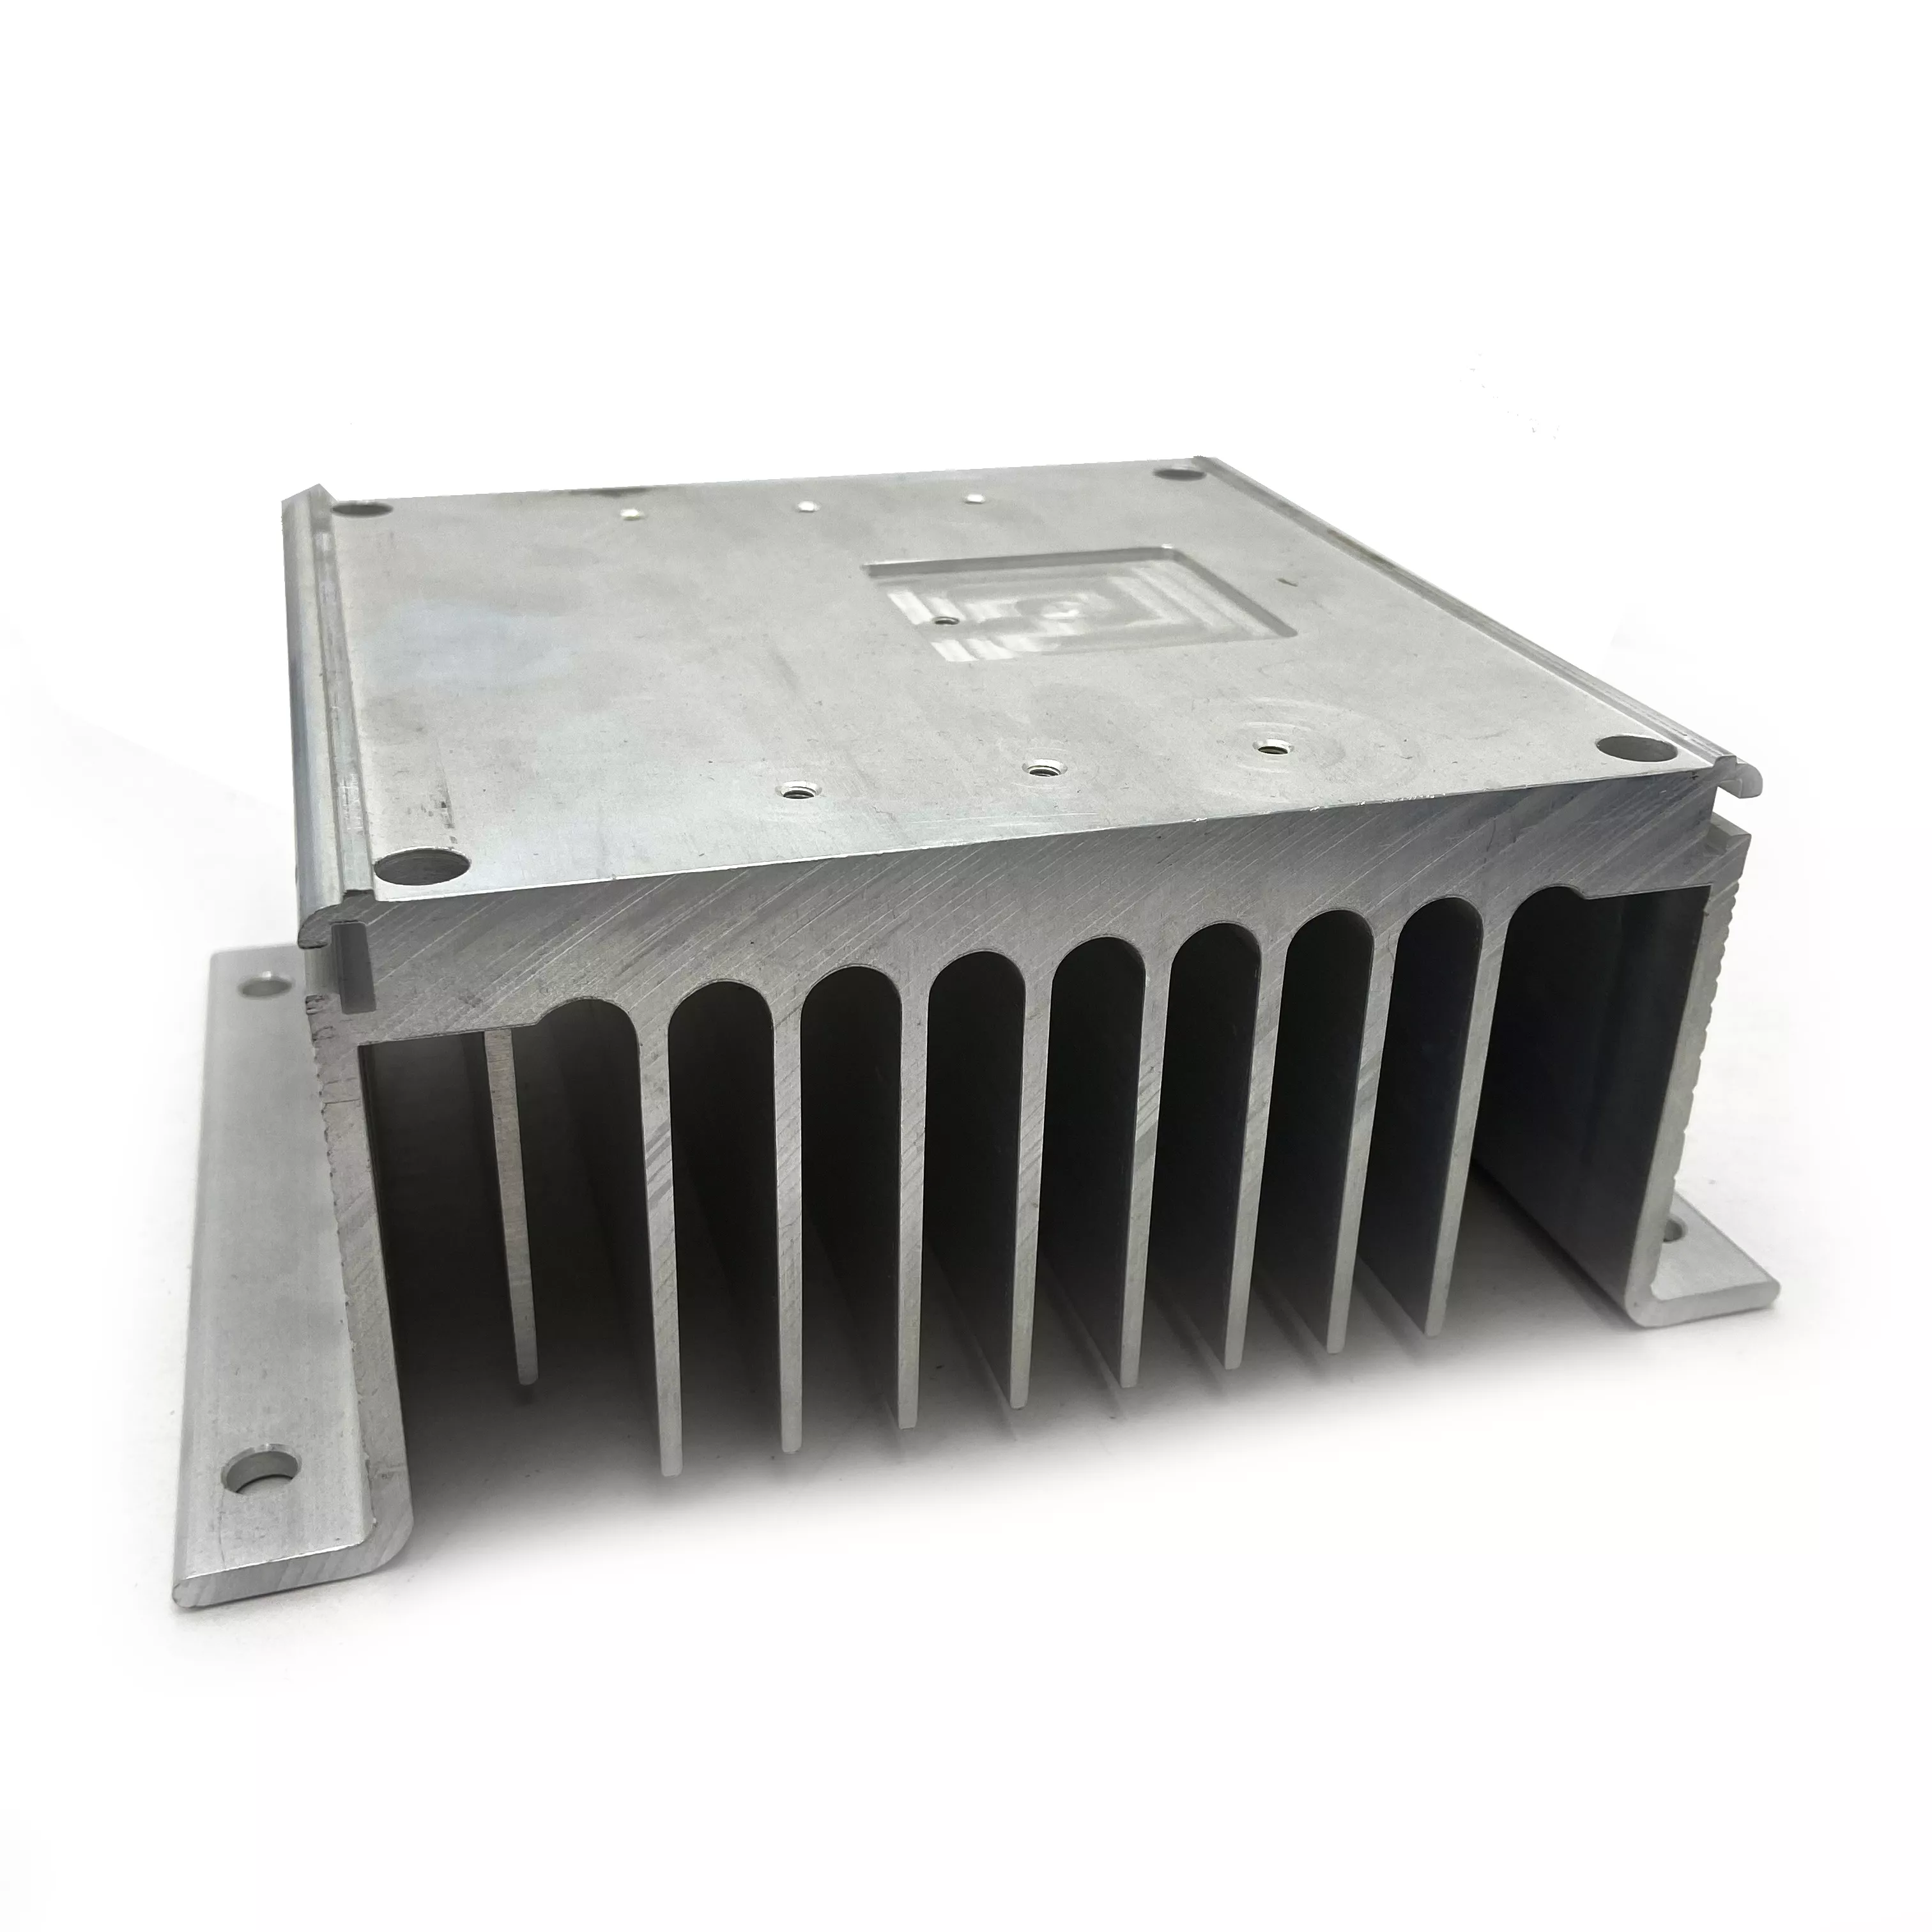
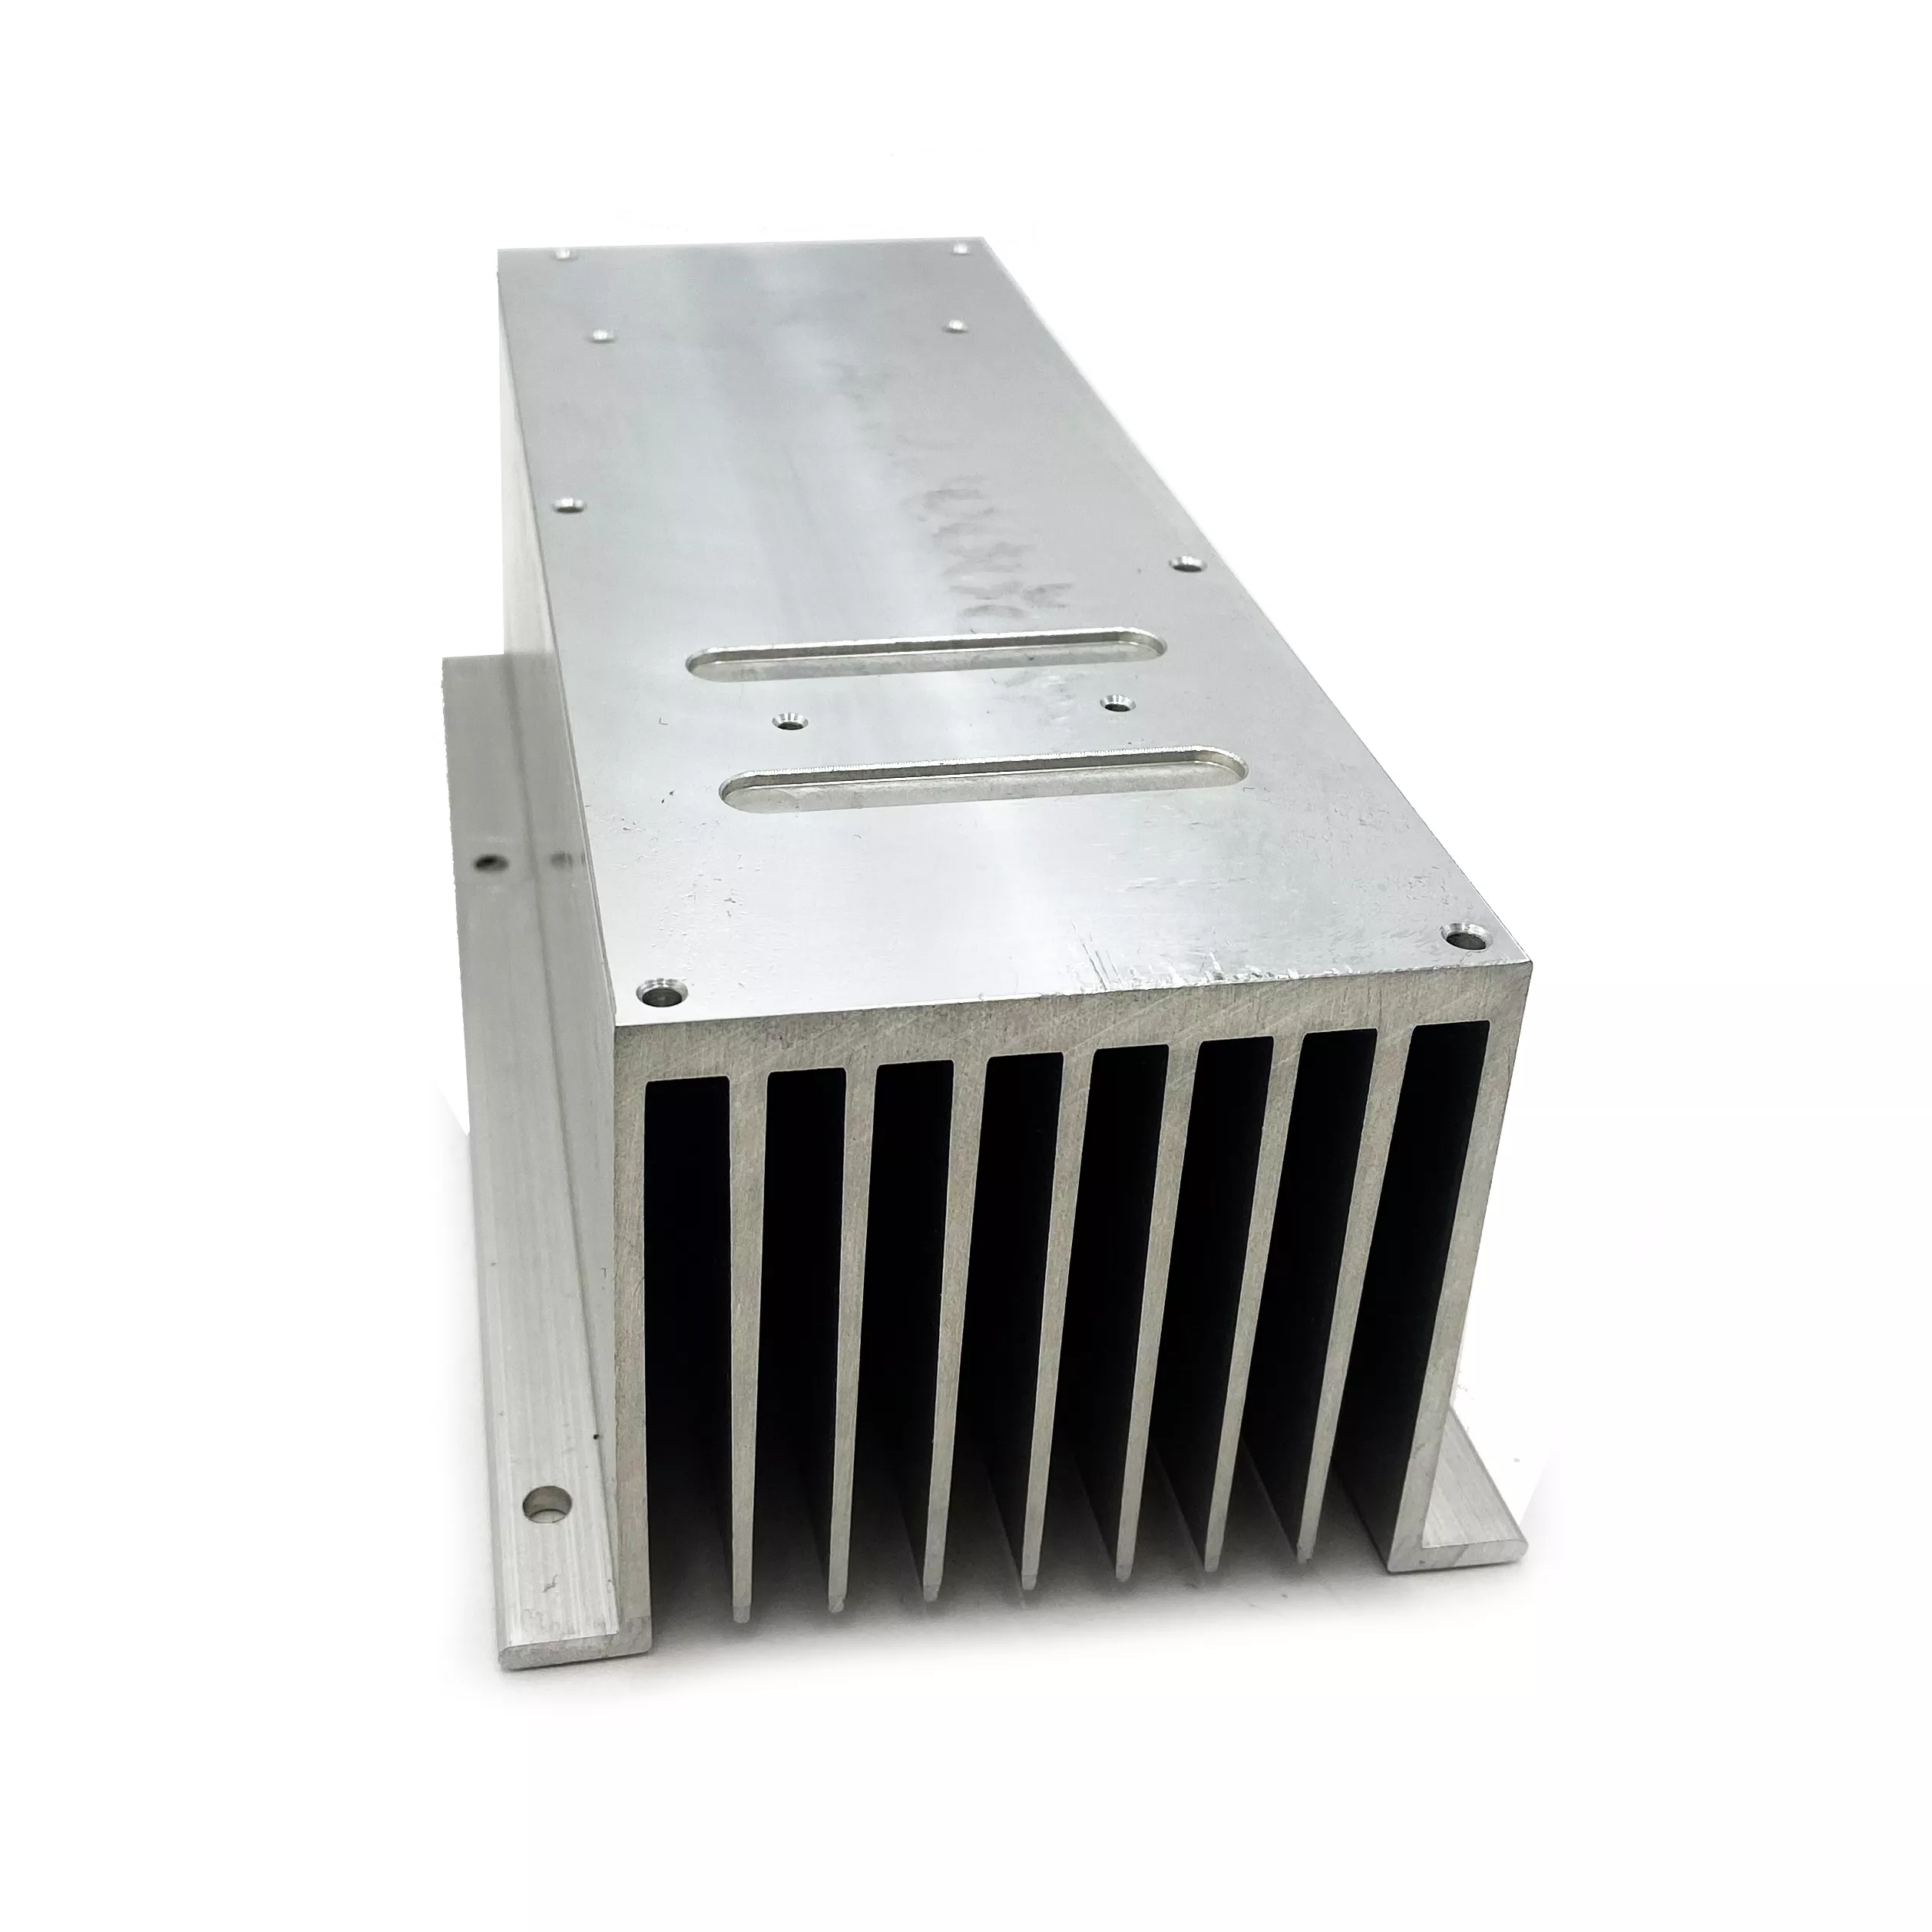
If the design requires holes, pockets or machined contact faces, show them on the controlled drawing. State the dimensions and positional relationships that govern fit. A general CNC-machining description does not define a particular setup or imply that every surface receives the same machining operation.
- Specify 6061 or 6063 and the actual required temper.
- Provide the section drawing and individual component lengths.
- Locate channel, lip and mounting interfaces.
- Mark CNC features, finish and masking requirements.
- Define dimensional limits and inspection records.
Choose between the named alloys
The two alloy names are alternatives, not a single established sample composition. Select the material and condition required by the design and identify supporting records where needed. Apply feature-specific tolerances rather than treating a ±1% reference as an order-wide requirement. Agree the profile-manufacturing and machining route for the actual part instead of automatically following a historical general casting field.
Define the supplied component and thermal context
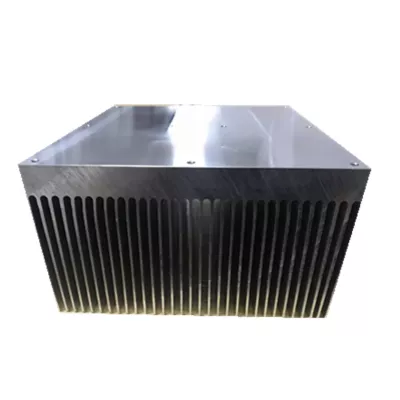
Identify the contact face, heat load, ambient conditions and airflow arrangement needed for thermal assessment. The deep channel and fin geometry do not establish a measured cooling rating. Choose treatment and finish for the selected alloy, with acceptance in the delivered condition. Confirm quantities and whether the order covers only the profile or additional installation components. The enquiry should link one selected alloy and channel drawing to a clear machining, finish and inspection scope.