-
Grade6000 SeriesTemperT3-T8
-
ApplicationHeat SinkShapeAngle
-
Alloy Or NotIs AlloyModel NumberS2301
-
Tolerance0.02mm, ±0.02Processing ServiceBending, Decoiling, Welding, Punching, Cutting, Machining
-
Delivery Time15 daysMaterial6063/ 6061 etc
-
MachiningAvailableSurface treatmentAnodized/oxide etc /powder coated
-
ToolingMade by ourselfSurface ColorCustomized Panton Colors
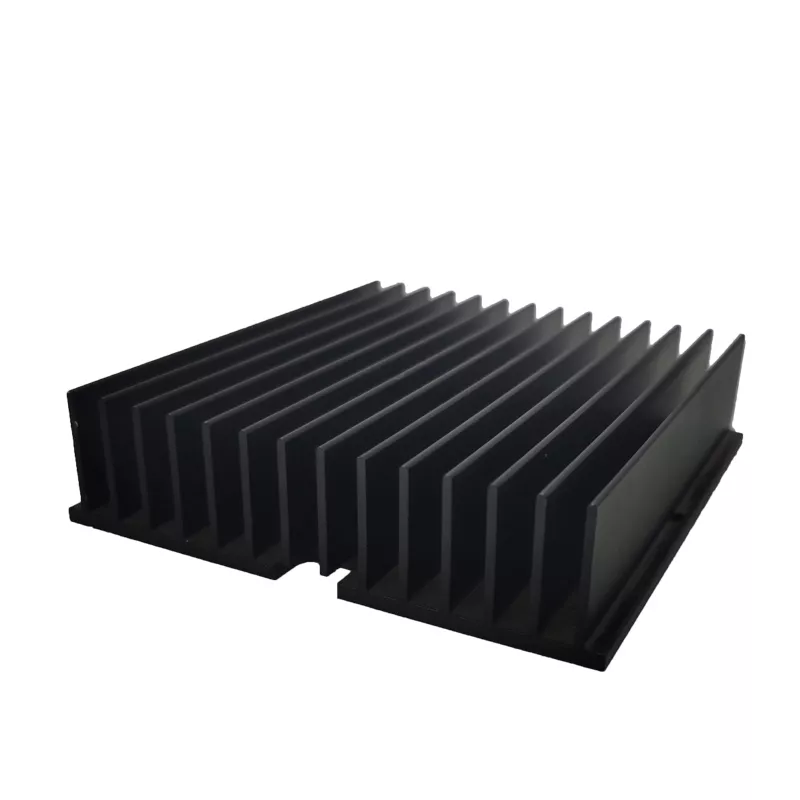
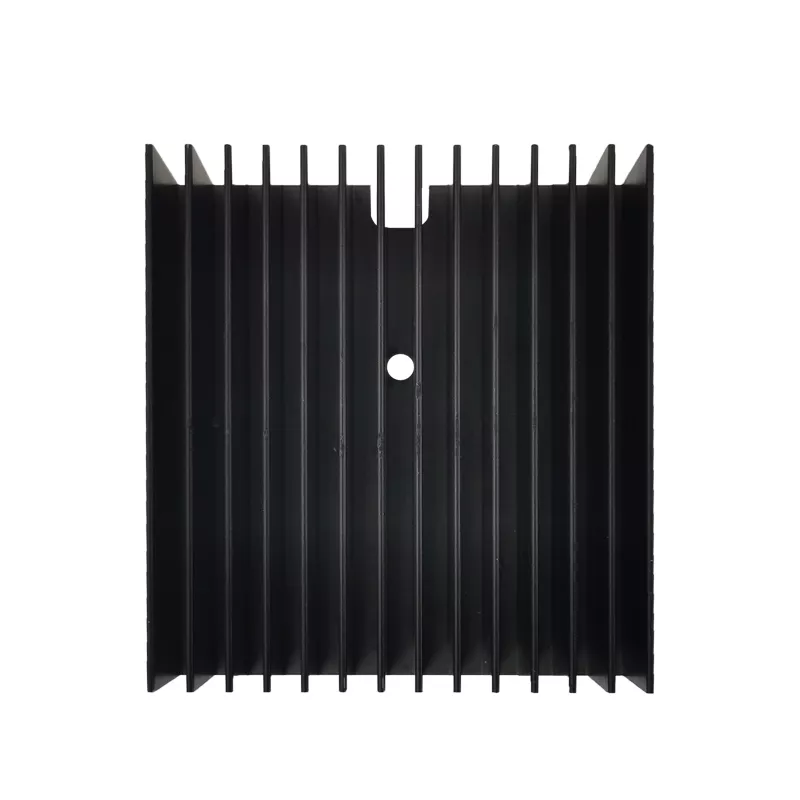
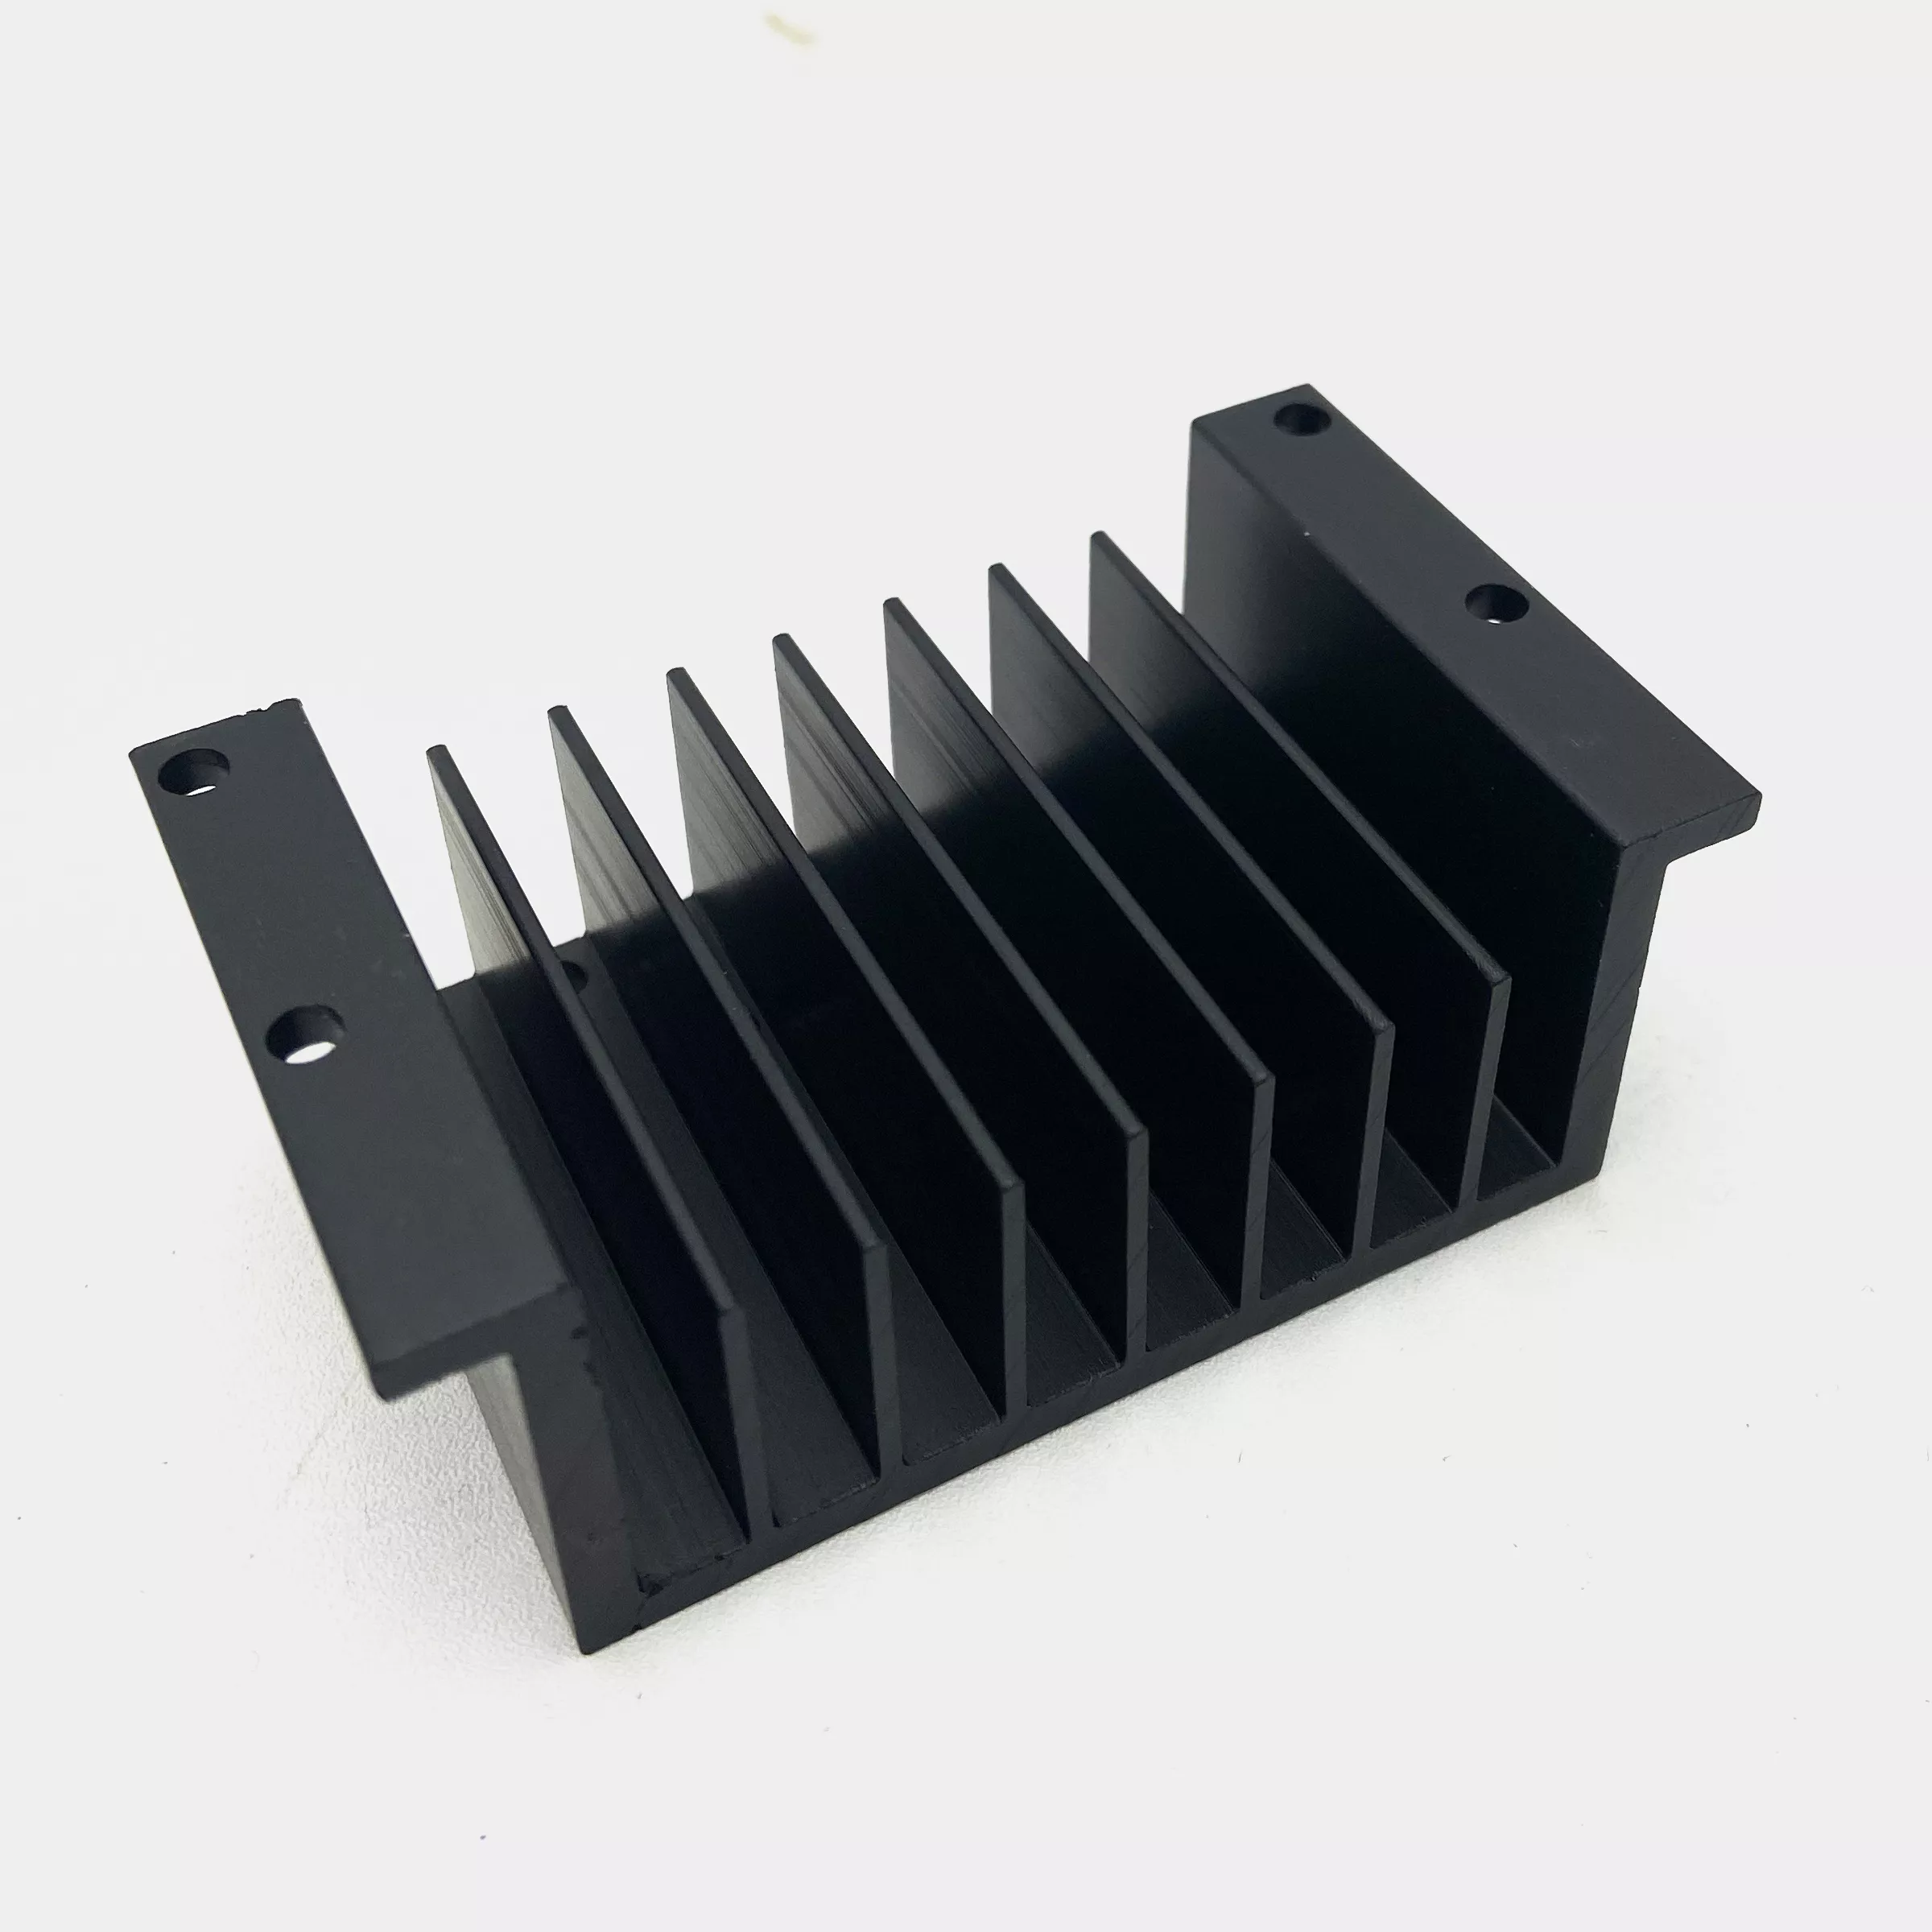
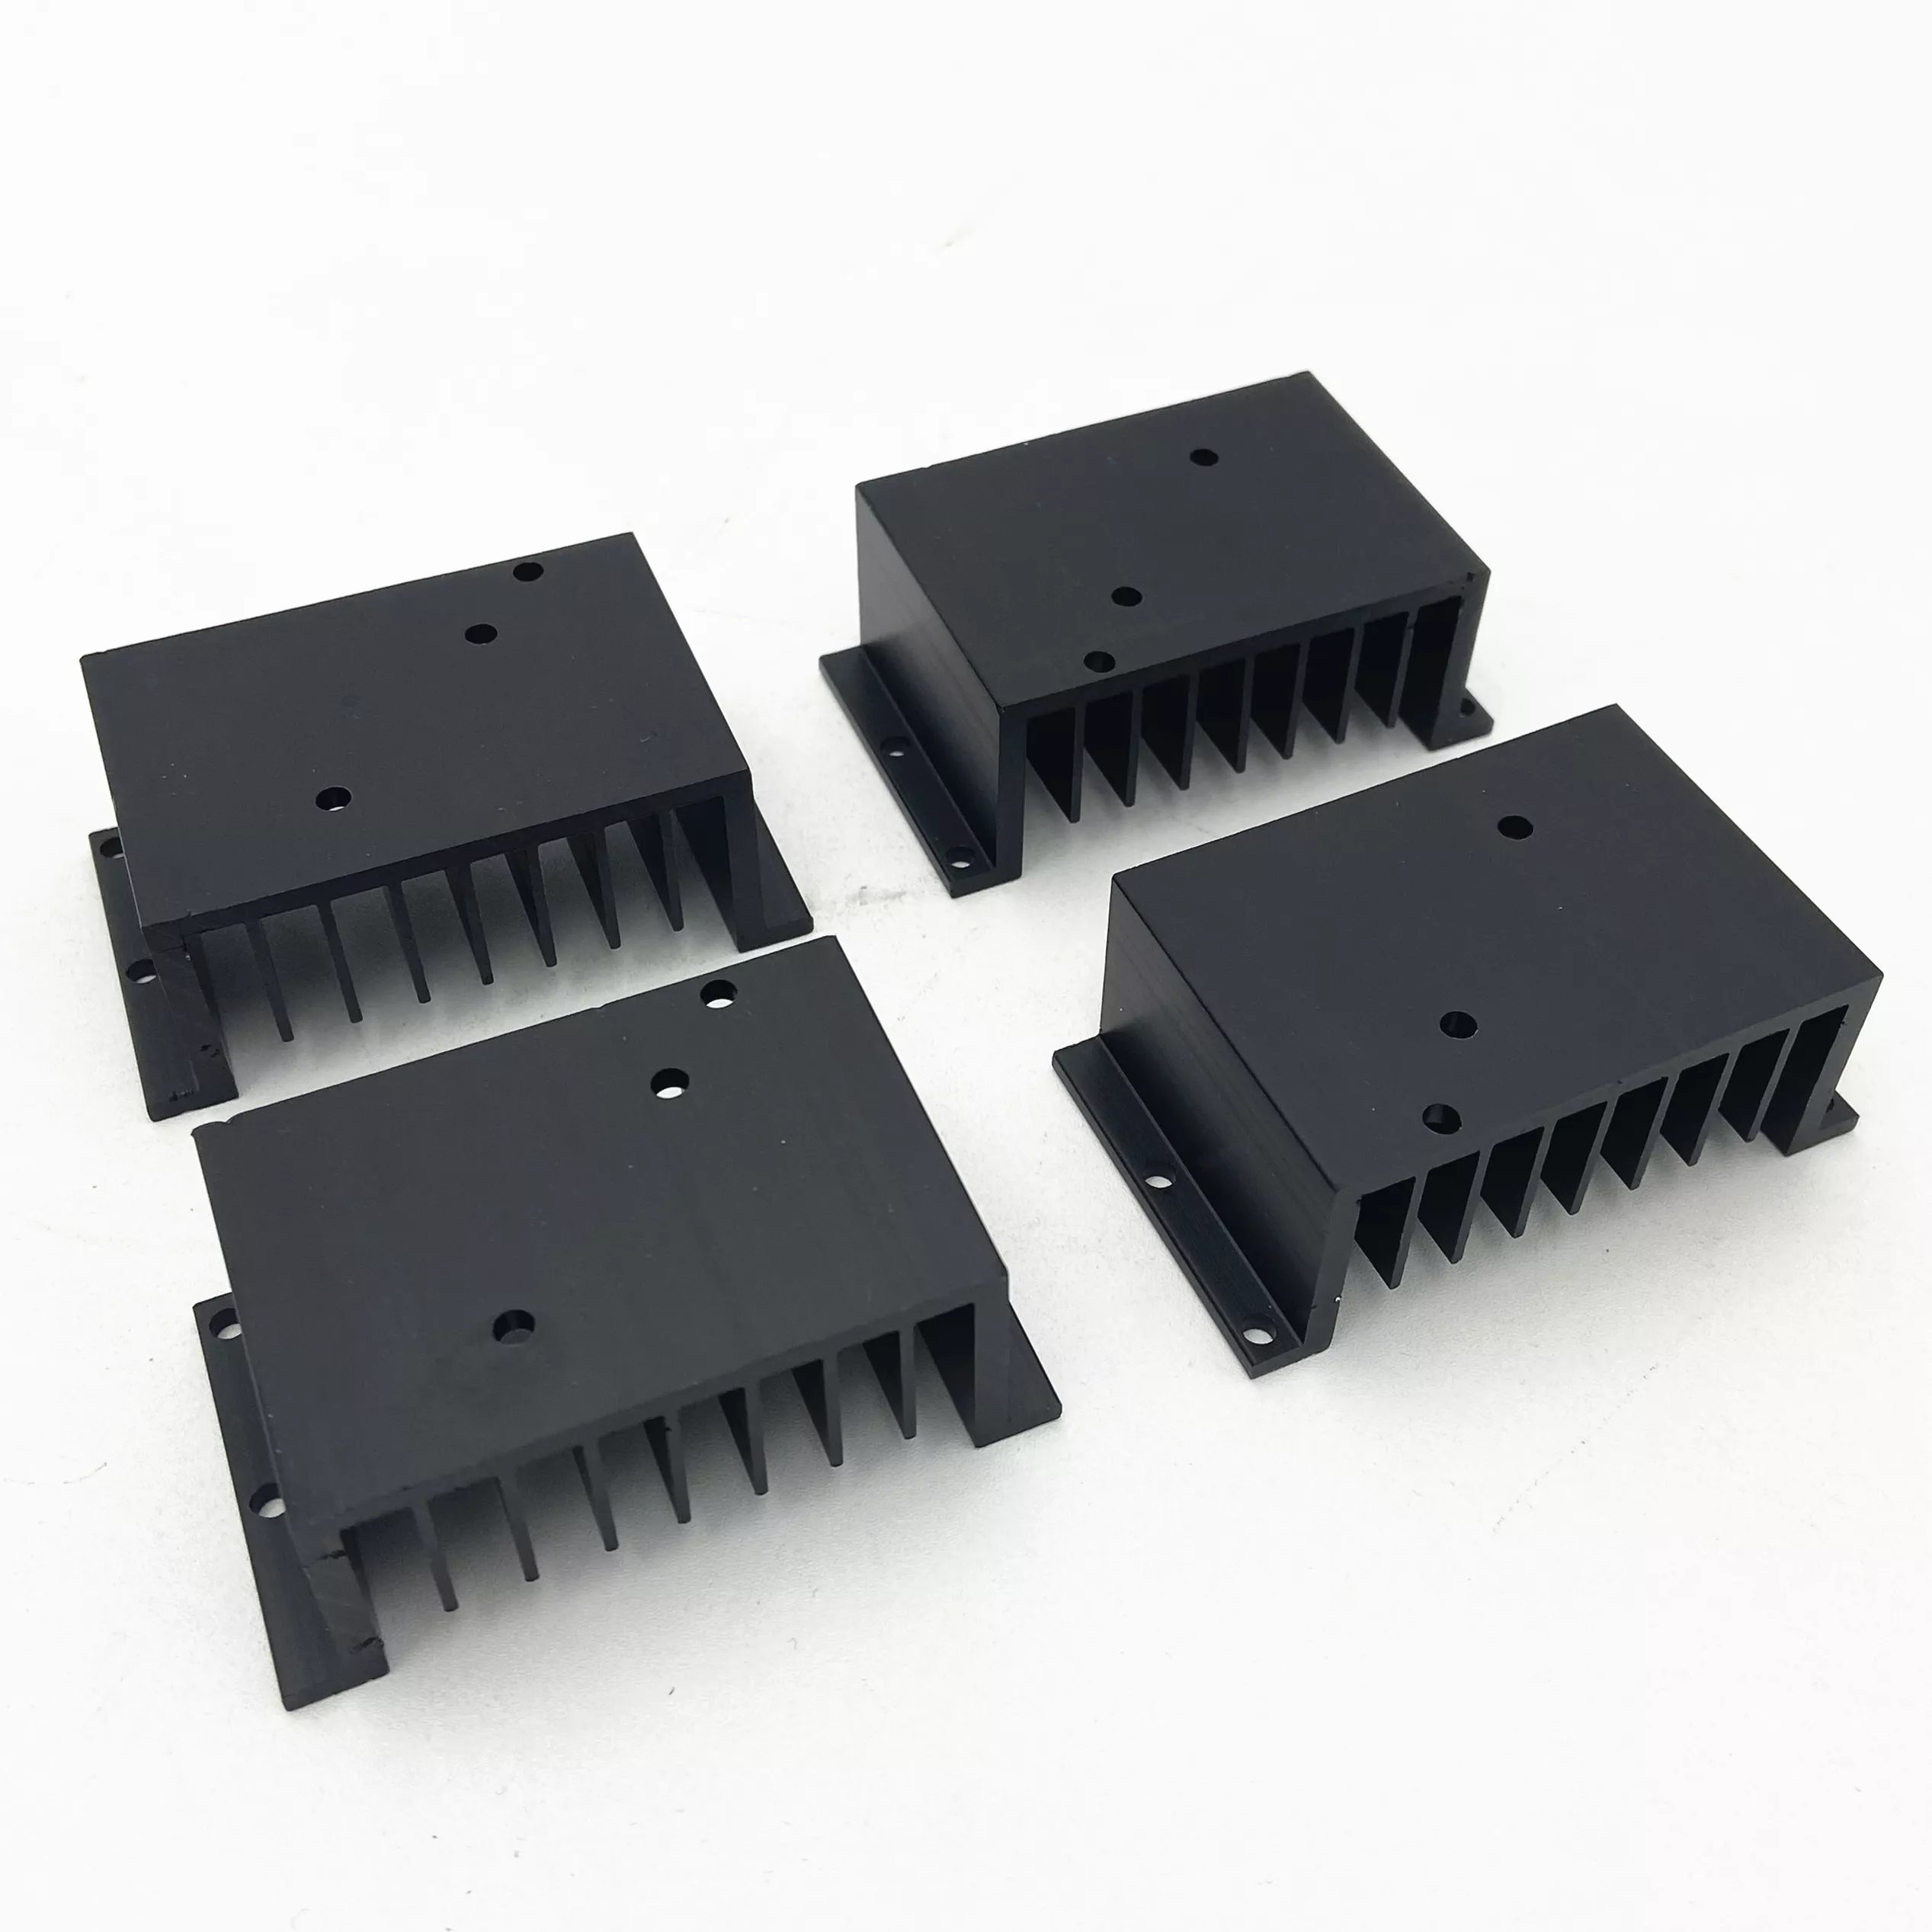
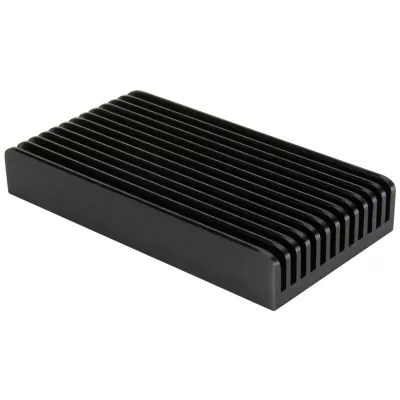
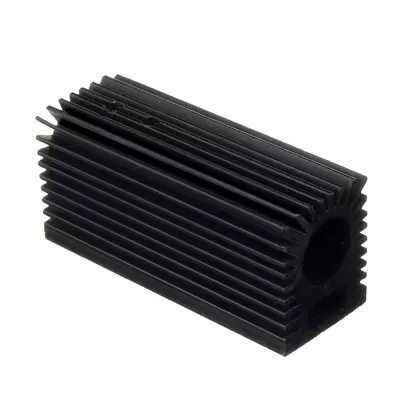
Define the extruded aluminum heat sink and the finished interfaces required by the assembly. The example is a dark rectangular profile with tall parallel plate fins and an interruption along one base edge. These details provide a drawing reference, while the actual section, material condition and anodized finish should follow the order specification.
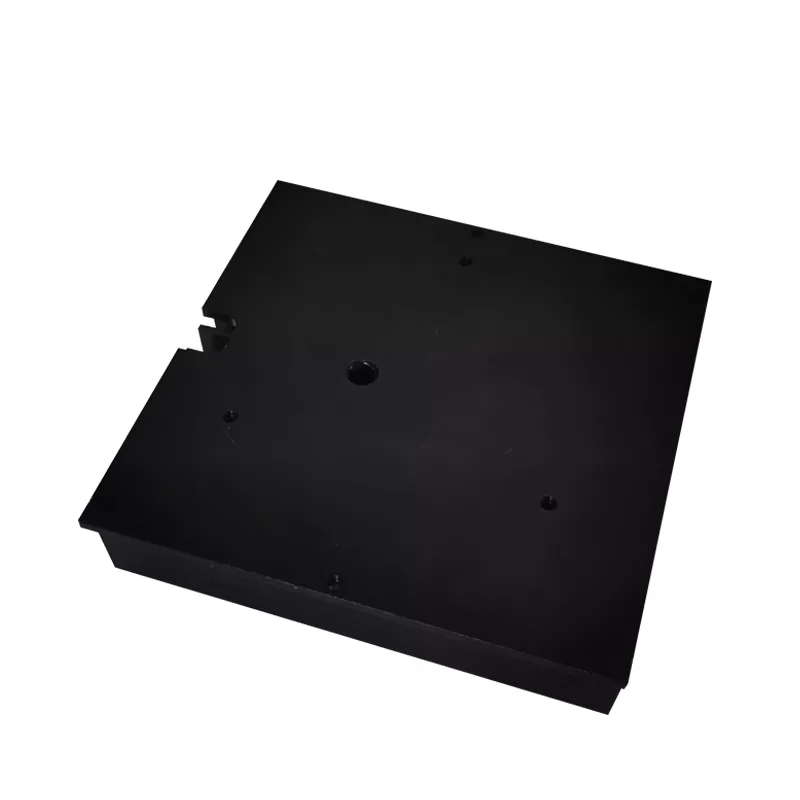
Locate the base edge and contact face
Provide the base dimensions, fin field, cut length and the clearance or engagement required at the interrupted edge. Show the face that contacts the heat source and locate mounting features from the assembly datums. Include adjoining components where they limit access or the available installation envelope.
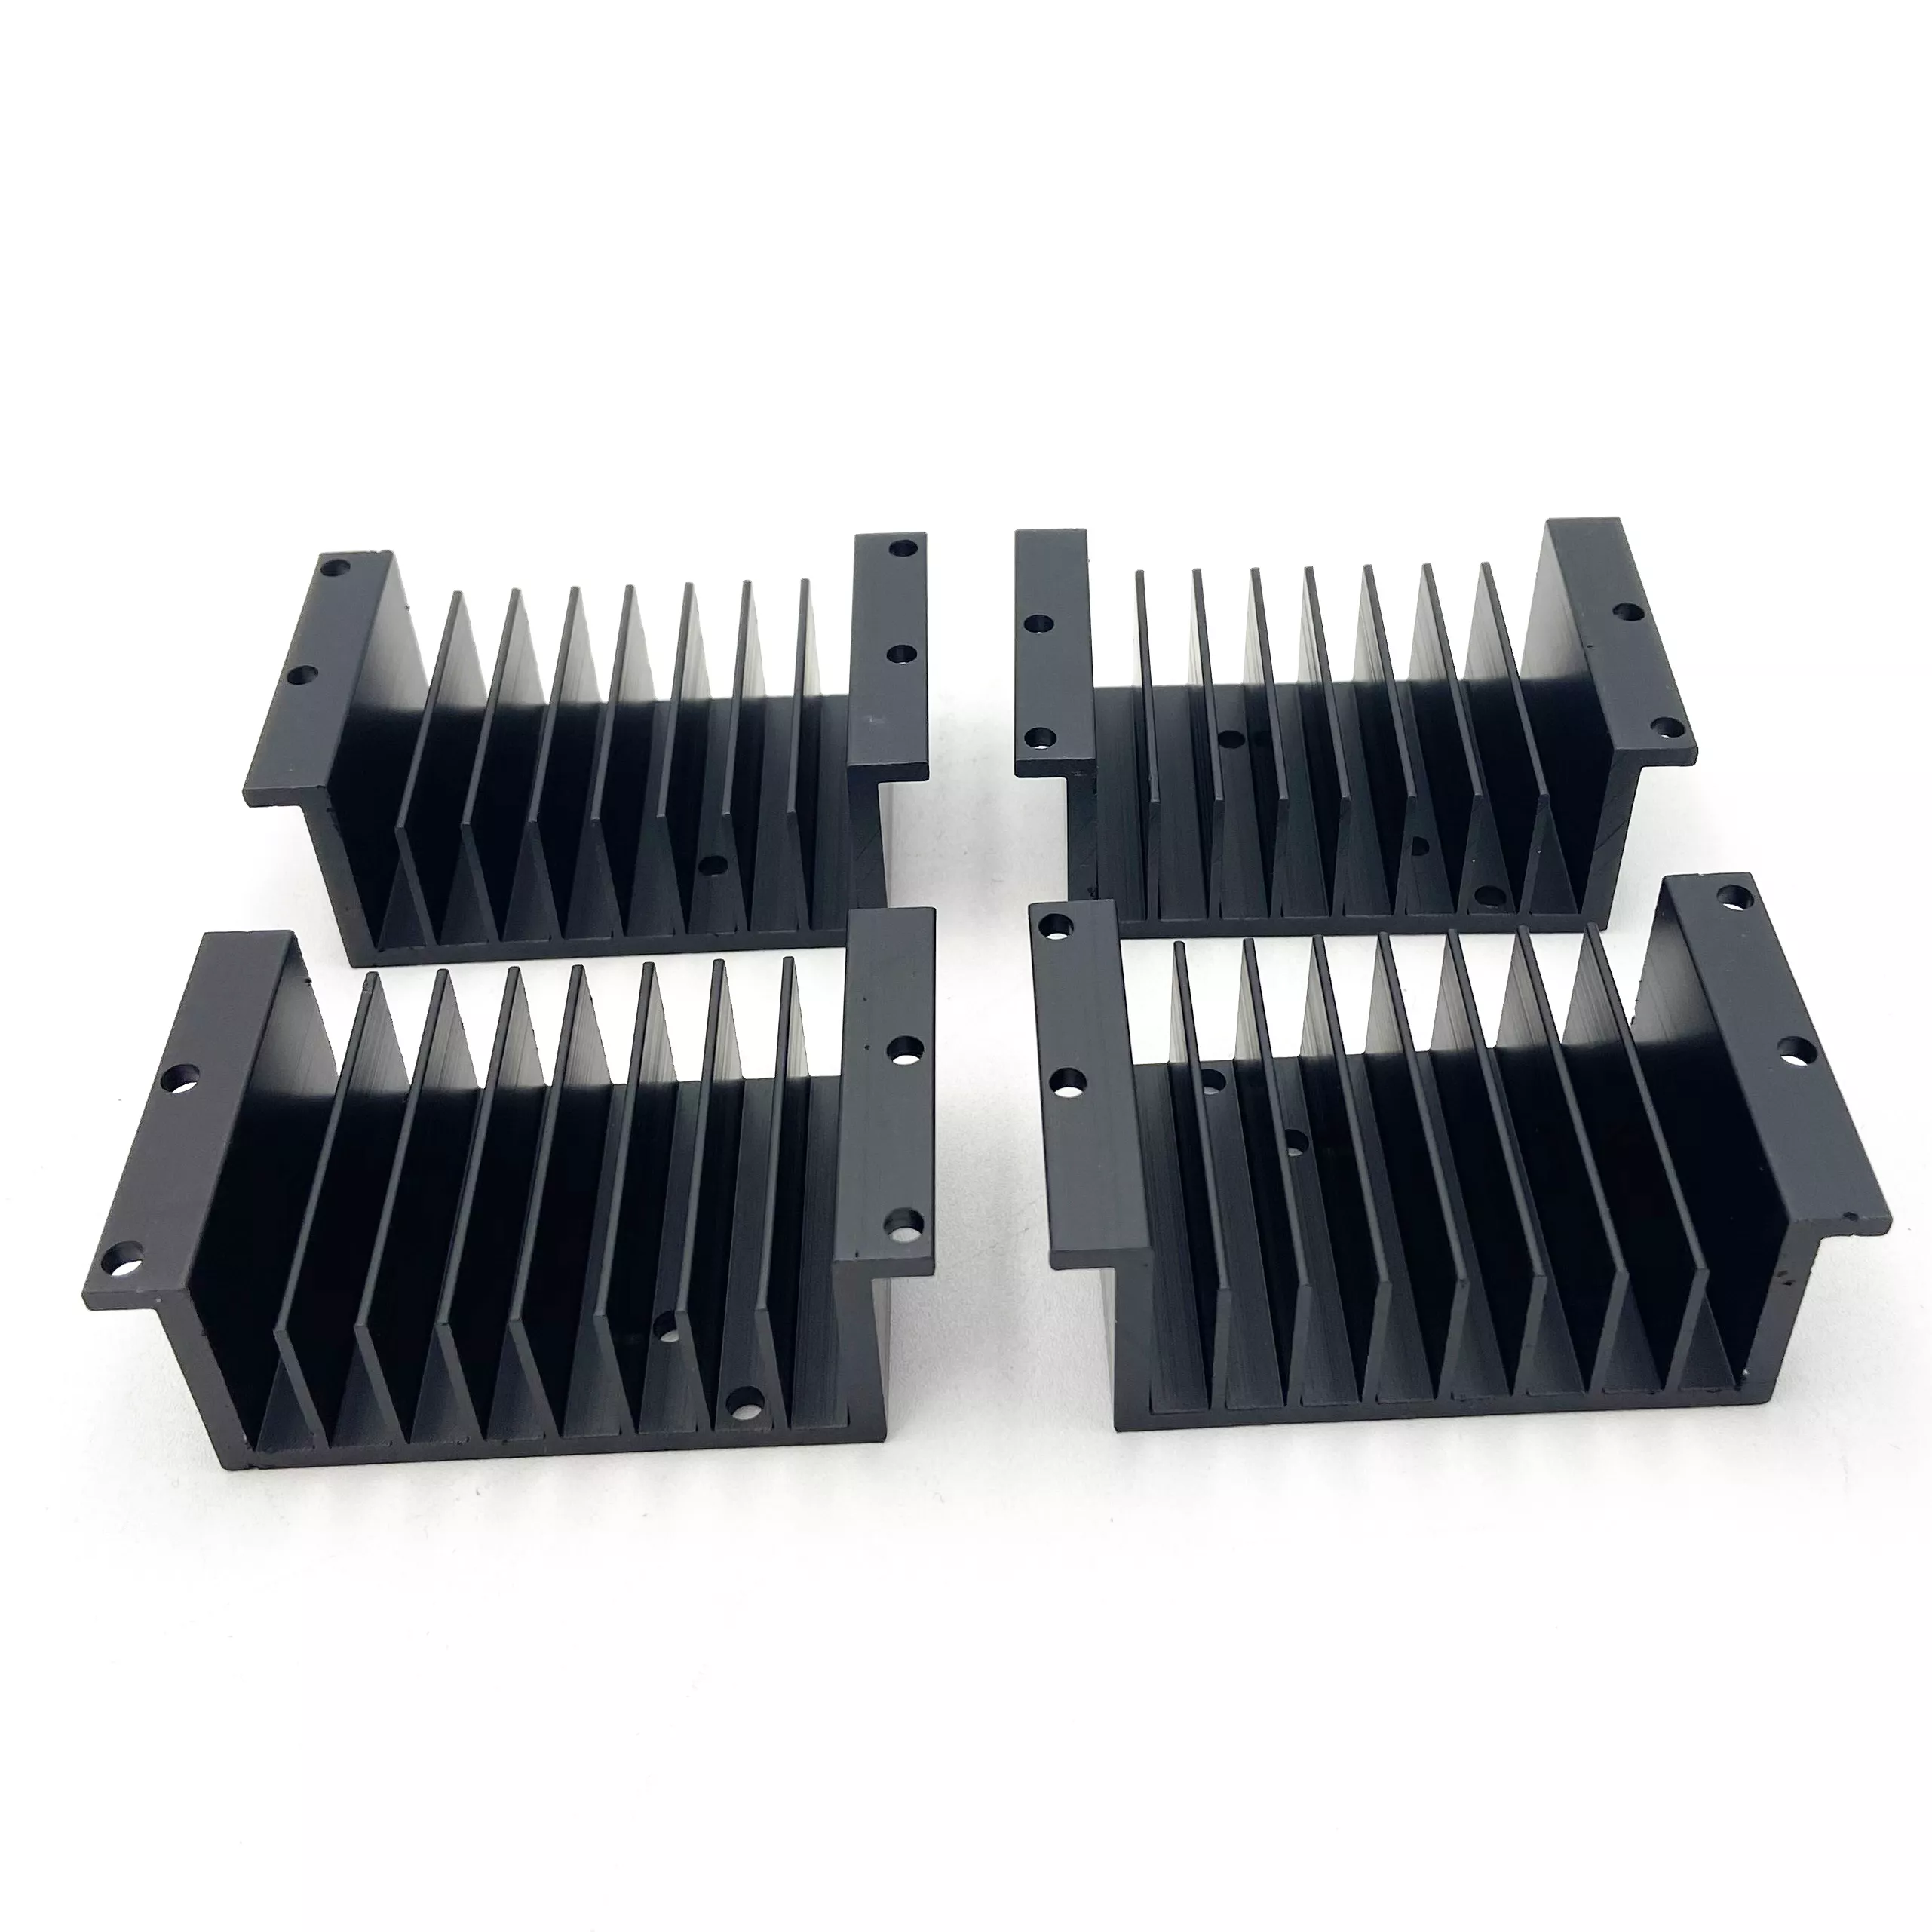
If CNC machining is required, mark the holes, ends or contact surfaces to be finished. State their dimensional limits and positional relationships. The image does not establish a machining setup or one universal geometry for all enquiries.
Agree material, finish and inspection condition
- Select the actual 6061 or 6063 alloy and temper.
- Provide the controlled profile and mounting drawing.
- Locate the base-edge detail and CNC interfaces.
- Specify anodizing, masking and fit-sensitive surfaces.
- Define dimensional acceptance in the supplied condition.
The 0.02mm and ±0.02 references need affected features, units and measurement methods before they can determine acceptance. They do not establish the same tolerance for all fins, cut lengths and machined surfaces. Select the secondary operations needed for the actual design rather than applying every listed service to the part.
Specify the thermal installation requirements
Supply heat load, ambient conditions, airflow and the contact arrangement relevant to thermal assessment. A dark surface and a finned outline do not establish an anodizing specification or a measured cooling result. Identify any project-specific evidence needed under the actual installation conditions. Confirm quantities, documentation and the complete delivered scope for the selected drawing. A useful enquiry links the finned profile and CNC work to a clear material, finishing and inspection plan, so that the proposed component can be accepted against the same requirements used for the quotation.